Aerospace 3D Printing for Aircraft Parts, MRO Tooling and Drone Airframes

MRO tooling, cabin and aircraft-system parts, production drone airframes and propulsion hardware in FST-rated polymers, engineering nylons and metals, with documented inspection and material traceability.

  • FST-rated ULTEM 9085 and Antero 800NA for aircraft interior parts.
  • CoCs, inspection records and lot traceability on request.
  • Production drone parts in repeat runs without tooling investment.
Aerospace 3D Printing Solutions
Aerospace Overview

3D printing for aerospace production, tooling and development

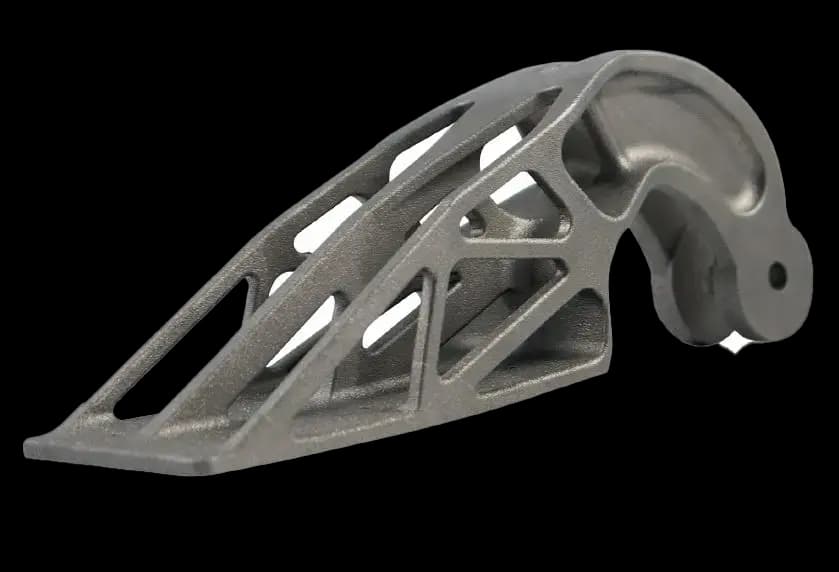
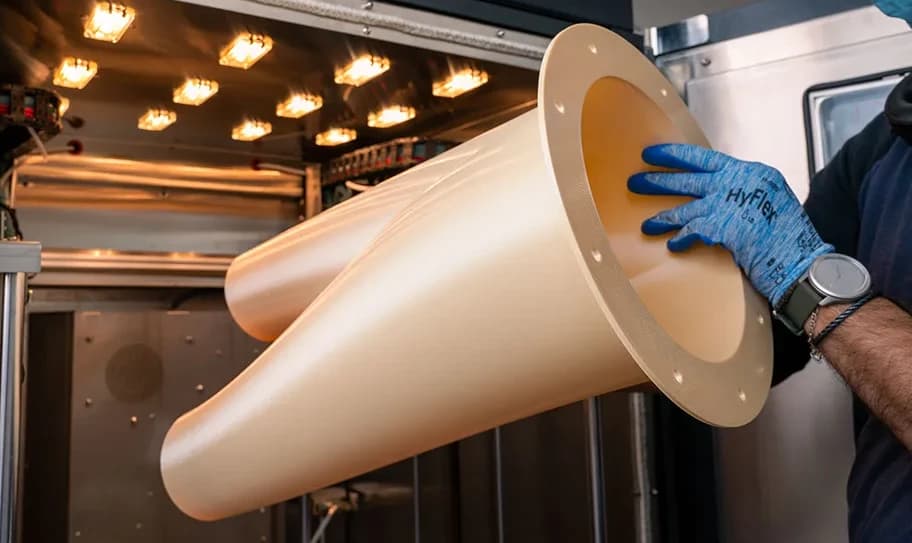
Aerospace teams use additive manufacturing where machining and moulding are slow or uneconomic at low volume. We make engine test plates and fixtures for MRO shops, ULTEM enclosures for aircraft water systems, cabin trays and trim, production airframe parts for drone and UAS manufacturers, combustor swirlers, pump impellers and pitot rakes for propulsion developers, stator sections for electric aircraft, titanium parts for space programs, and sensor and optical test housings. We build them with FDM, MJF, SLS, DMLS, SLA and PolyJet, around material traceability and repeatable inspection, so engineers can move from design review to production hardware without machining lead times.

Where additive creates leverage

Lighter parts, fewer assemblies and spares on demand

Forge Labs helps teams move from design validation to production-ready parts without waiting on tooling lead times. Consolidated assemblies, lighter parts, and faster revisions give engineering teams more control over schedule, cost, and performance.

Key manufacturing benefits

  • Make complex ducting, brackets and housings without the cost premium machining puts on complex geometry.
  • Produce MRO tooling and spare parts on demand, with no tooling or stored inventory.
  • Consolidate several fixtures or assemblies into one printed part with fewer failure points.
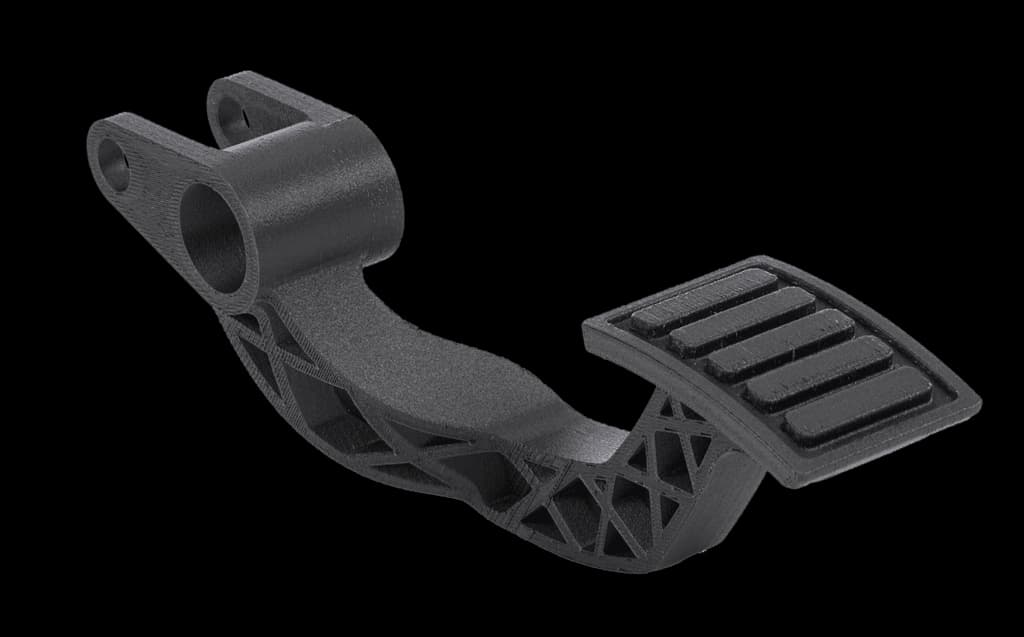
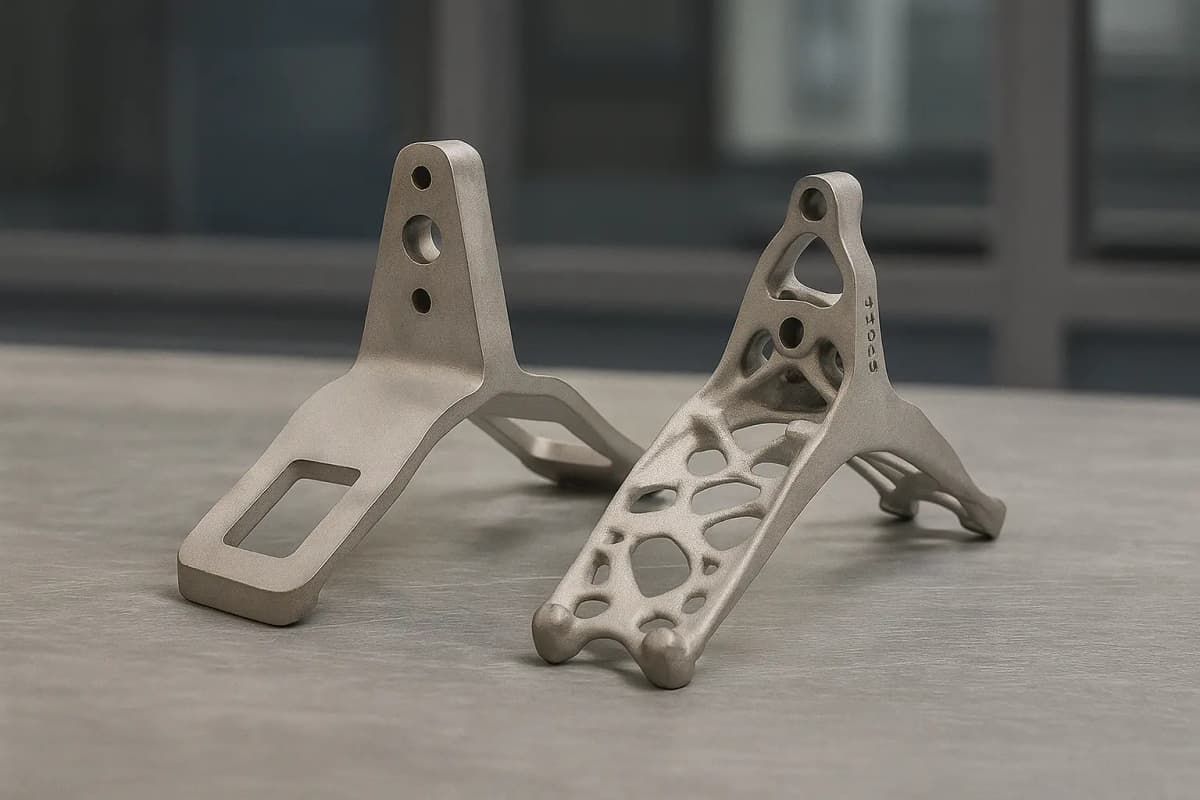
  • Cut part weight through optimized geometry and lightweight materials, for fuel savings in service.
  • Customize parts quickly in lightweight aerospace materials such as ULTEM 9085 and titanium.
  • Shorten prototyping and design iteration cycles before production.
Aerospace Manufacturing Process 1
Aerospace Manufacturing Process 2
Aerospace Manufacturing Process 3
Aerospace Manufacturing Process 4
Quality and compliance

Traceability and compliance for aerospace qualification

From cabin interior components to production tooling, each build can be supported with material pedigree, inspection records and documented process controls that help aerospace teams qualify printed parts with fewer surprises. Read the Cozy Mk IV investigation and updated LAA guidance.

Compliance documentation
Certificates of conformance, material test reports and batch traceability that support FAA compliance processes for aircraft components and interior parts.
FST-rated materials
Flame, smoke and toxicity rated materials for aircraft interiors, including ULTEM 9085 and Antero 800NA.
Material traceability
Batch tracking and material certification for every component, with a complete documentation chain from material lot to finished part.
ISO 9001-aligned quality assurance
Rigorous inspection protocols and quality controls under ISO 9001-aligned processes, held to the tolerances on your drawings.
First article and production sampling
Attach drawings with tolerance callouts and add first article inspection or production sampling where offered for the material.
Digital inventory and repeat lots
Part files stay archived, so tooling, spares and production lots can be reordered from your order history without holding physical stock.
Manufacturing Capabilities

3D Printed Aircraft, Drone and Propulsion Parts

The aerospace parts we make most often, with the processes, materials and material data behind each.

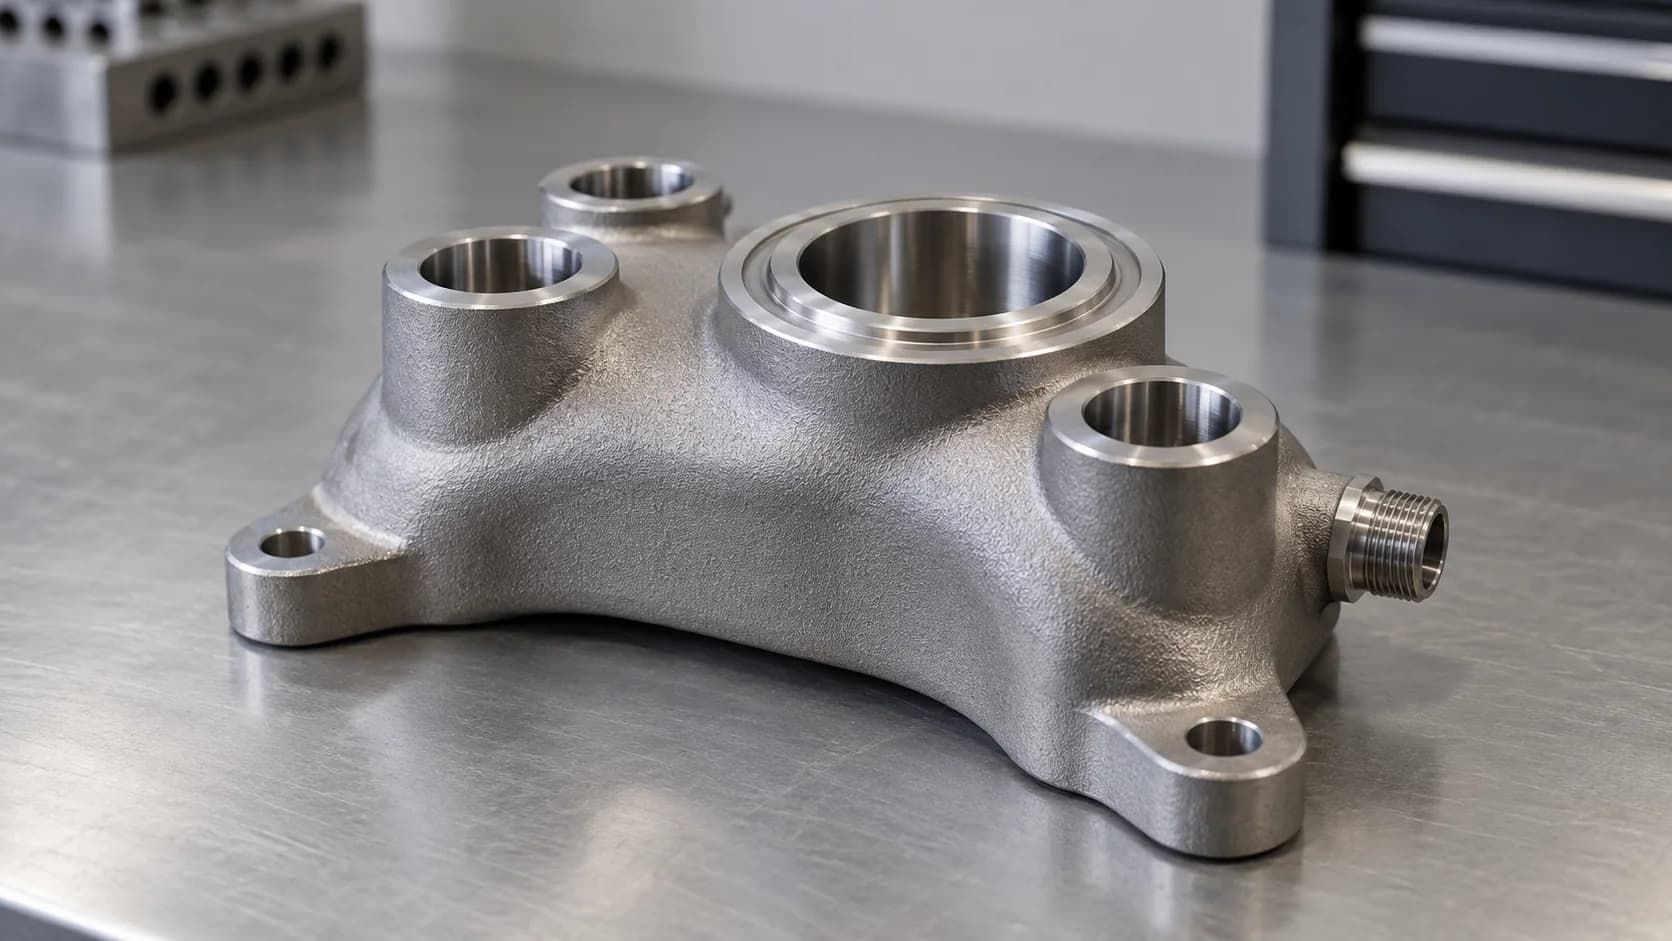
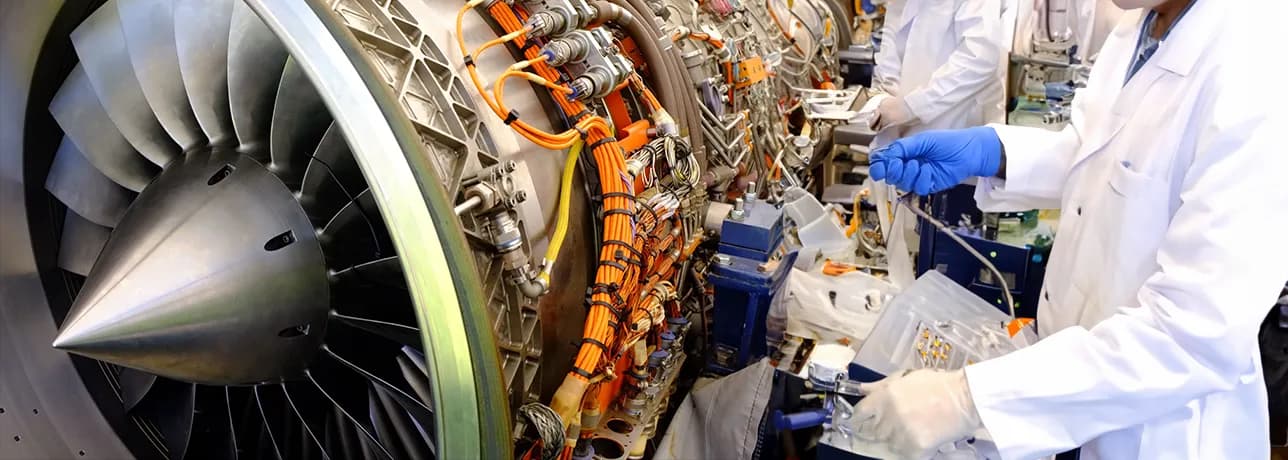
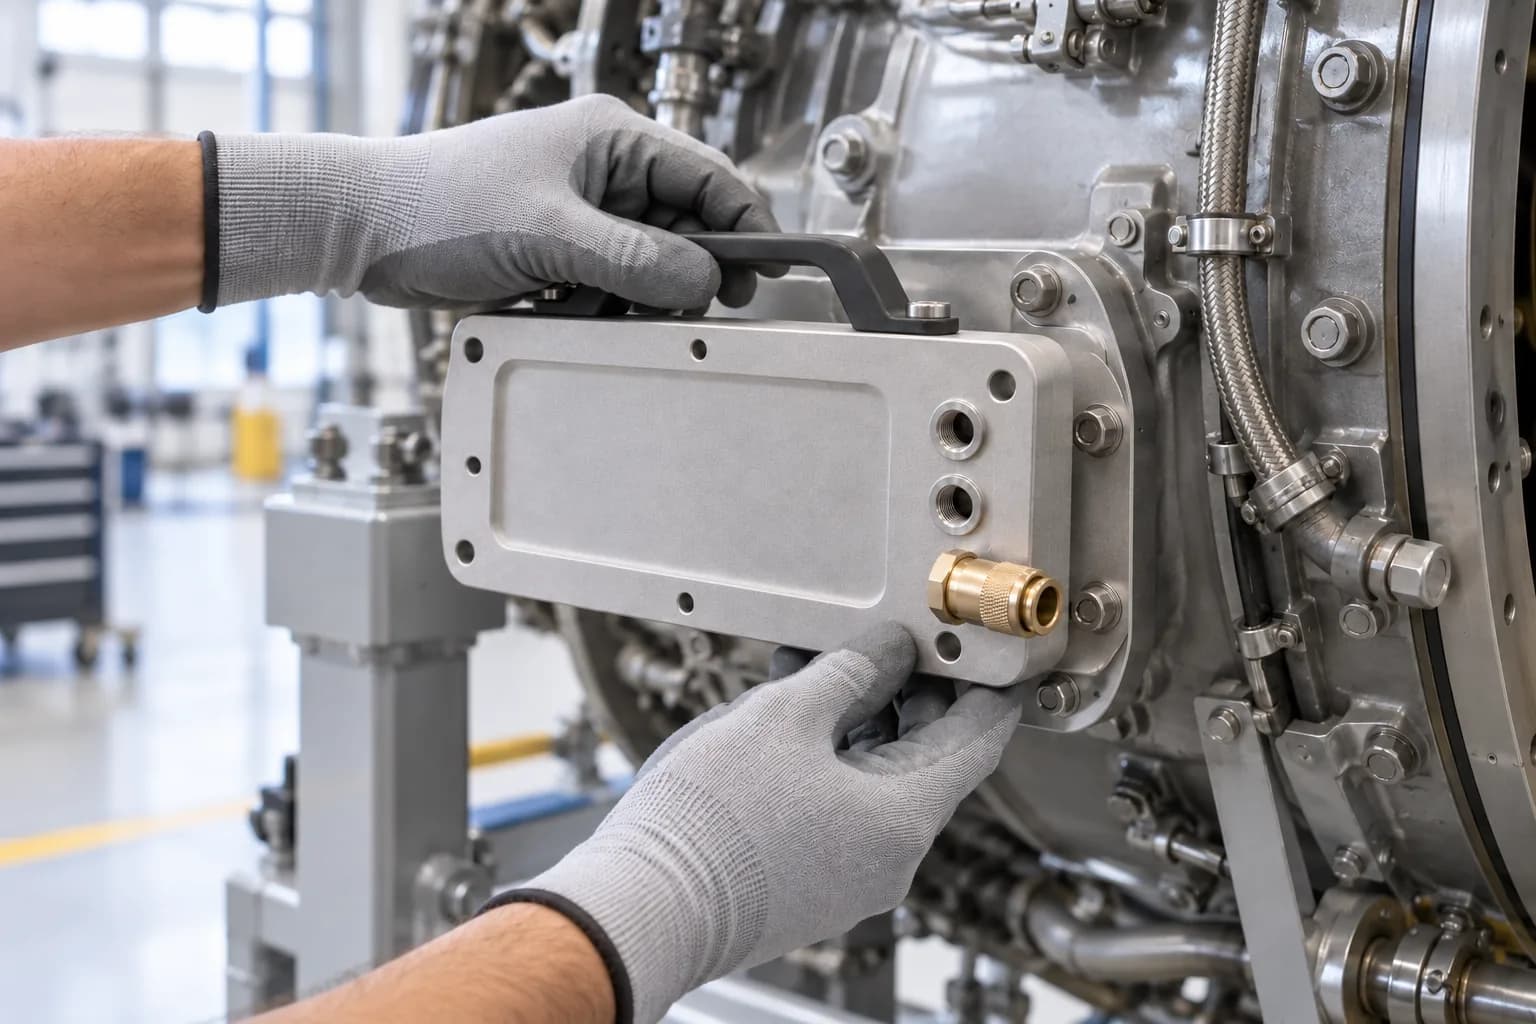
3D printed stainless test plate fitted to an engine during maintenance

Engine MRO and line maintenance

MRO Tooling & Test Fixtures

DMLS 316L stainless steel makes engine test plates and maintenance fixtures to the shop's drawings, including a single tool that replaced three separate fixtures. Parts are printed with extra stock on critical bores, then drilled, threaded and grooved for O-rings to the finished sizes, and internal air passages are polished. FDM ULTEM makes larger jigs and fixtures; Stratasys rates ULTEM excellent against petroleum fuels and good against oils and greases.

Typical parts
Engine test plates, maintenance fixtures, jigs, small MRO replacement parts
Key properties
Machining stock on critical bores; threads and O-ring grooves finished to drawing
Material data
316L stainless; ULTEM: excellent vs fuels, good vs oils and greases (Stratasys)
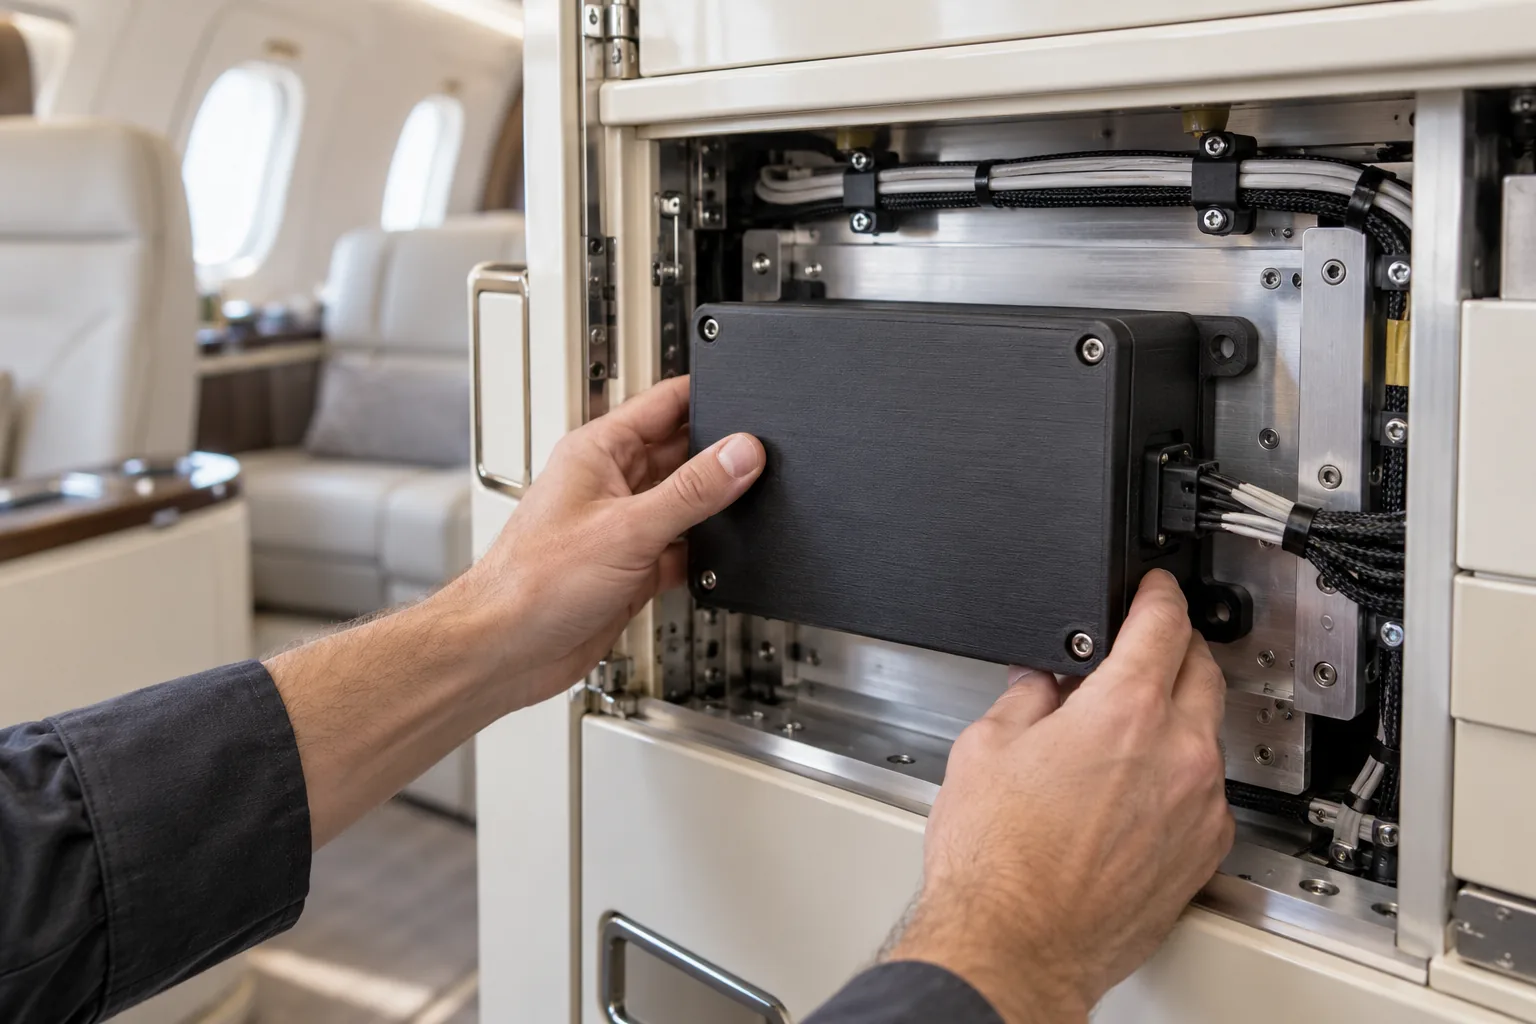
Black ULTEM 9085 enclosure fitted behind an aircraft cabin panel

Cabin, galley and aircraft systems

Cabin Interior & Aircraft Systems Parts

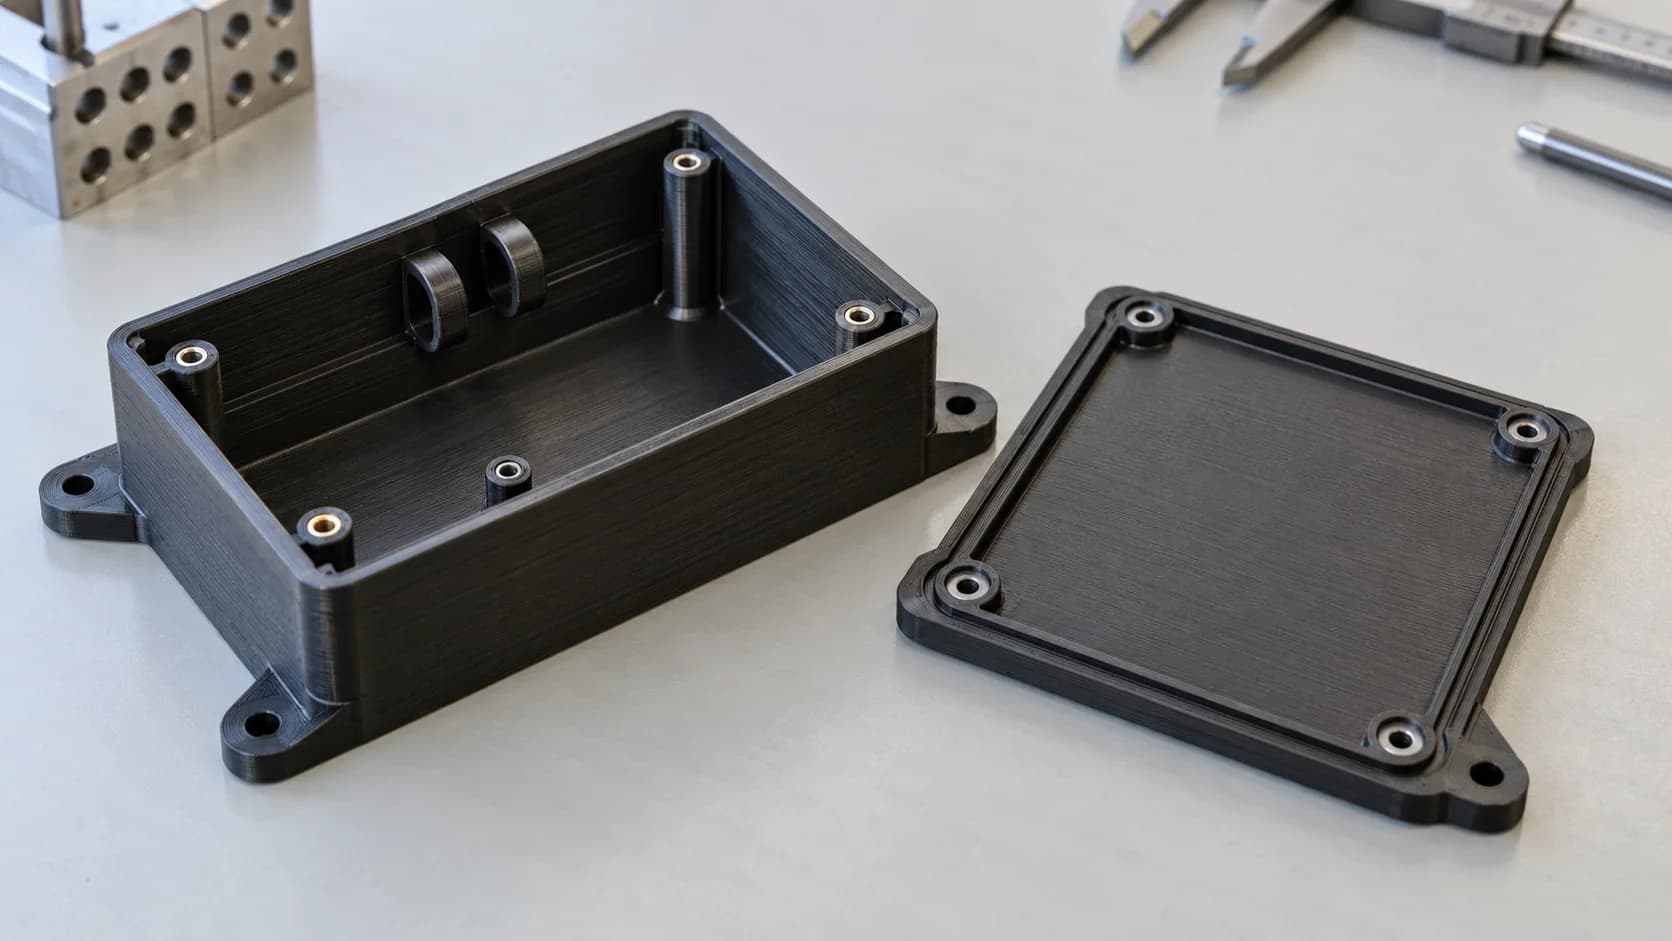
FDM builds black ULTEM 9085 enclosures for aircraft water-system controllers to drawings that specify the material, the FDM process and the build direction, and ULTEM 9085 and Antero 800NA carry FAA flame, smoke and toxicity data for cabin parts. SLA and FDM make large cabin parts in one piece, such as trays over 600 mm long and curved polycarbonate trim, and ULTEM 1010 serves out-of-cabin and high-heat parts.

Typical parts
Controller enclosures, cabin trays, curved trim, ducts, brackets
Key properties
Build direction to drawing; cabin parts over 600 mm in one piece
Material data
ULTEM 9085: FAR 25.853; Antero: BSS 7238/7239, AITM; 170 °C HDT (ULTEM 9085)
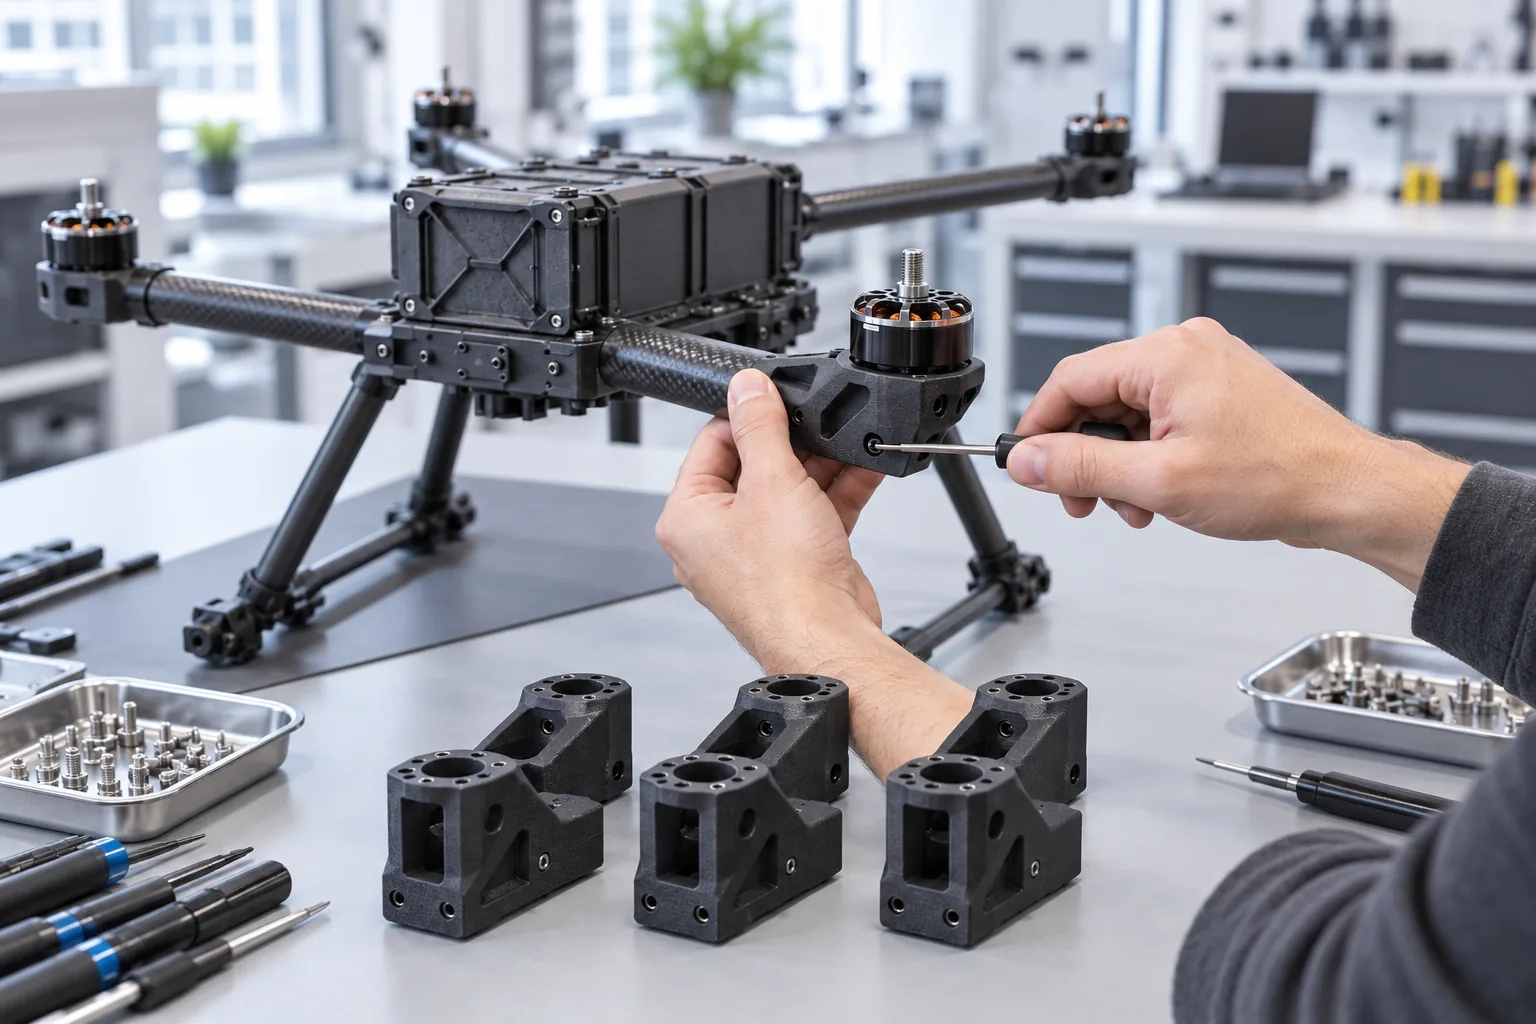
Black SLS nylon motor mounts being fitted to a drone airframe

Production drones and UAS

UAS & Drone Airframe Production

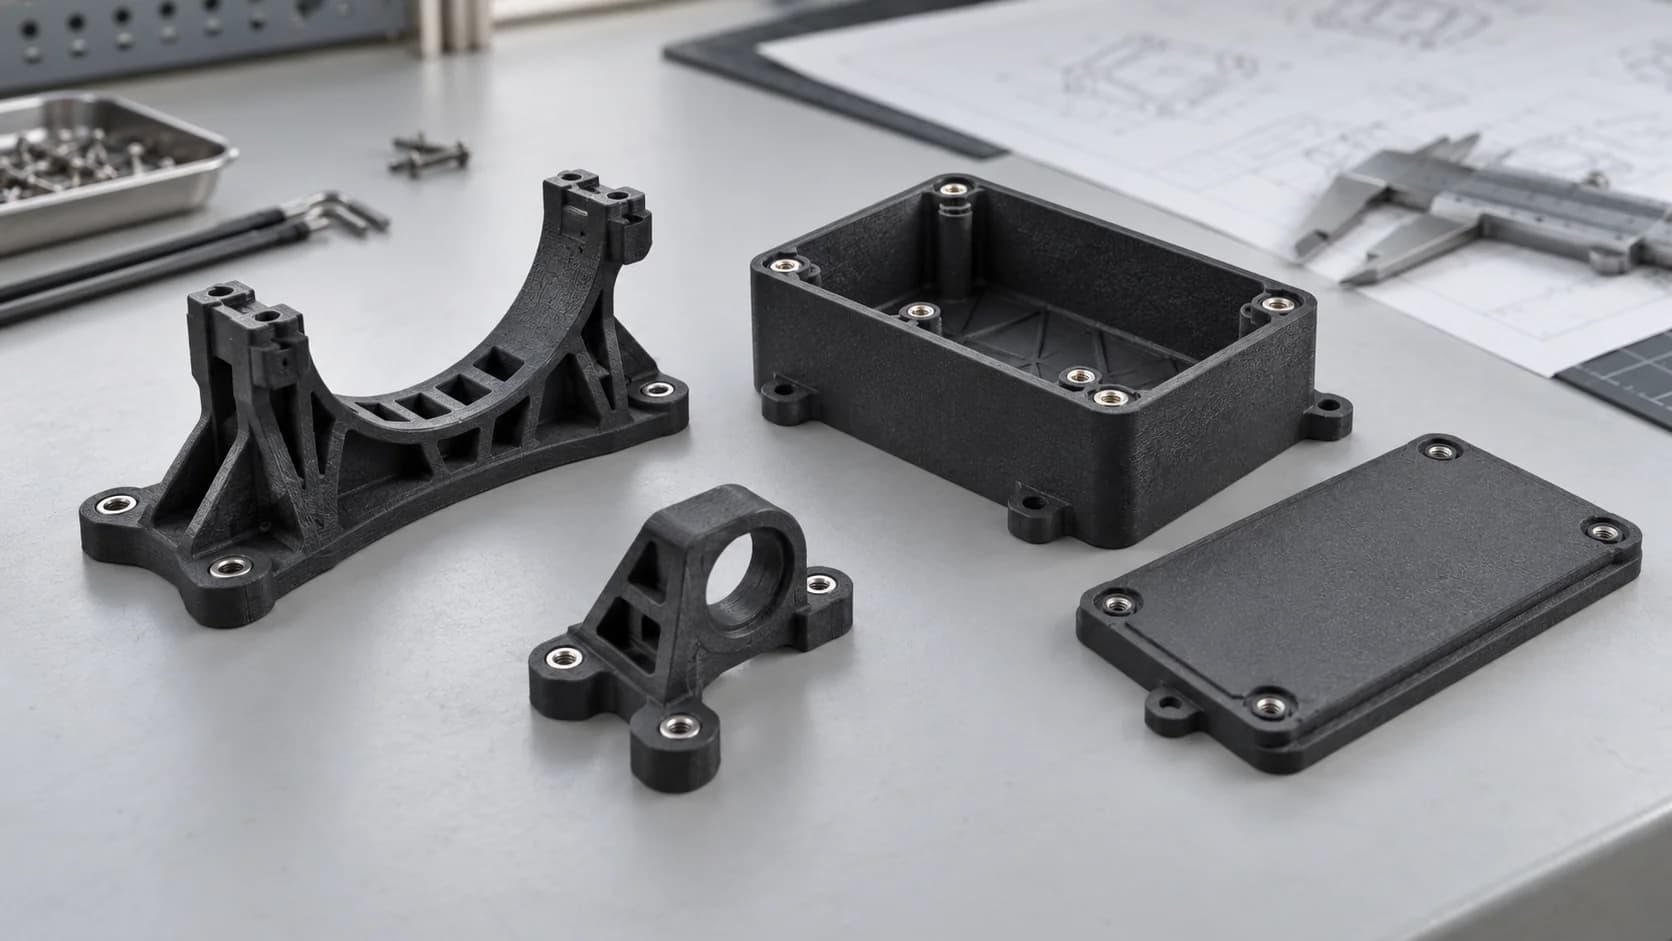
SLS PA12 is the production process for drone and UAS airframe parts: fuselage bodies up to 370 mm long, end caps and access panels, battery enclosures and latches, GPS, camera and optical-flow mounts, antenna clamps and motor guards. One UAS manufacturer has ordered more than 2,000 parts across 15 orders, with motor mounts in runs of 360 and threaded heat-set inserts installed to its drawings. With no supports, internal routing and snap features print in the part. In a separate racing-drone project, a topology-optimized carbon-fibre-reinforced frame weighed 40% less, had higher crash resistance and incorporated cable routing.

Typical parts
Fuselage bodies, mounts, battery enclosures, sensor and antenna mounts
Key properties
Runs of 360 per order; heat-set inserts installed; SLS ±0.3% (min ±0.3 mm)
Material data
Nylon PA12: 48 MPa tensile, 1.01 g/cm³
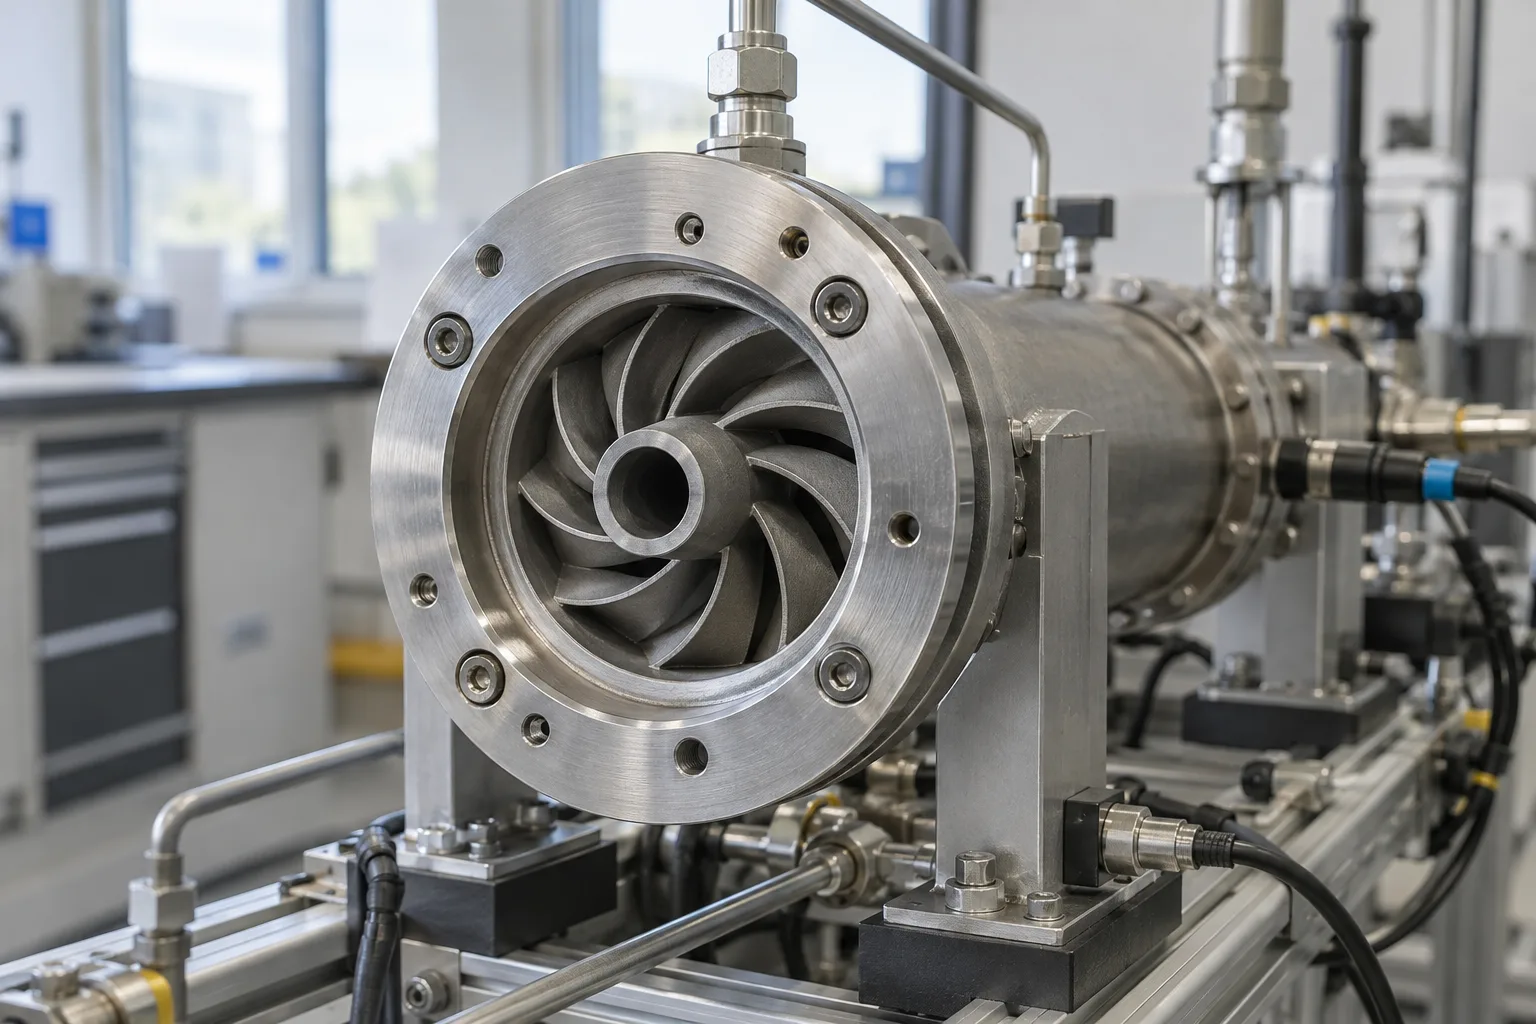
3D printed impeller installed in a propulsion test rig

Propulsion, flow and test instrumentation

Propulsion & Engine Hardware

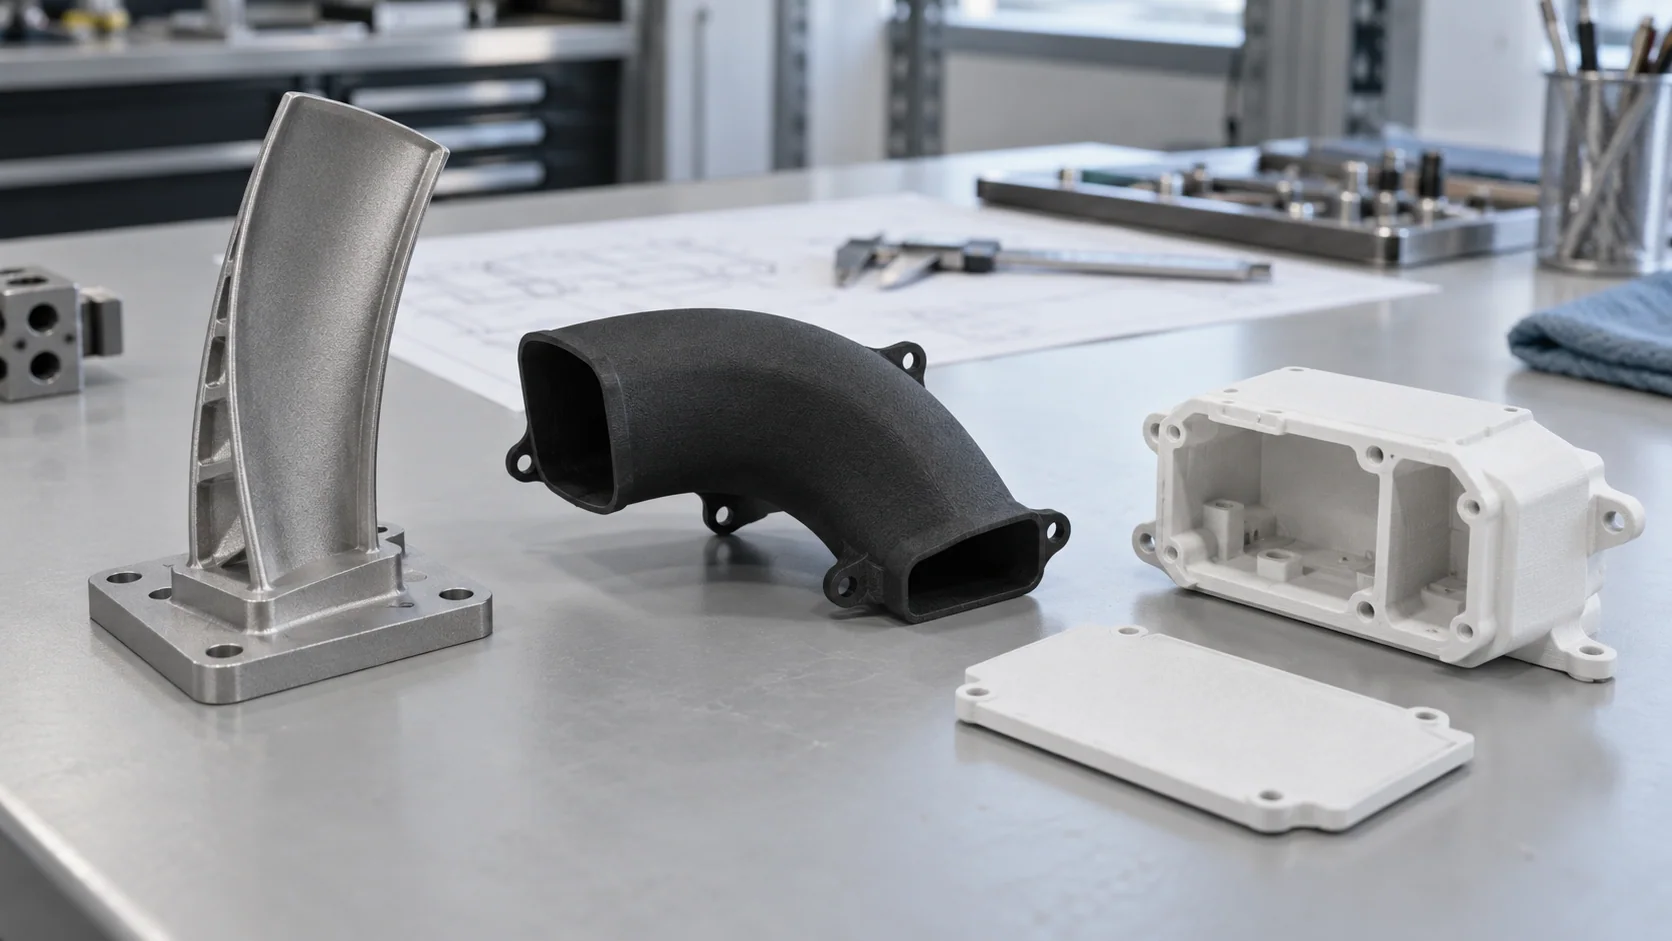
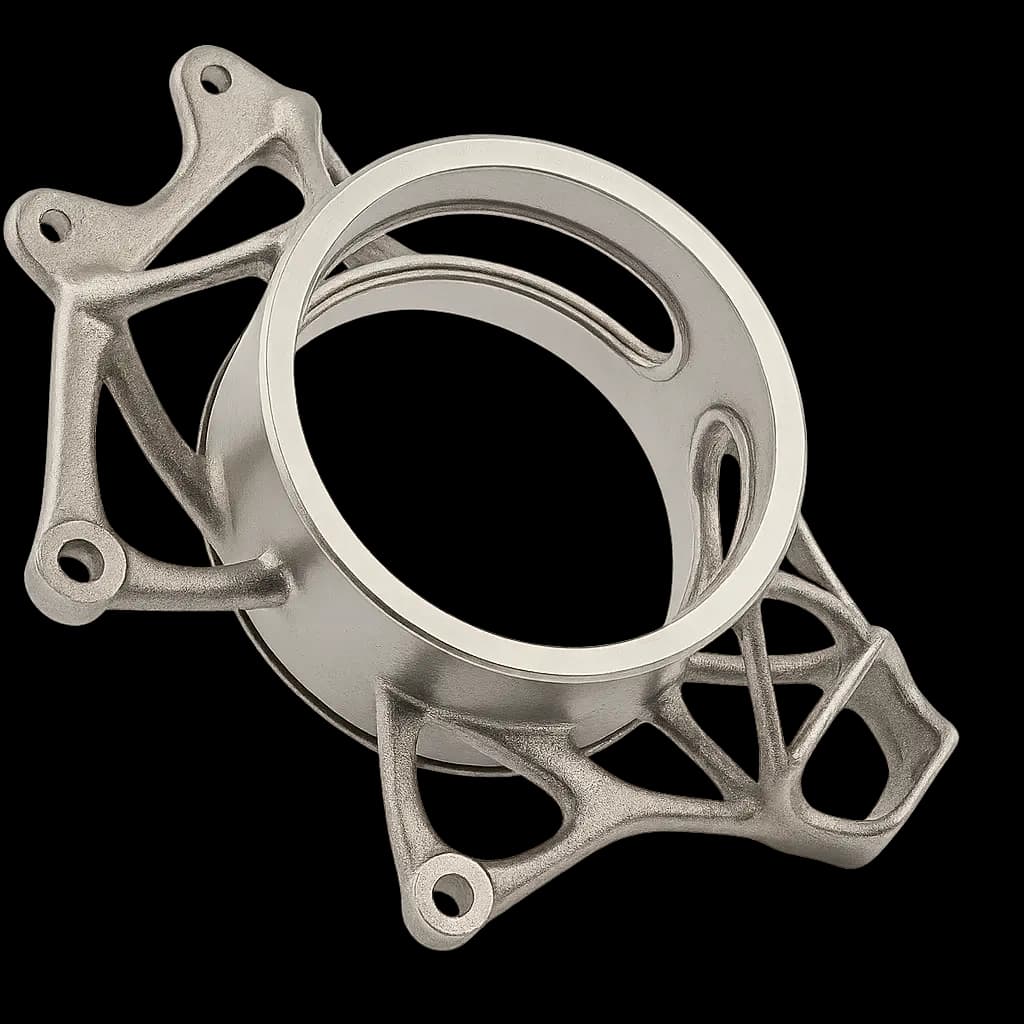
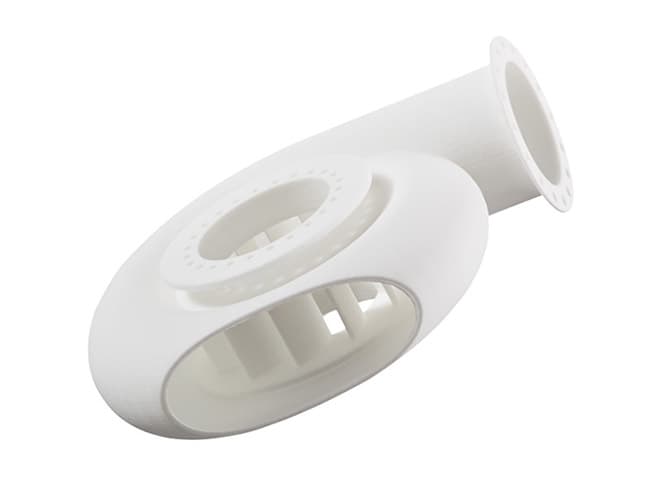
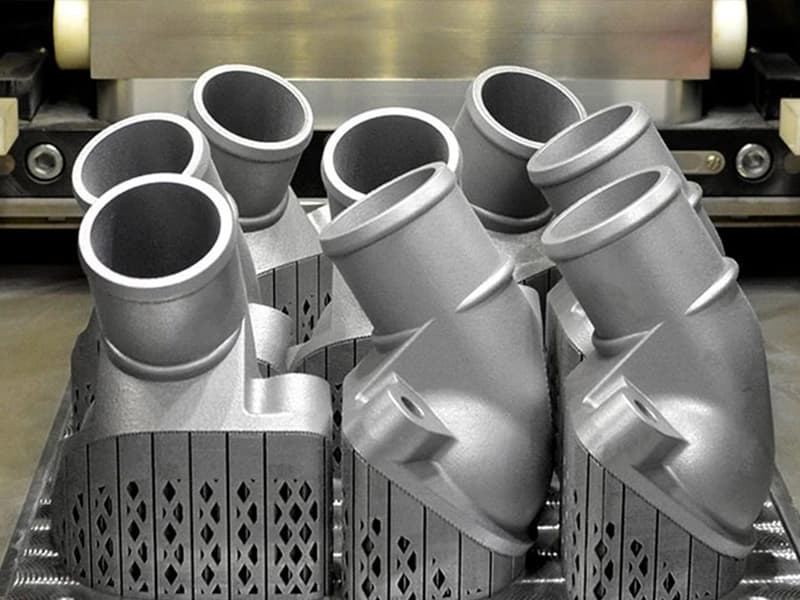
DMLS builds combustor swirlers in runs of 35, a radial fuel-pump impeller, pitot rakes and their sheaths for test instrumentation, and fan stator blade and hub sections for an electric aircraft, in 316L, 17-4 PH, AlSi10Mg and Ti6Al4V. EOS reports about 99.85% density for AlSi10Mg and about 100% for Ti64 and 316L, and after the supplier heat treatment heat-treated Ti64 exceeds ASTM F1472 / B348 wrought minimums. Heat treatment, HIP and machining are available.

Typical parts
Combustor swirlers, pump impellers, pitot rakes, stator sections, titanium brackets
Key properties
DMLS ±0.3% (min ±0.3 mm); MJF from 4 business days, DMLS 8–12
Material data
Ti6Al4V to ASTM F2924 / F3302; AlSi10Mg ~99.85% density (EOS)
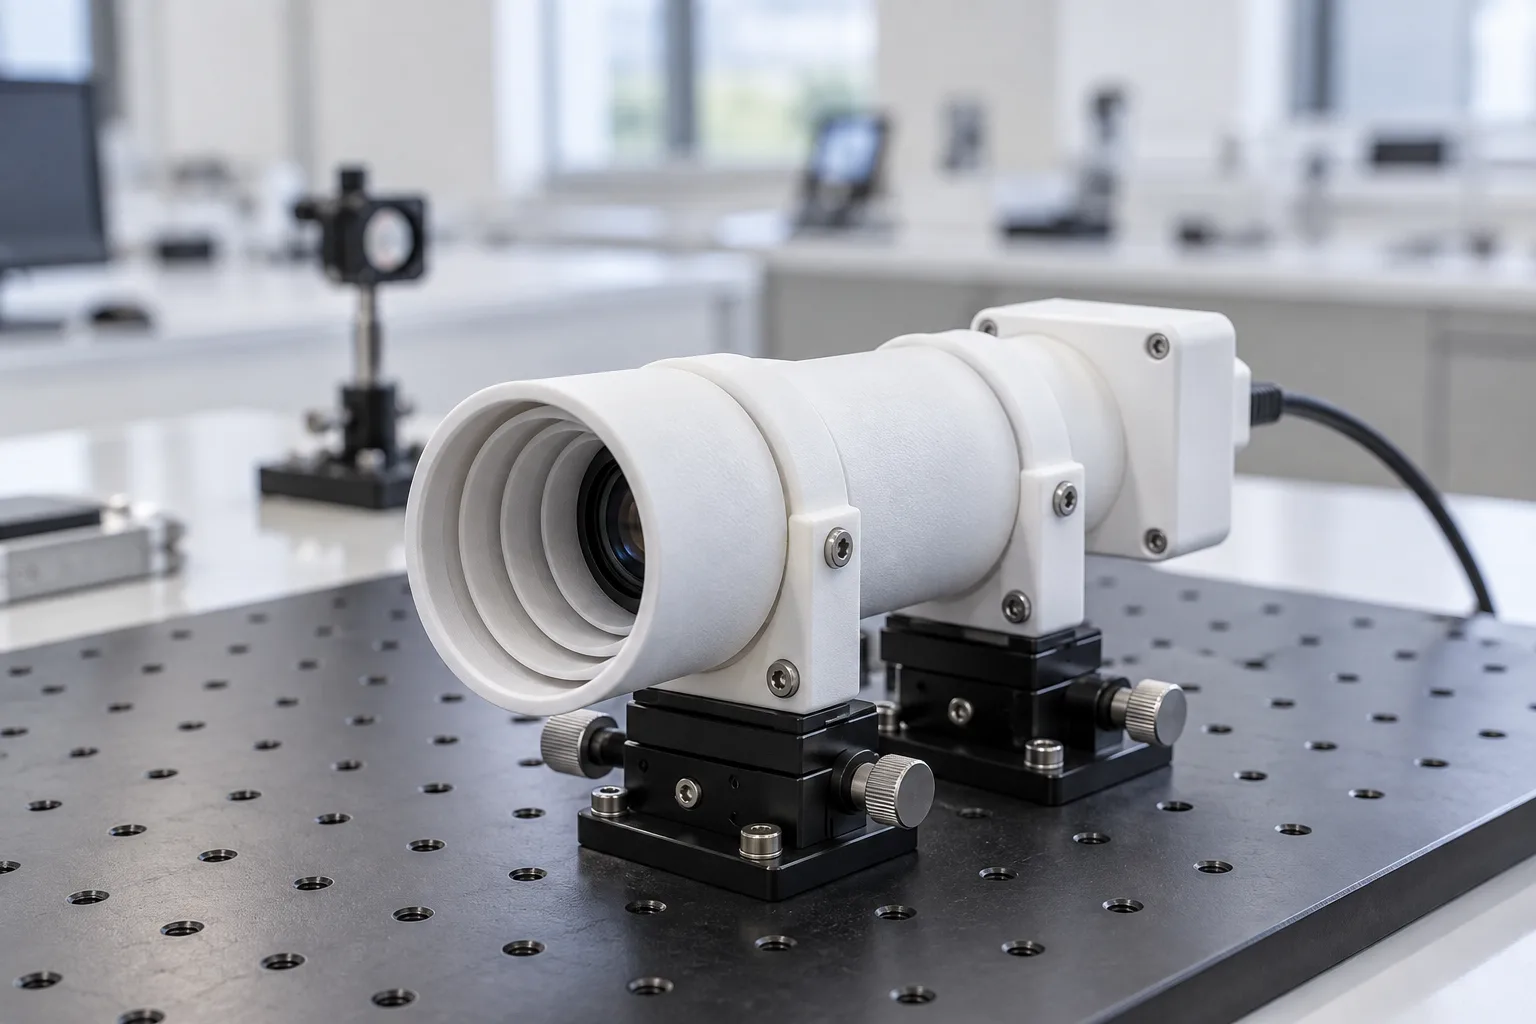
White SLS nylon sensor barrel and housing on an optical bench

Sensors, optics and test rigs

Sensor, Optical & Test Housings

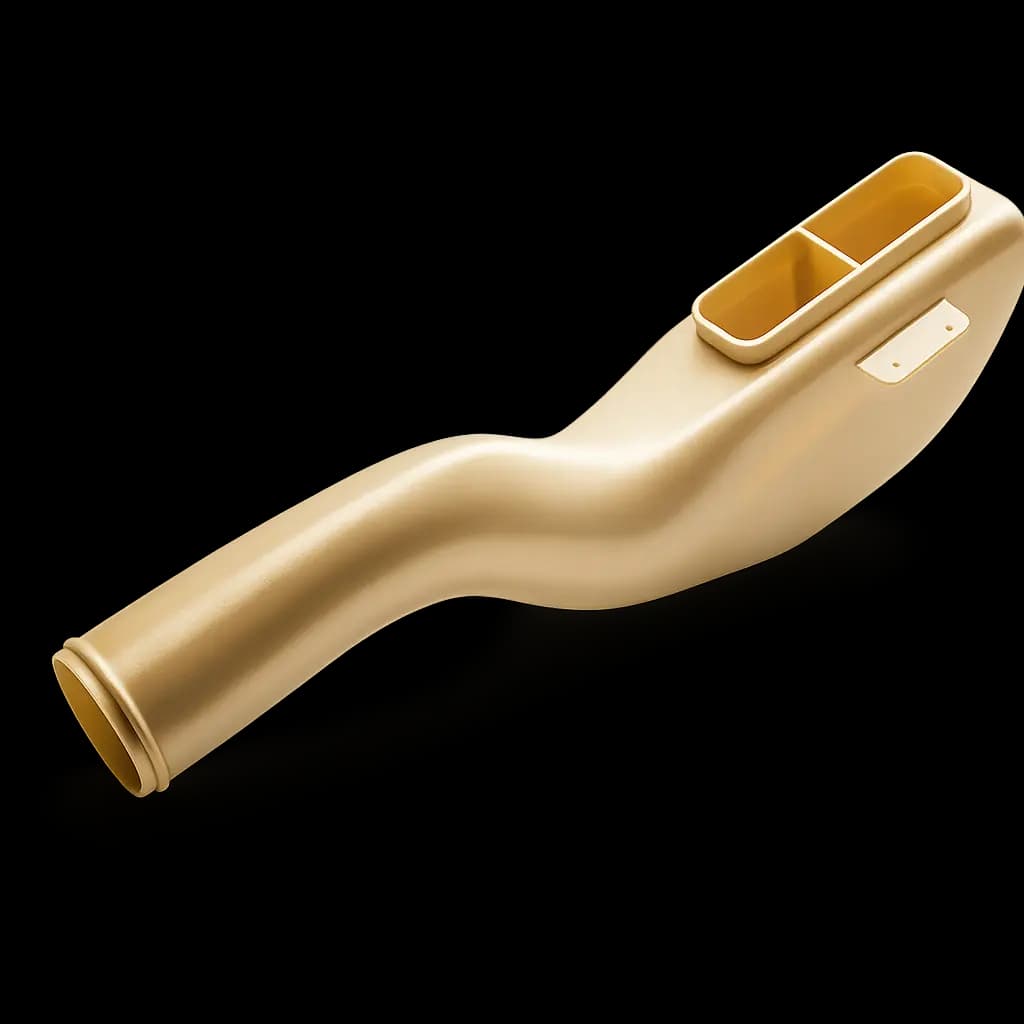
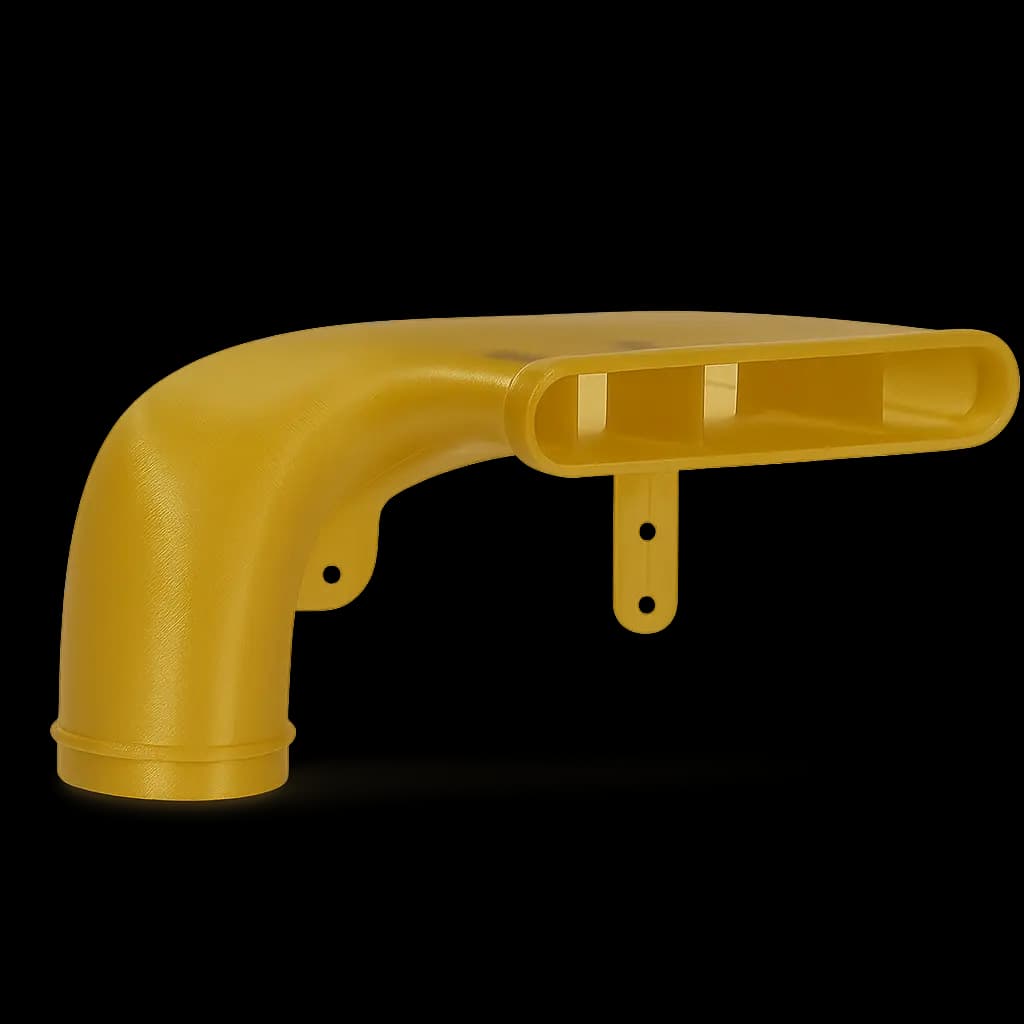
SLS PA12 makes complete sensor and optical test assemblies, with fore and aft barrels, baffles, detector housings and mounting brackets up to 325 mm. Two-shot housings are prototyped as a nylon first shot with an Agilus30 gasket, clear Accura ClearVue parts let engineers check fit and flow on flight hardware, and nylon ducts route cooling air to electronics heat sinks.

Typical parts
Optical barrels and baffles, detector housings, brackets, heat-sink ducts
Key properties
Assemblies up to 325 mm (SLS); SLA features from 0.1 mm
Material data
Accura ClearVue: 87.2% luminous transmittance; Agilus30 Shore A 30
Large SLA aeroshell fairing on a fit-check fixture

Large-format and metal prototypes

Large-Format Aerospace Prototyping

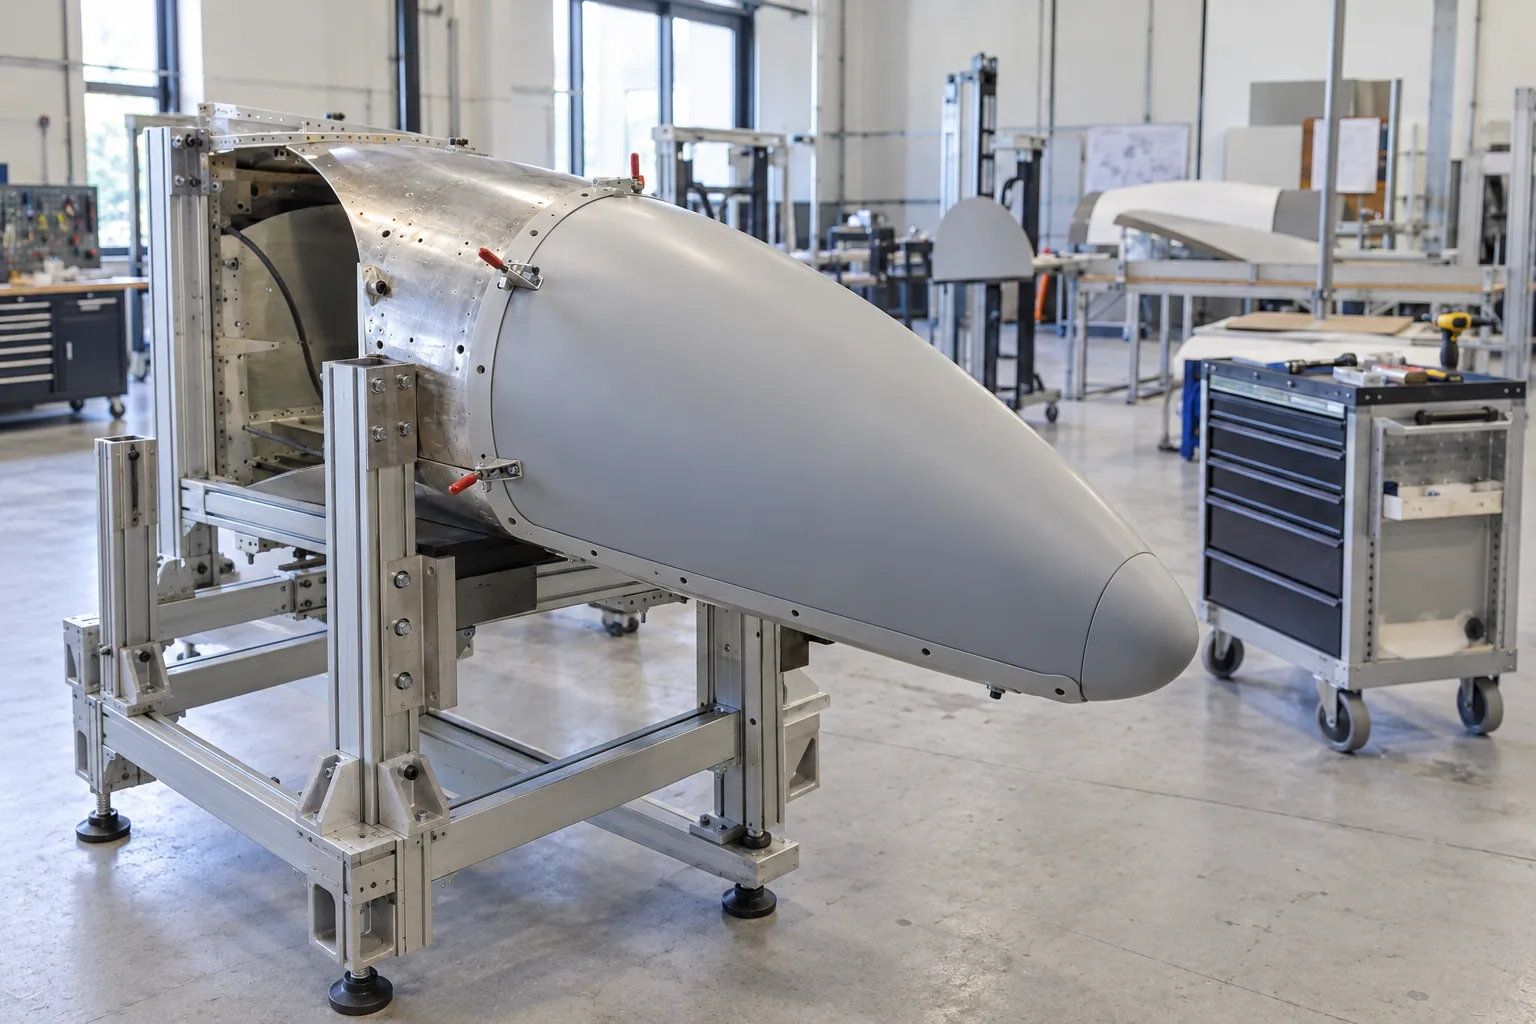
SLA builds aeroshells and fairings up to 930 mm and cabin trays over 600 mm in one piece, with ±0.25% (min ±0.25 mm) on critical features and a 1500 × 750 × 550 mm build volume. Features resolve down to 0.1 mm, prototypes are dimensionally checked on calibrated measuring equipment against your drawings, and High Temperature resin covers hot-air and thermal tests.

Typical parts
Aeroshells, fairings, cabin trays, large assemblies
Key properties
±0.25% (min ±0.25 mm); over 10 in ±0.4% (min ±0.5 mm); 0.1 mm features
Material data
High Temperature resin: 238 °C heat deflection at 0.45 MPa
Aircraft seat prototypes for interior fit checks

Fit checks and aerodynamic testing

Design Validation

High-definition SLA gives the surface quality and dimensional accuracy needed for fit-check prototypes and functional testing. 50-micron layers capture the fine surface detail and sharp edges that aerodynamic testing and assembly validation depend on, and clear and pigmented resins allow visual inspection of internal features and flow. Lead times from 2 business days and next day shipping across North America support fast iteration, and the resin range covers concept models through functional prototypes that simulate end-use material properties.

Typical parts
Interior fit-check models, aerodynamic test models, assembly mock-ups
Key properties
50–100 µm layers; Ra 0.5–2 µm as printed; ±0.25%; from 2 business days
Material data
Clear and pigmented resins, including Accura ClearVue
Case Studies

Aerospace Manufacturing Outcomes

Production and development work for aircraft interiors, drone and UAS manufacturers, and engine maintenance.

ULTEM 9085 Aircraft Enclosures: From Drawing to Inspected Samples

Case study

ULTEM 9085 Aircraft Enclosures: From Drawing to Inspected Samples

Black ULTEM enclosure samples brought mounting points and cable guides into one printed housing. Drawing-defined orientation, focused print trials and dimensional inspection turned the small internal features into a practical manufacturing route.

Key outcomes

  • Mounting and cable features printed together
  • Build orientation defined by the drawing
  • Samples inspected before evaluation
  • About 2½ working weeks including print trials
Explore the aircraft enclosure case study
Aircraft and UAV Prototypes in Printed Aluminum and Nylon

Case study

Aircraft and UAV Prototypes in Printed Aluminum and Nylon

Aluminum airfoil sections, nylon cooling ducts and UAV housings show how different prototypes answer different design questions. Separate projects connect material choice, assembly access and finishing to the parts an engineering team needs to evaluate.

Key outcomes

  • Curved metal geometry in DMLS AlSi10Mg
  • Cooling shrouds and housings in SLS PA12
  • UAV body and access parts finished in eight business days
  • Design changes without mould tooling
Explore the aircraft and UAV prototypes
Production Drone Parts in SLS PA12, With Assembly Built In

Case study

Production Drone Parts in SLS PA12, With Assembly Built In

Mounts, battery enclosures, access panels and sensor hardware combine lightweight nylon geometry with drawing-specified stainless inserts. Printing, black dyeing and hardware installation support production batches sized around assembly needs.

Key outcomes

  • Production quantities in the hundreds
  • Stainless threaded inserts installed to drawing
  • Selected cover batches finished in four to five business days
  • Revised geometry without new tooling
Explore the drone production case study
A Stainless Test Fixture: Print the Passages, Machine the Seals

Case study

A Stainless Test Fixture: Print the Passages, Machine the Seals

A consolidated engine-maintenance fixture combines internal air passages with precise ports and seal seats. Forge printed the 316L body with machining allowance, then finished the holes, threads and O-ring grooves to the drawing.

Key outcomes

  • Three fixtures consolidated into one tool
  • Internal air passages printed in one piece
  • Bores, threads and O-ring grooves finished to drawing
  • Printing and machining planned as one job
Explore the stainless test fixture case study
Material Library

Materials for Aerospace Parts

FST-rated thermoplastics, engineering nylons and aerospace alloys, chosen for weight, heat and chemical resistance. Compare full properties on each material page.

Explore the complete material matrix. Compare certifications, mechanical properties and application fit across the full portfolio before locking your production material stack.

Start a quote

Ready to Manufacture Your Aerospace Parts?

Upload your CAD files for an instant quote or speak with our application engineers about your specific requirements.

  • Instant pricing with automated manufacturability analysis
  • Production workflows built for repeatable quality
  • Engineering support from prototype to production
Talk to an Engineer

Create an account to upload CAD

STEP, STL, OBJ, 3MF and IGES supported

Manufacturing technologies
6
Engineering materials
50+
Part quantities
1-500+