Energy & Clean Tech 3D Printing for Fuel Cell, Hydrogen and Power Generation Parts

Production covers, enclosures, engine and flow parts for fuel cell, hydrogen, power generation and grid equipment makers, from validation builds to repeat production lots.

  • Drawing-controlled production lots with part marking and labelled packaging.
  • Nylon, flame-rated ULTEM, UV-stable ASA, clear resin and metal.
  • Repeat orders without investing in mould tooling.
Energy & Clean Tech 3D Printing Solutions
Energy & Clean Tech Overview

From validation hardware to production lots

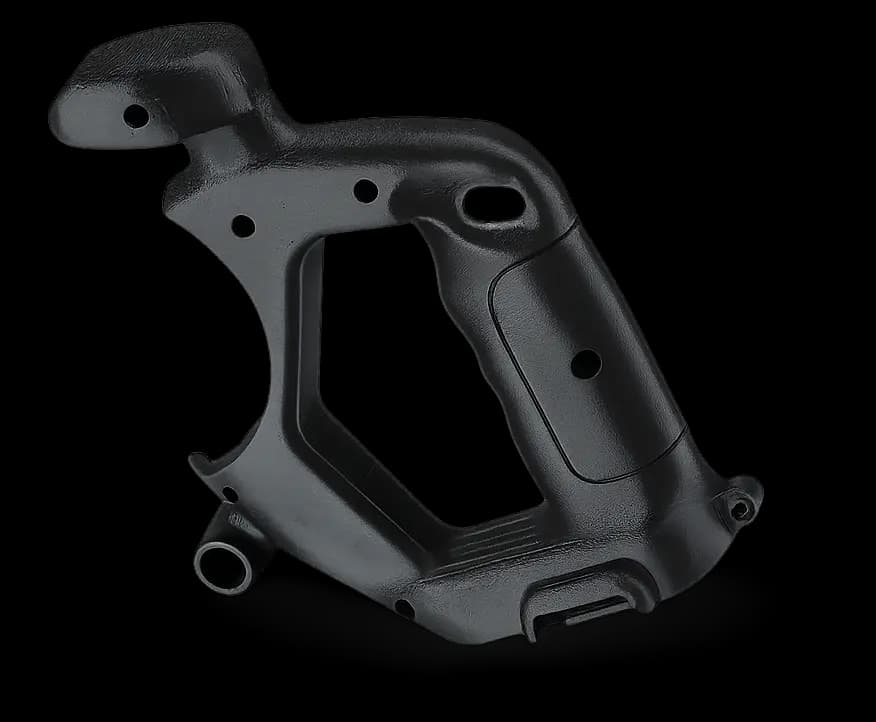
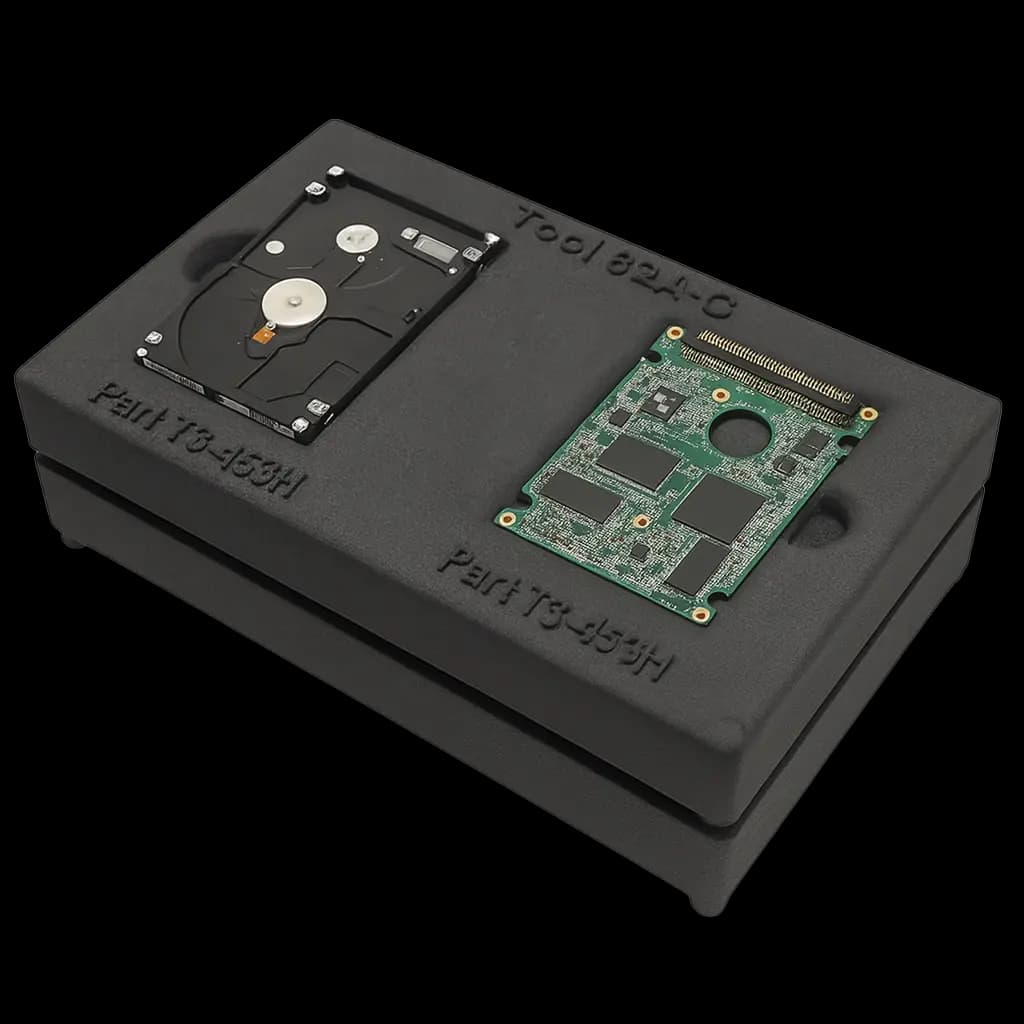
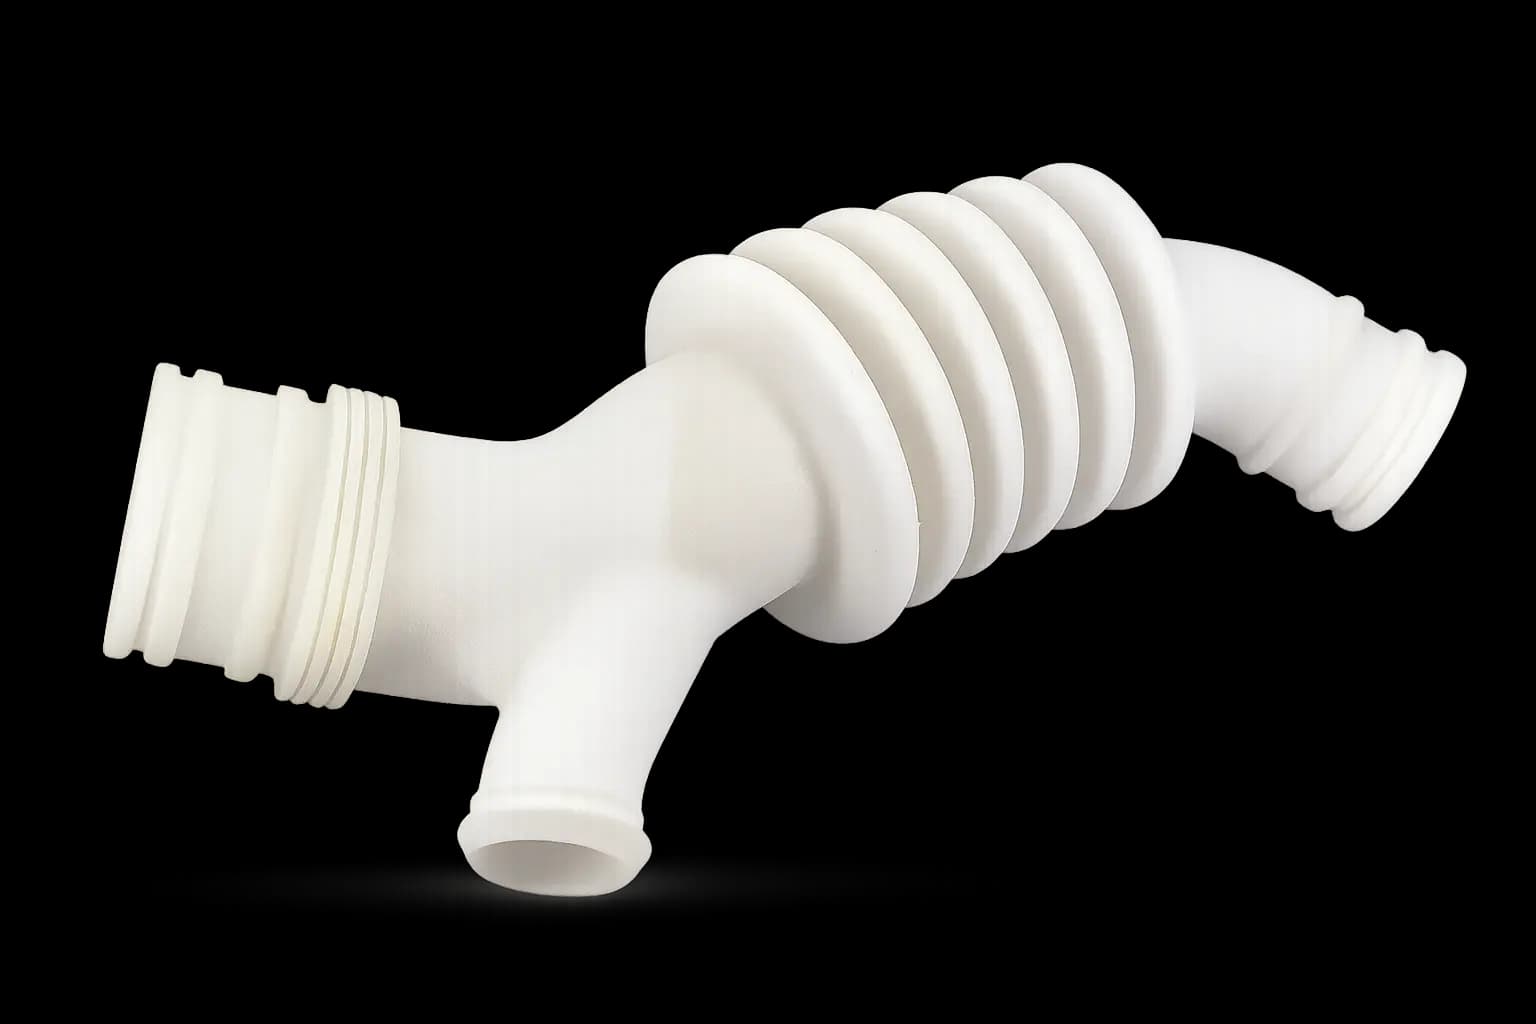
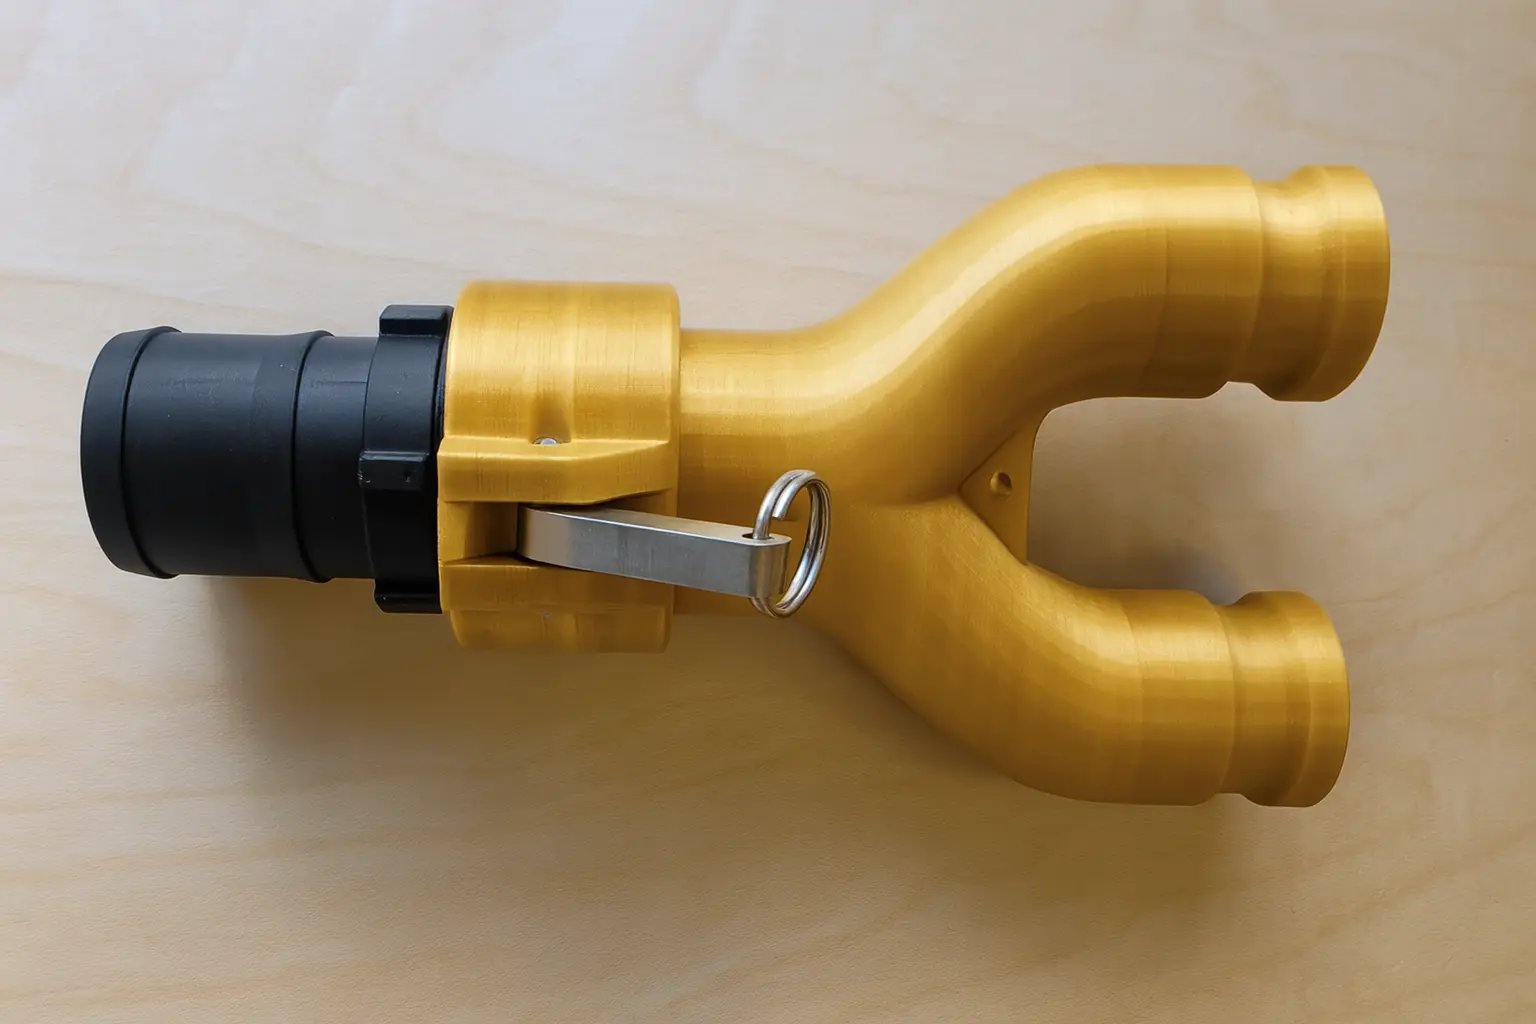
Clean tech hardware changes faster than mould tooling can be justified, and much of it stays printed in production. We make touch-proof covers for high-voltage connections in fuel cell equipment, injector adapters for hydrogen engines, clear fittings for development test rounds, pistons and valve parts for power generation equipment, charger and converter enclosures, separator grids for energy recovery cores, and ASA parts for power equipment, more than 600 from one unchanged file. We build them with MJF, SLS, FDM, SLA and DMLS, to your drawings, in materials chosen for heat, flame, UV and chemical exposure.

Where additive creates leverage

Change the design between test rounds, not the tooling

Forge Labs helps teams move from design validation to production-ready parts without waiting on tooling lead times. Consolidated assemblies, lighter parts, and faster revisions give engineering teams more control over schedule, cost, and performance.

Key manufacturing benefits

  • Move from validation builds to pilot and repeat production lots without mould tooling.
  • Order production parts against your drawing, with GD&T callouts, part marking and labelled packaging.
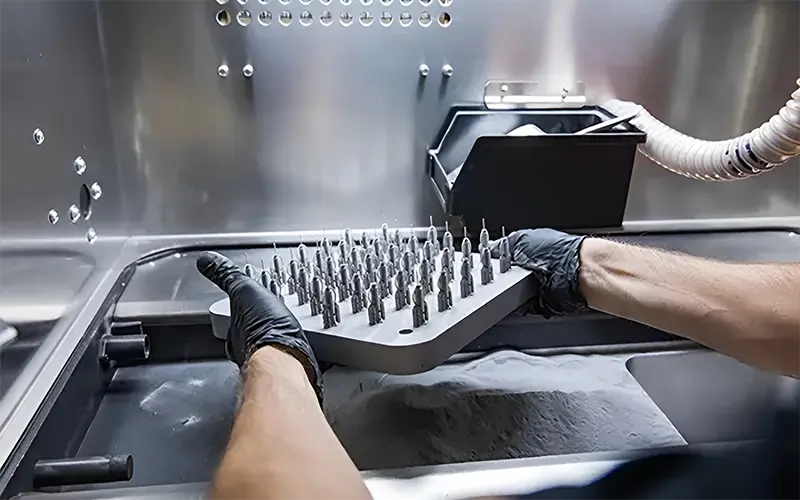
  • Print metal engine and flow parts that were drawn for machining, in aluminium, stainless steel and titanium.
  • See inside development fittings with clear resin parts, then move a revised design to nylon.
  • Revise fuel cell, hydrogen and enclosure designs between test rounds without tooling changes.
  • Reorder outdoor and field parts from your order history, with next day shipping across North America.
Energy & Clean Tech Manufacturing Process 1
Energy & Clean Tech Manufacturing Process 2
Energy & Clean Tech Manufacturing Process 3
Energy & Clean Tech Manufacturing Process 4
Quality and compliance

Production discipline for energy hardware

Energy hardware combines thermal, electrical and environmental demands, and production customers send drawings, marking specifications and compliance requirements. We work to them, from first article to repeat lots.

ISO 9001-aligned inspection
Parts are inspected under ISO 9001-aligned processes against your drawing, including GD&T callouts and tolerance classes.
Flame-rated materials
ULTEM 1010 and ULTEM 9085 carry UL 94 V-0 material ratings, with supplier data to support your own product certification.
Part marking and packaging
Part numbers marked on the part and on labelled packaging to your specification, with parts supplied clean and packed against shipping damage.
Compliance declarations
Material compliance declarations such as REACH supplied with first article delivery when your drawing calls for them.
Material certifications
Documented material properties for energy-critical applications, with material certifications on request.
Ordering and repeat lots
Upload STEP, STL, OBJ or IGES files with drawings and tolerance callouts, add first article inspection or production sampling where offered, and reorder lots from your order history, with next day shipping across North America.
Manufacturing Capabilities

3D Printed Parts for Energy and Clean Tech Equipment

The energy parts we make most often, with the processes, materials and material data behind each.

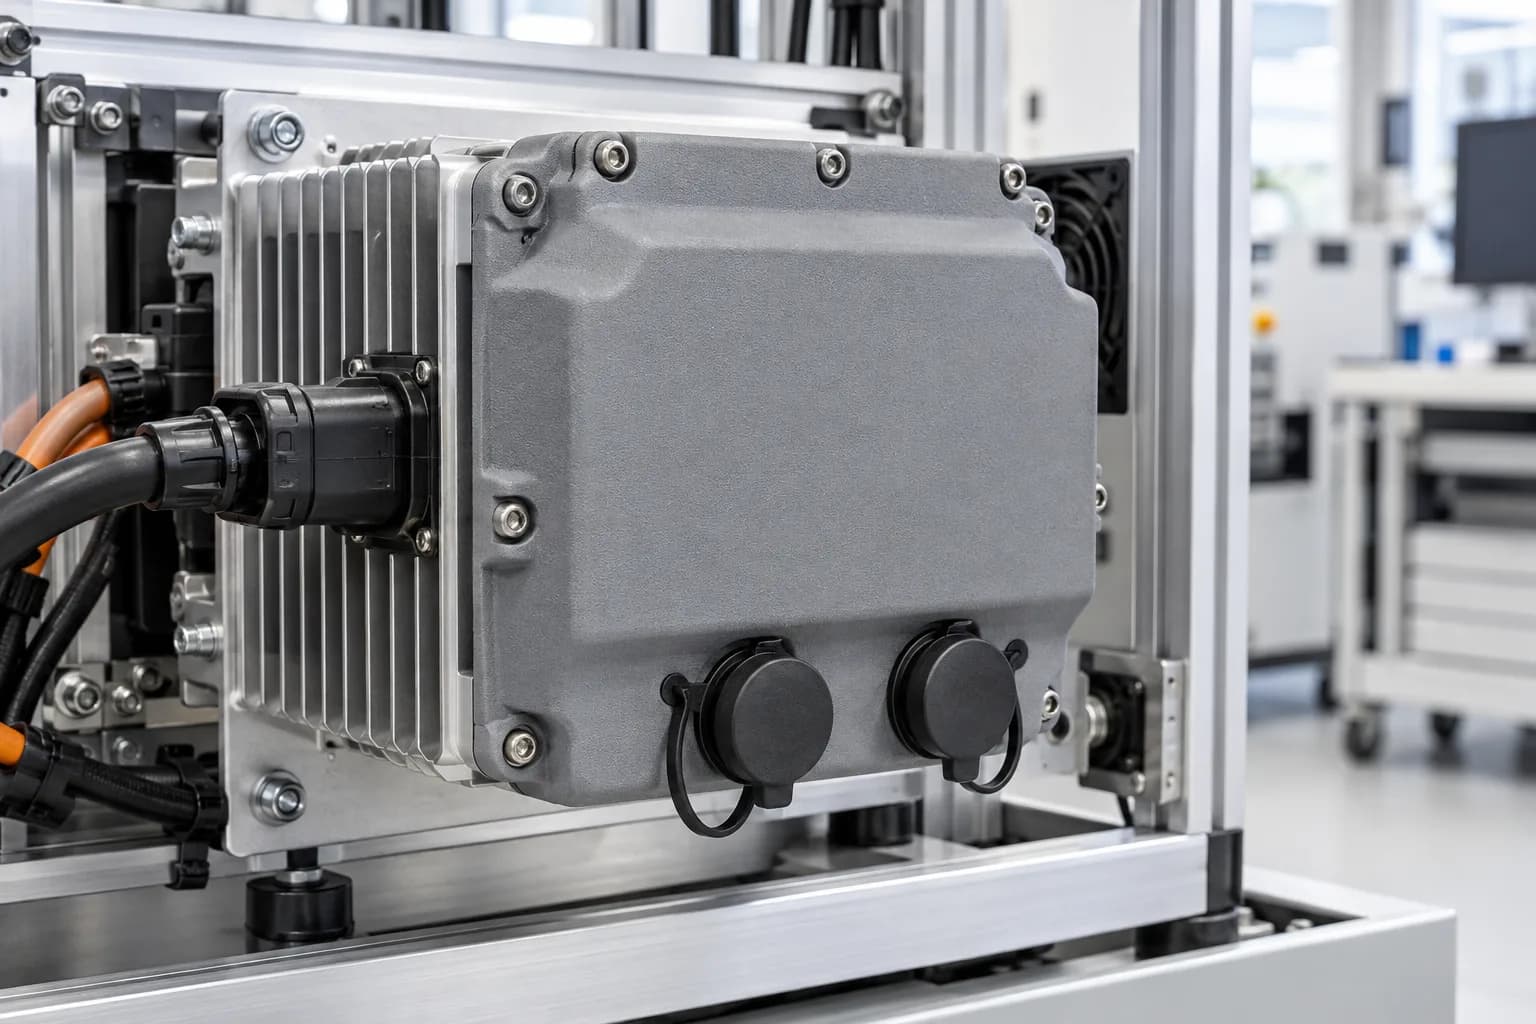
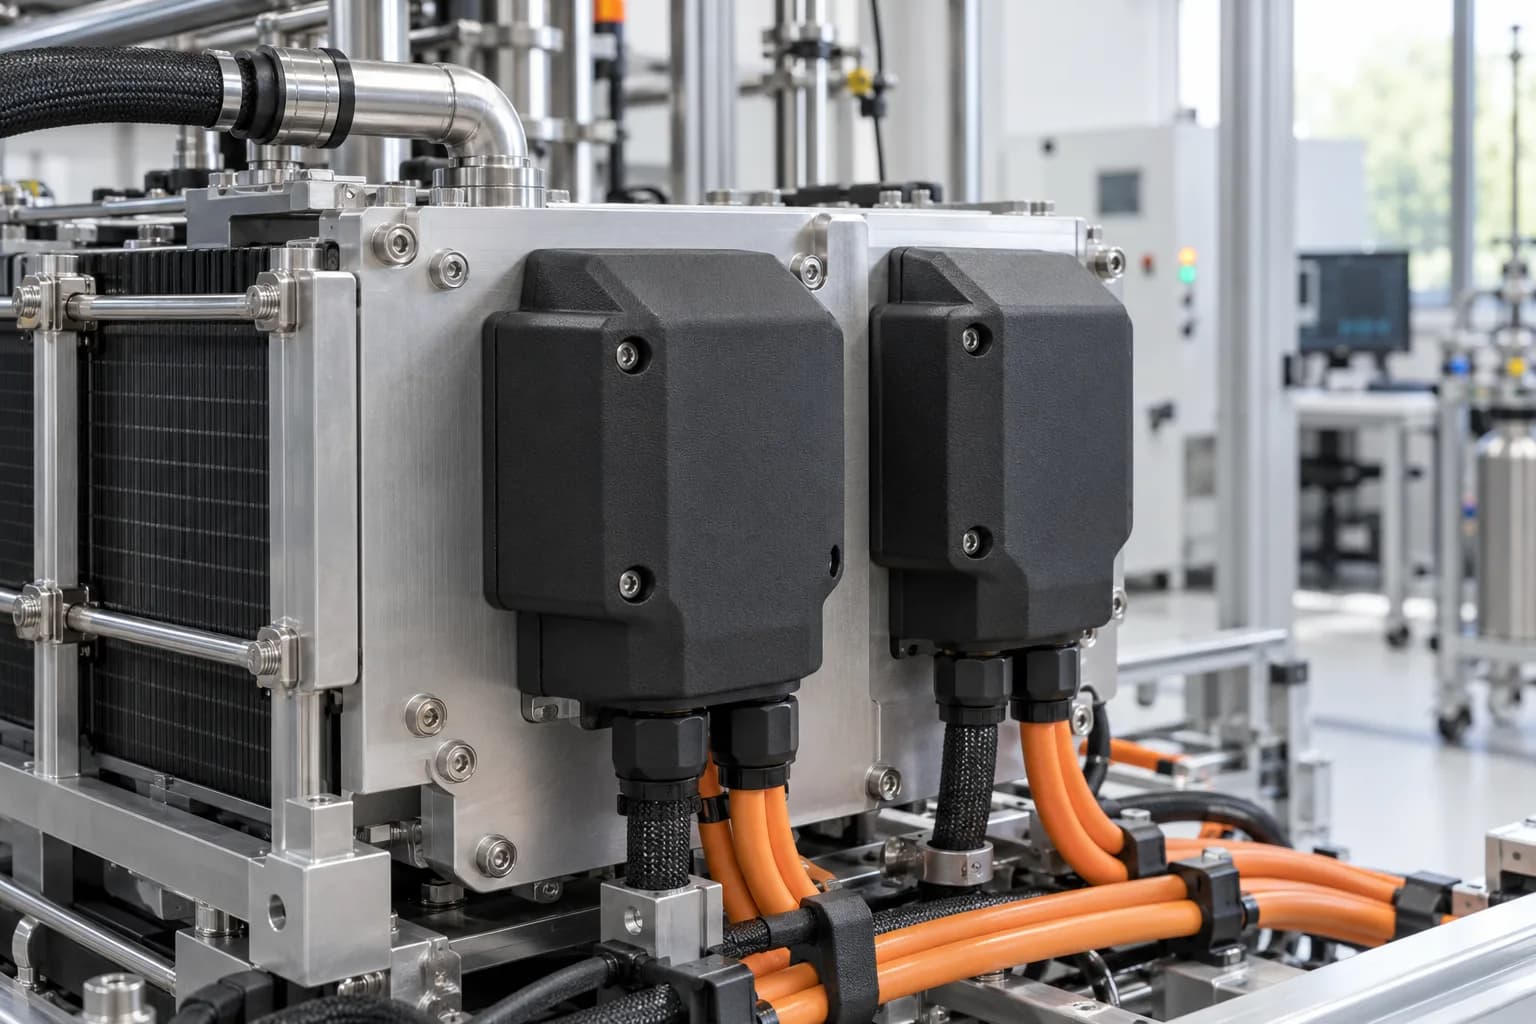
Black MJF nylon covers fitted over electrical connections on a fuel cell module

Fuel cells and hydrogen

Fuel Cell & Hydrogen Systems

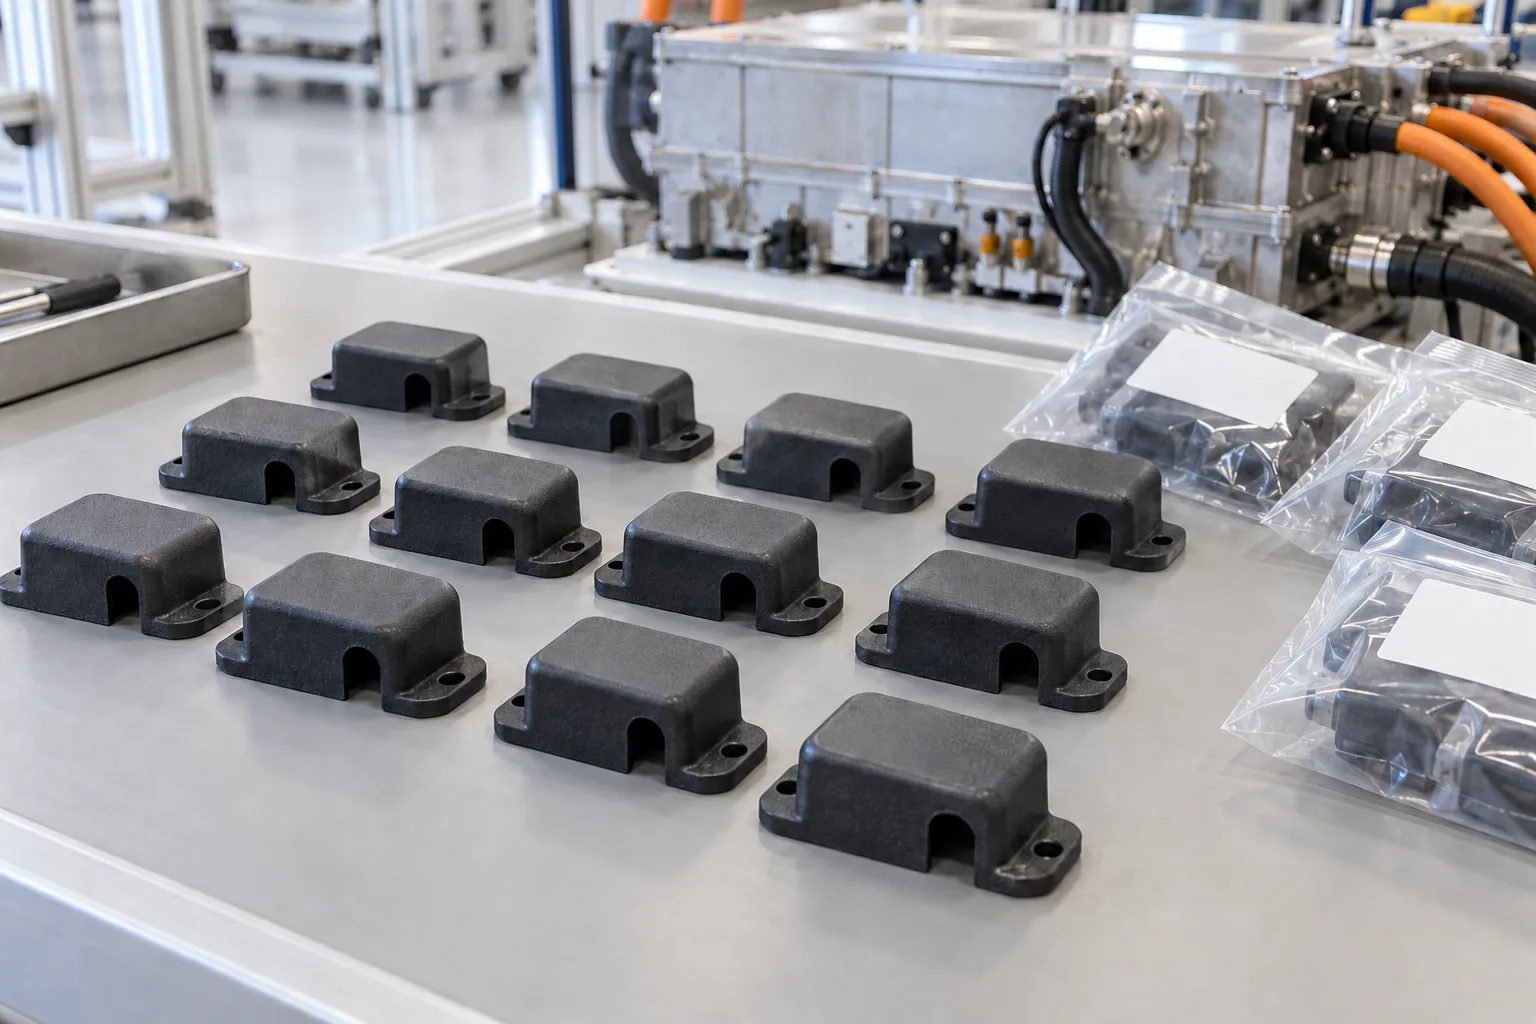
MJF PA12 makes touch-proof covers for high-voltage connections and low-voltage covers for fuel cell equipment, ordered as production parts to the customer's drawing. ULTEM 9085 makes flame-rated brackets, and DMLS aluminium makes injector adapters for hydrogen engine conversions.

Typical parts
High- and low-voltage covers, brackets, injector adapters
Key properties
MJF ±0.3% (min ±0.5 mm); production lots to customer drawings
Material data
ULTEM 9085: UL 94 V-0 from 0.508 mm
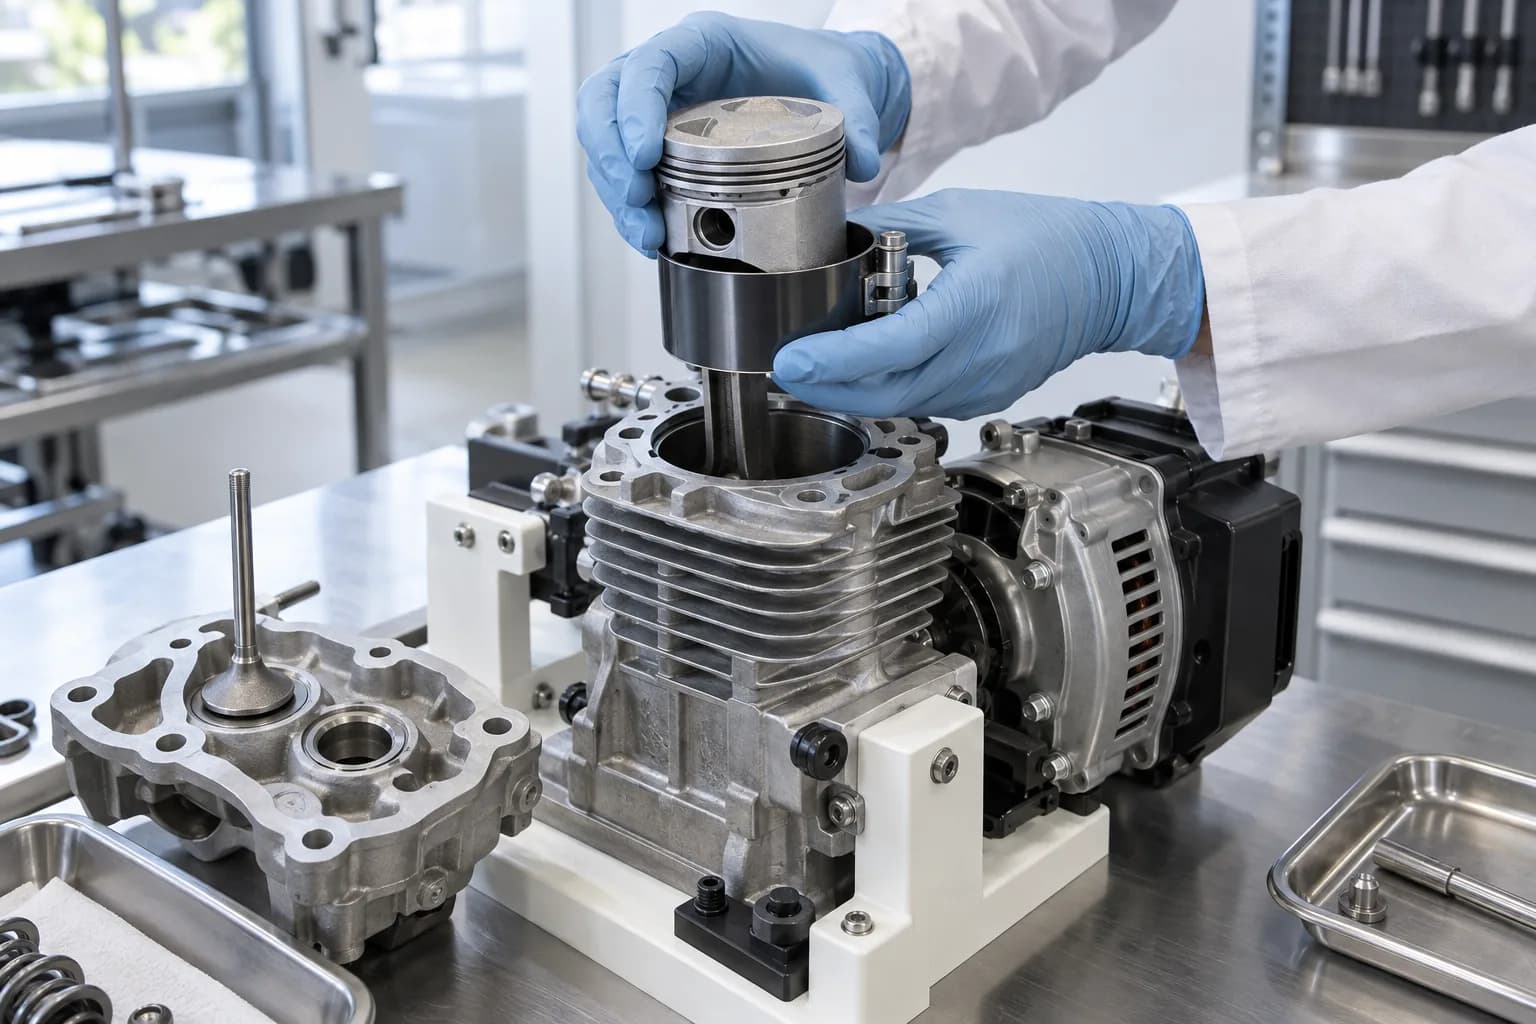
DMLS aluminium piston and stainless steel valve parts on an engine test stand

Engines, pistons and valves

Power Generation & Engine Components

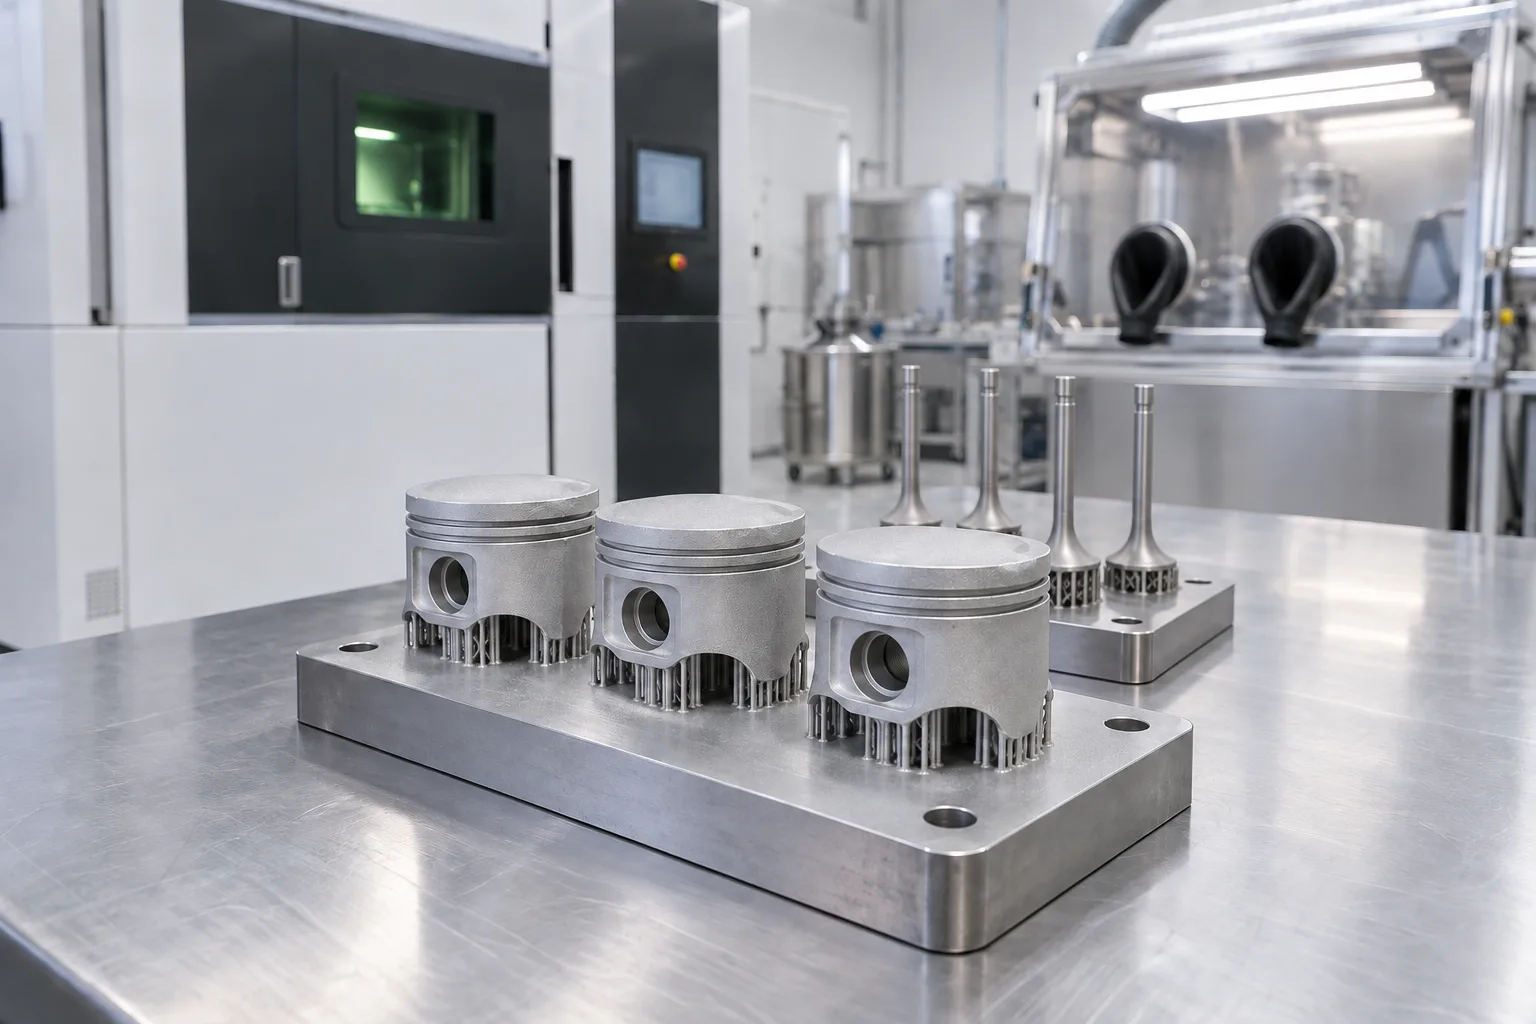
DMLS produces pistons and counterweights, valve plates and heads, valve seal protectors and trigger wheels for power generation equipment, in aluminium, 316L and 17-4 PH stainless steel. Parts drawn for machining in wrought aluminium or hot-rolled steel are printed to shape, then ring grooves, threads and narrow slits are finished by machining, tapping or wire EDM. An intake fitting drawn in 6061-T6 aluminium is made in ULTEM 9085 by FDM.

Typical parts
Pistons, valve parts, seal protectors, intake fittings
Key properties
DMLS ±0.3% (min ±0.3 mm); grooves and threads machined after printing
Material data
AlSi10Mg, 316L and 17-4 PH stainless; ULTEM 9085 UL 94 V-0
SLS nylon charger enclosure halves with TPU connector dust caps

Chargers, converters and controls

Chargers & Power Electronics Enclosures

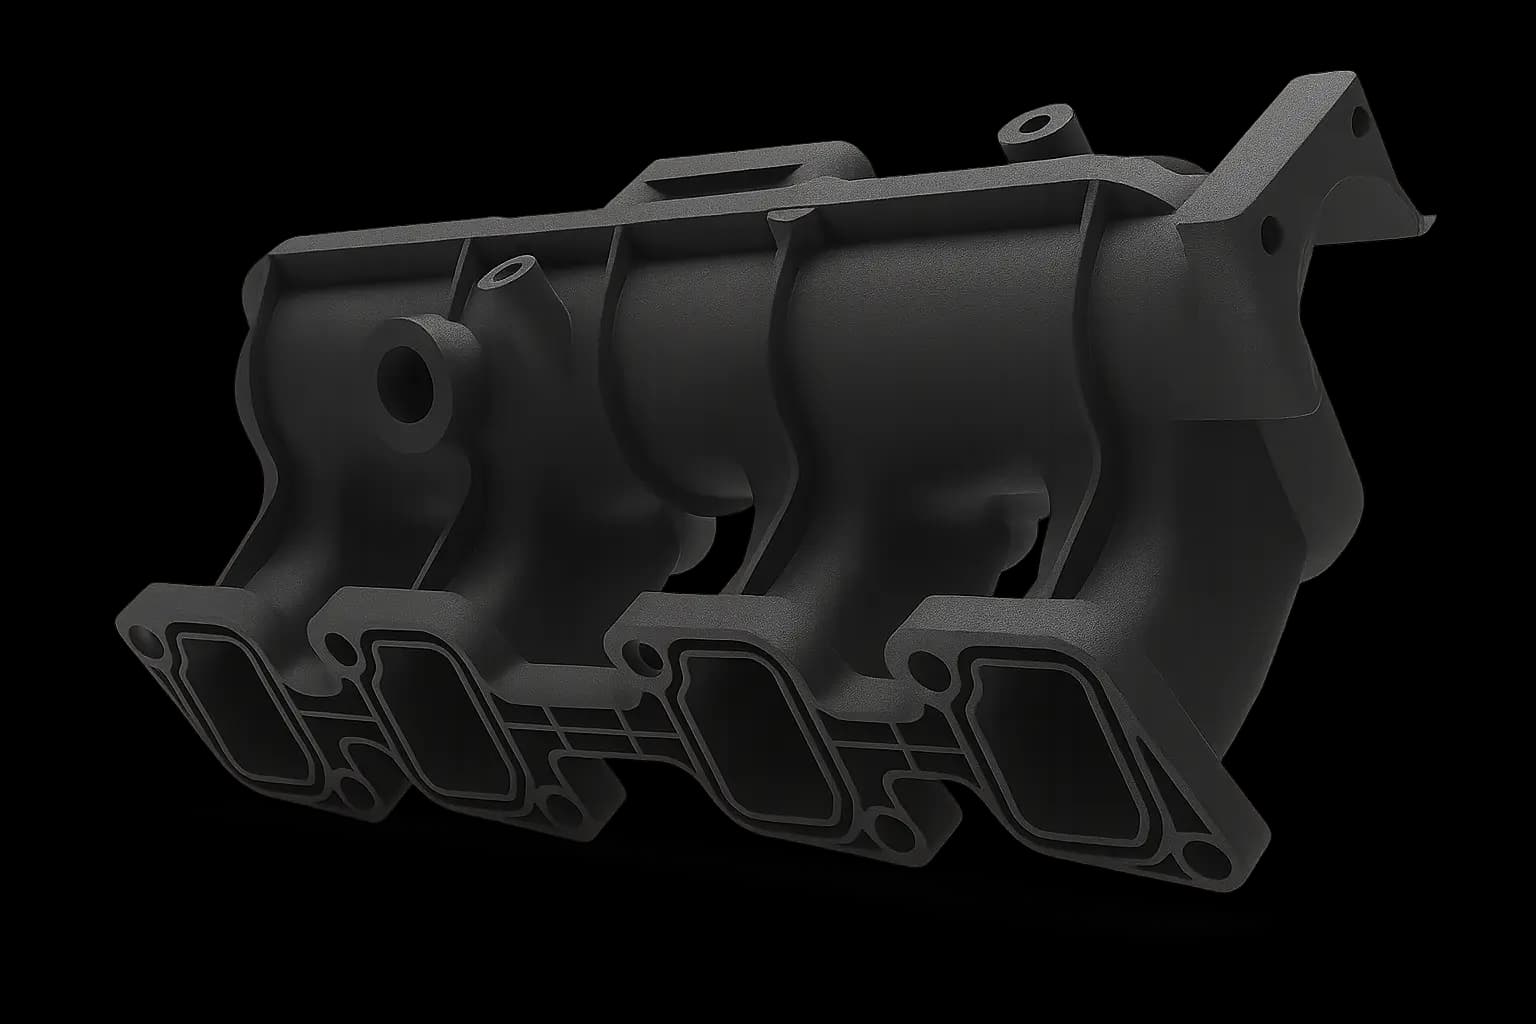
SLS PA12 produces enclosures for battery chargers and power converters, split housings that keep pneumatic and electronic sides apart, and accessories for outdoor units such as snow catches. Flexible TPU 88A makes dust caps and seals for connectors, and static-dissipative PA12 ESD and ABS-ESD7 protect electronics during assembly.

Typical parts
Charger and converter enclosures, split housings, connector dust caps
Key properties
SLS ±0.3% (min ±0.3 mm); no support structures
Material data
TPU 88A: no cut growth after 100k flex cycles; PA12 ESD 1.2 × 10⁷ Ω/sq
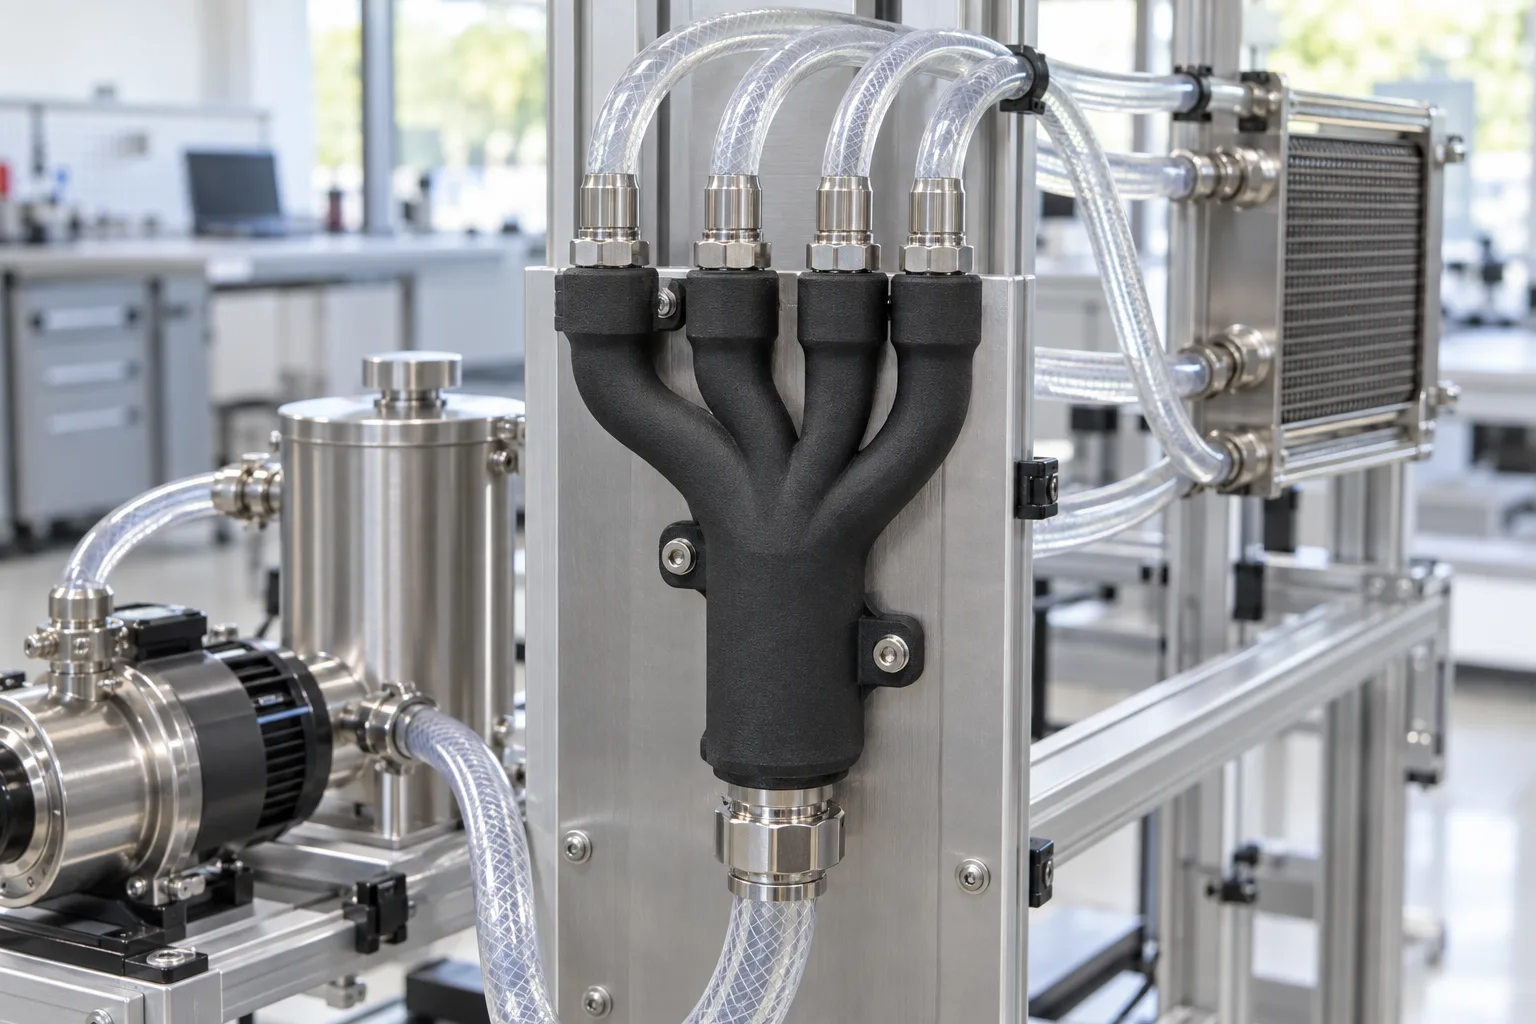
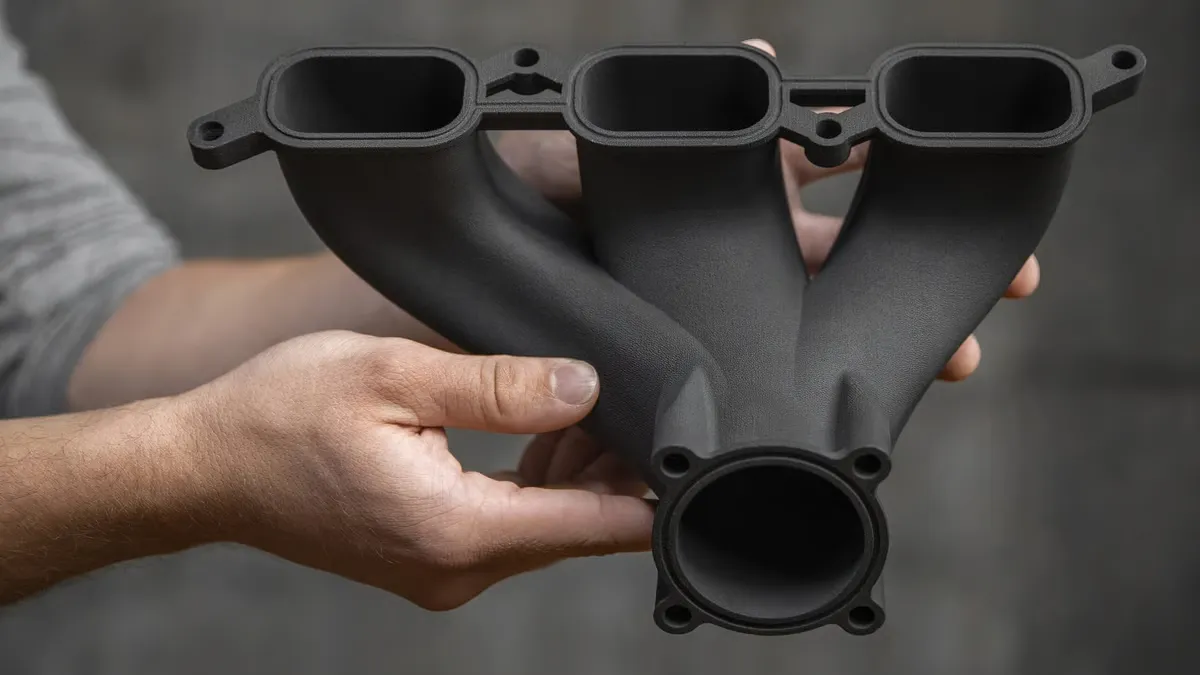
Printed separator grids, pin-fin cold plate and nylon manifold block

Cooling, heat exchange and recovery

Thermal Management & Energy Recovery

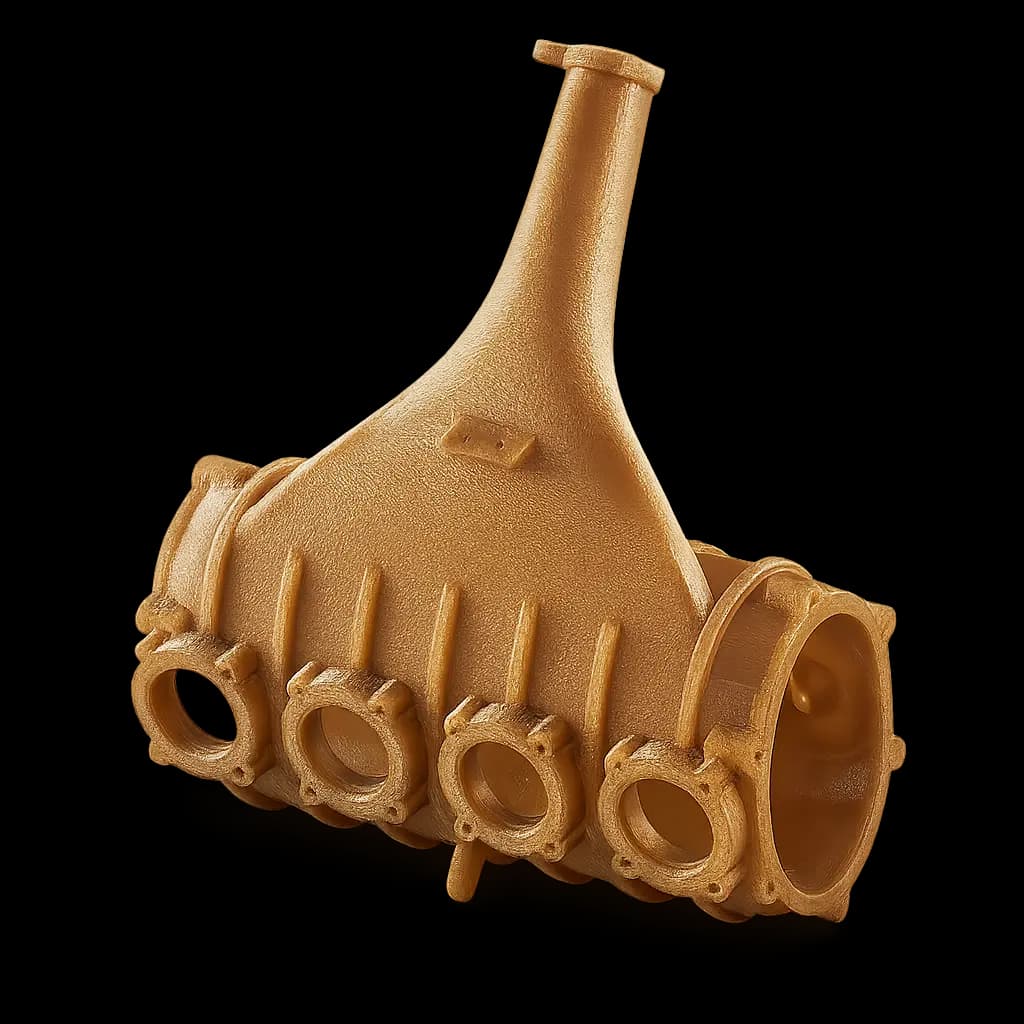
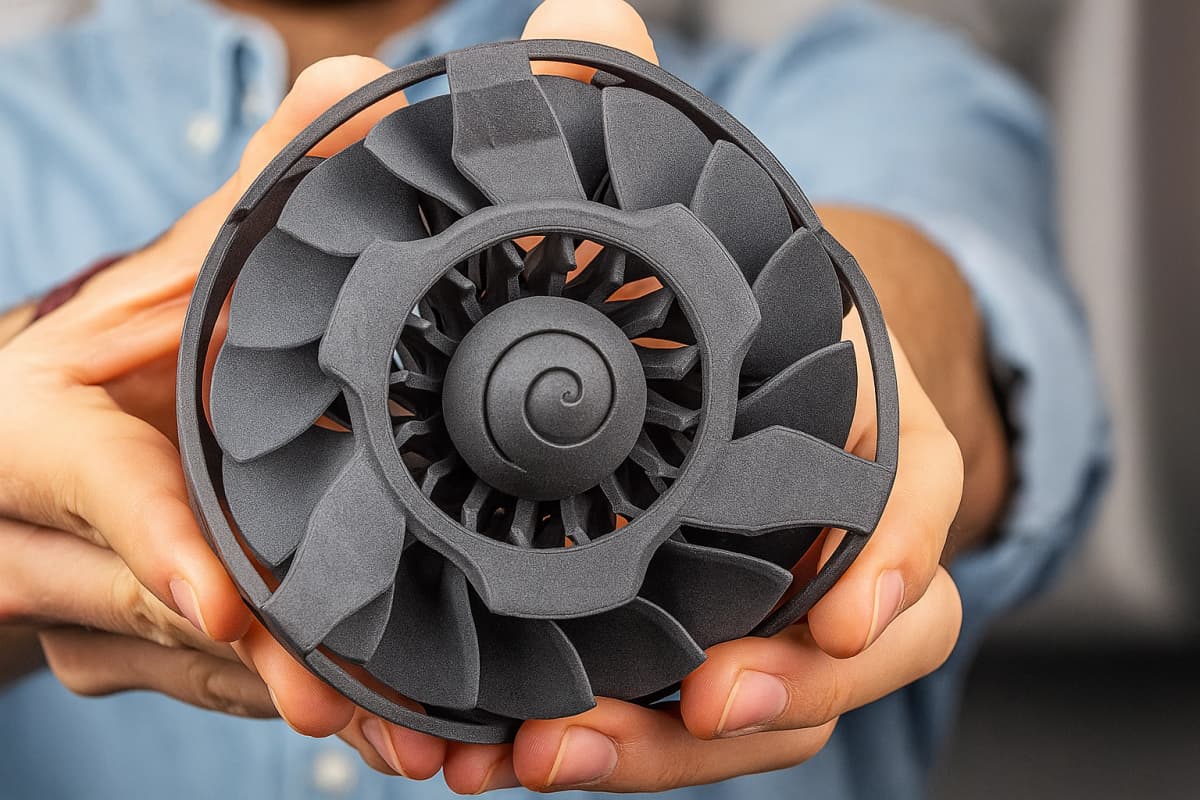
Thin separator grids for energy recovery cores are printed in runs of 150, so each core size can change without new tooling. For two-phase cooling, SLA makes evaporator plates with dense pin arrays and SLS makes vapour manifolds with internal passages, and DMLS aluminium carries heat where a metal part is needed.

Typical parts
Separator grids, evaporator plates, vapour manifolds, heat spreaders
Key properties
Internal passages without supports (SLS); runs of 150 and more
Material data
AlSi10Mg: 100–110 W/m·K as built, up to 165 W/m·K heat treated
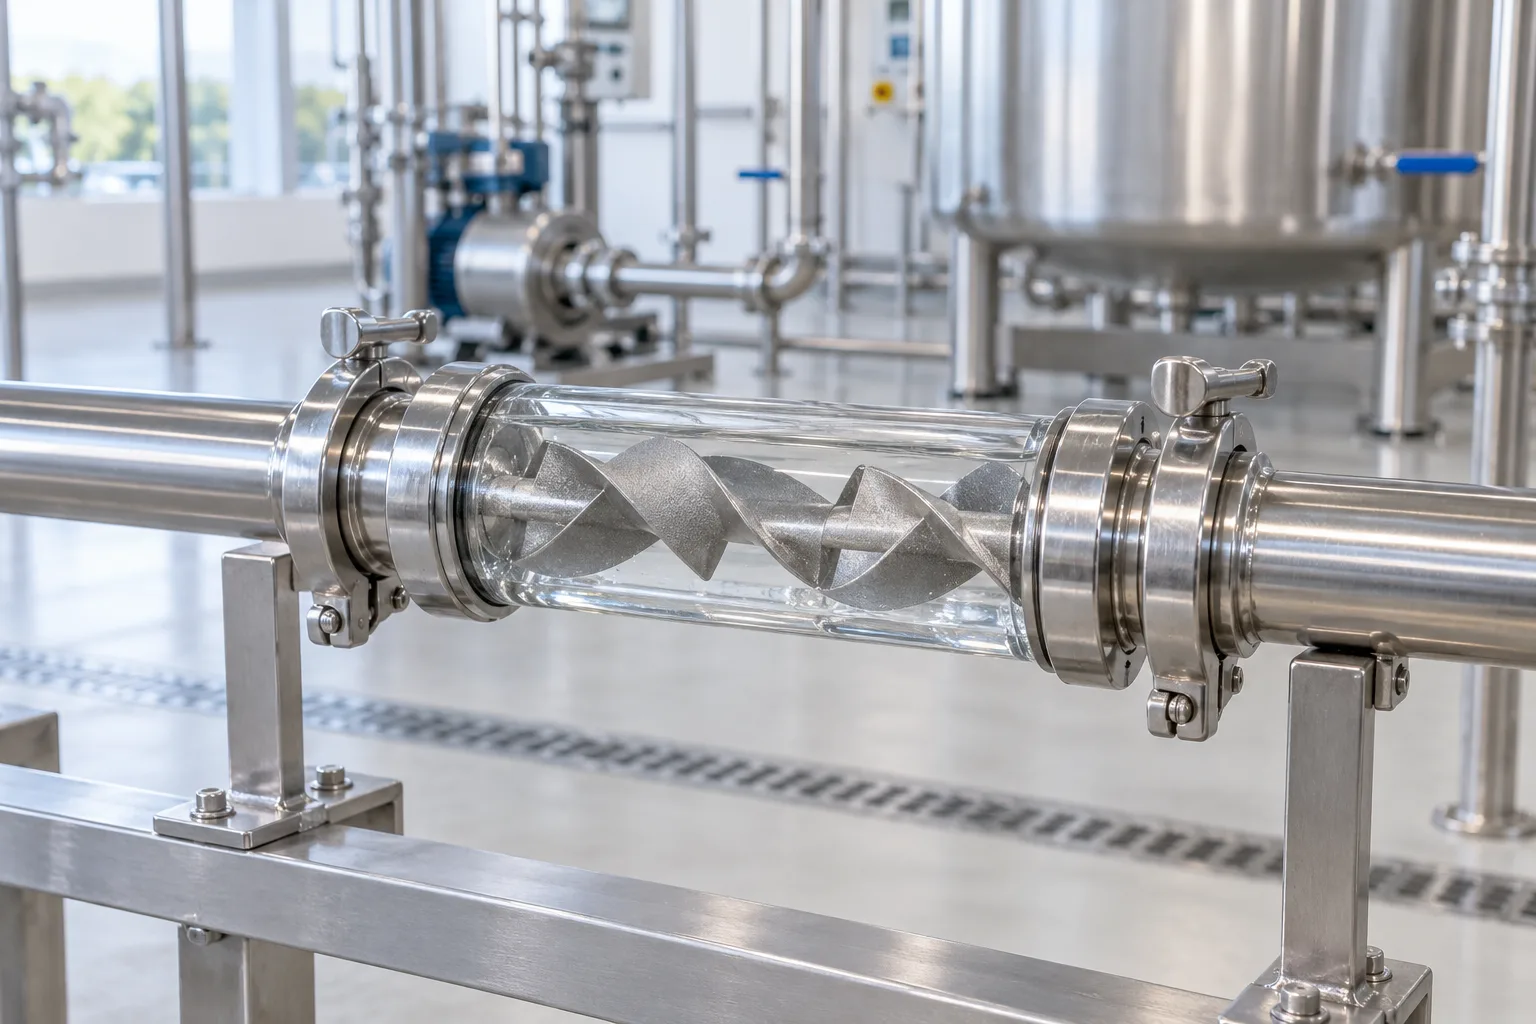
3D printed stainless static mixer with tri-clamp ends in a clear section of a process line

Flow, mixing and fittings

Water & Process Equipment

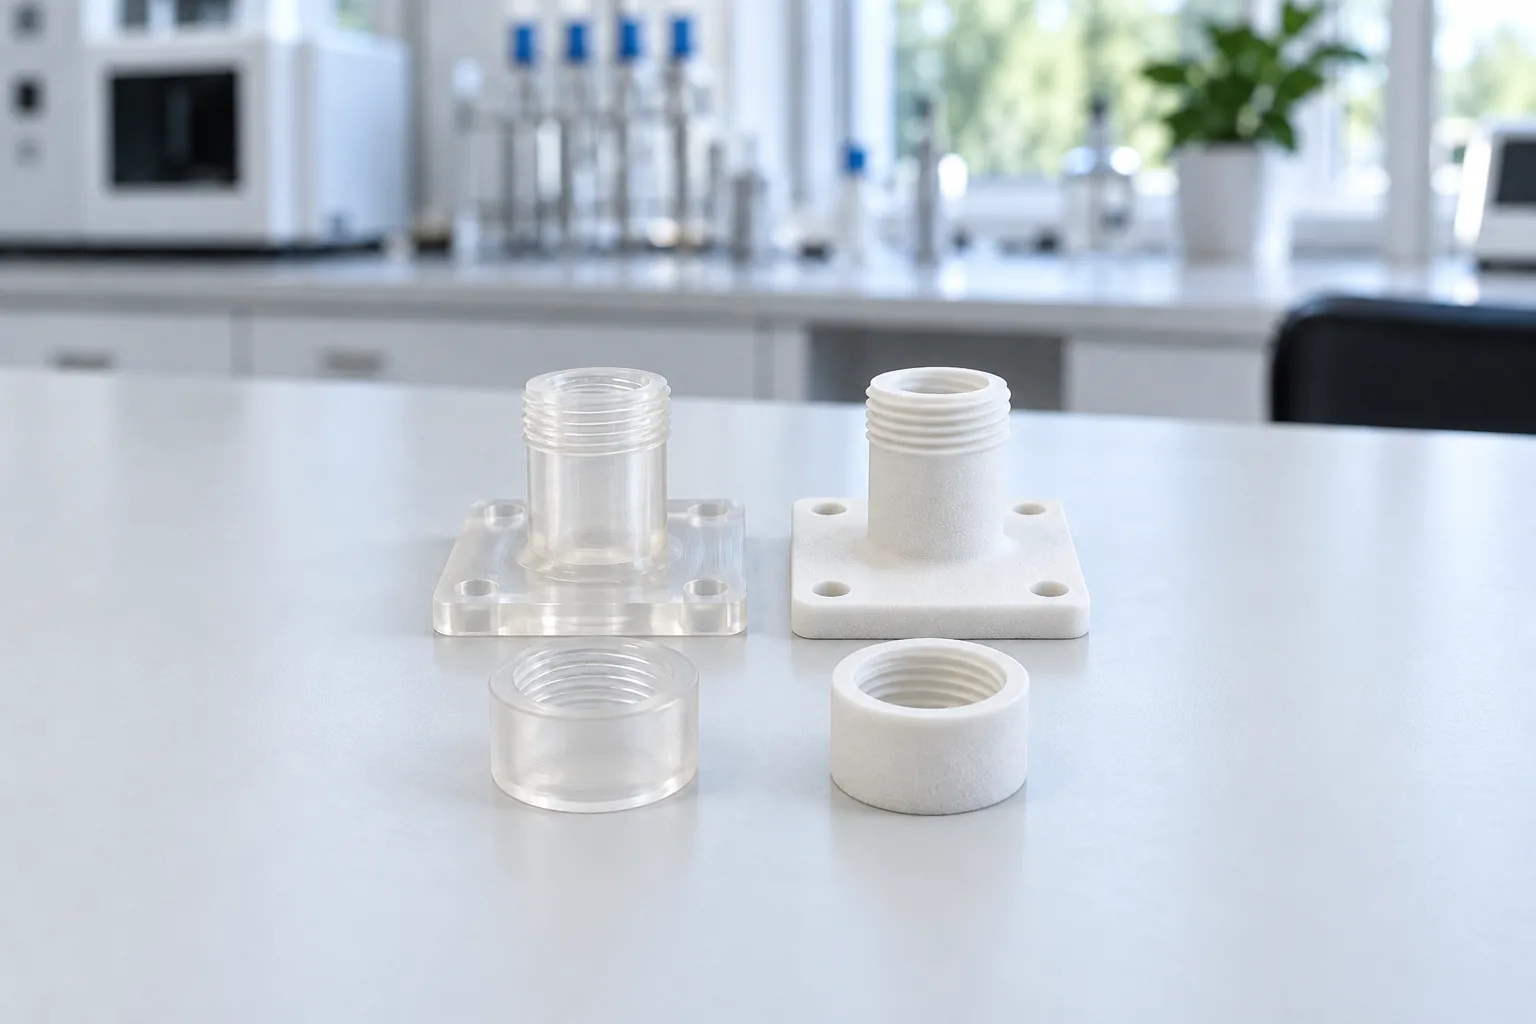
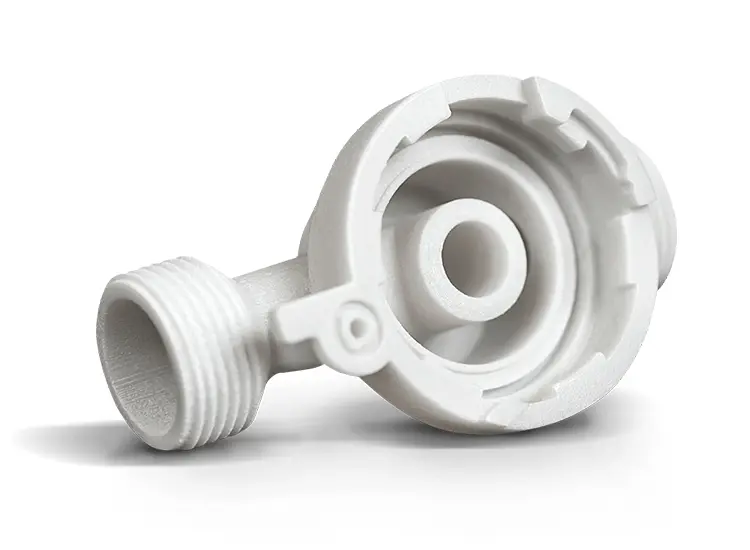
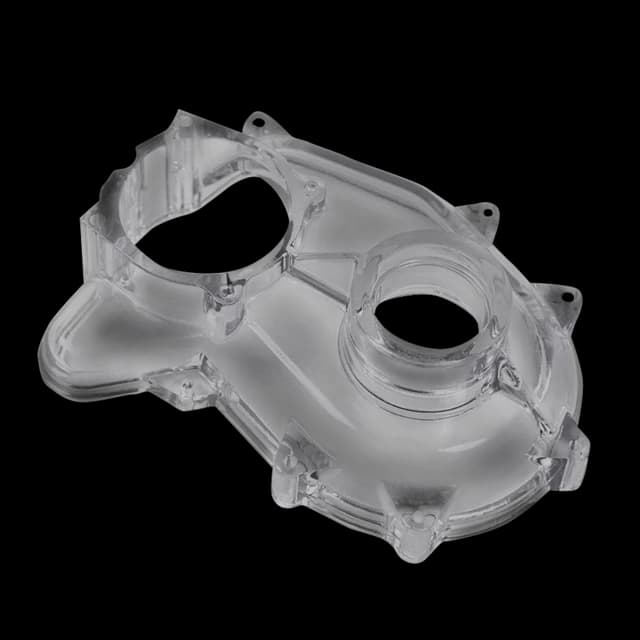
DMLS 316L stainless steel produces helical static-mixer vanes up to 380 mm long with sanitary tri-clamp ends, and tees with NPT threads and hose barbs in 316L or titanium. The internal geometry that makes a mixer work would need several machined and welded pieces; printed, it is one part. Clear Accura ClearVue SLA makes flanged transition fittings and threaded collars for development rounds, where you can see into the assembly; a revised design can move to SLS PA12.

Typical parts
Static-mixer vanes, threaded tees, barbed fittings, clear flanged fittings
Key properties
Parts up to 380 mm long in one piece; NPT threads
Material data
316L stainless and Ti6Al4V for corrosion resistance; Accura ClearVue: 87.2% luminous transmittance
Black ASA mounting plate fitted to an outdoor electrical cabinet

Grid, solar and field installations

Grid & Field Hardware in Repeat Lots

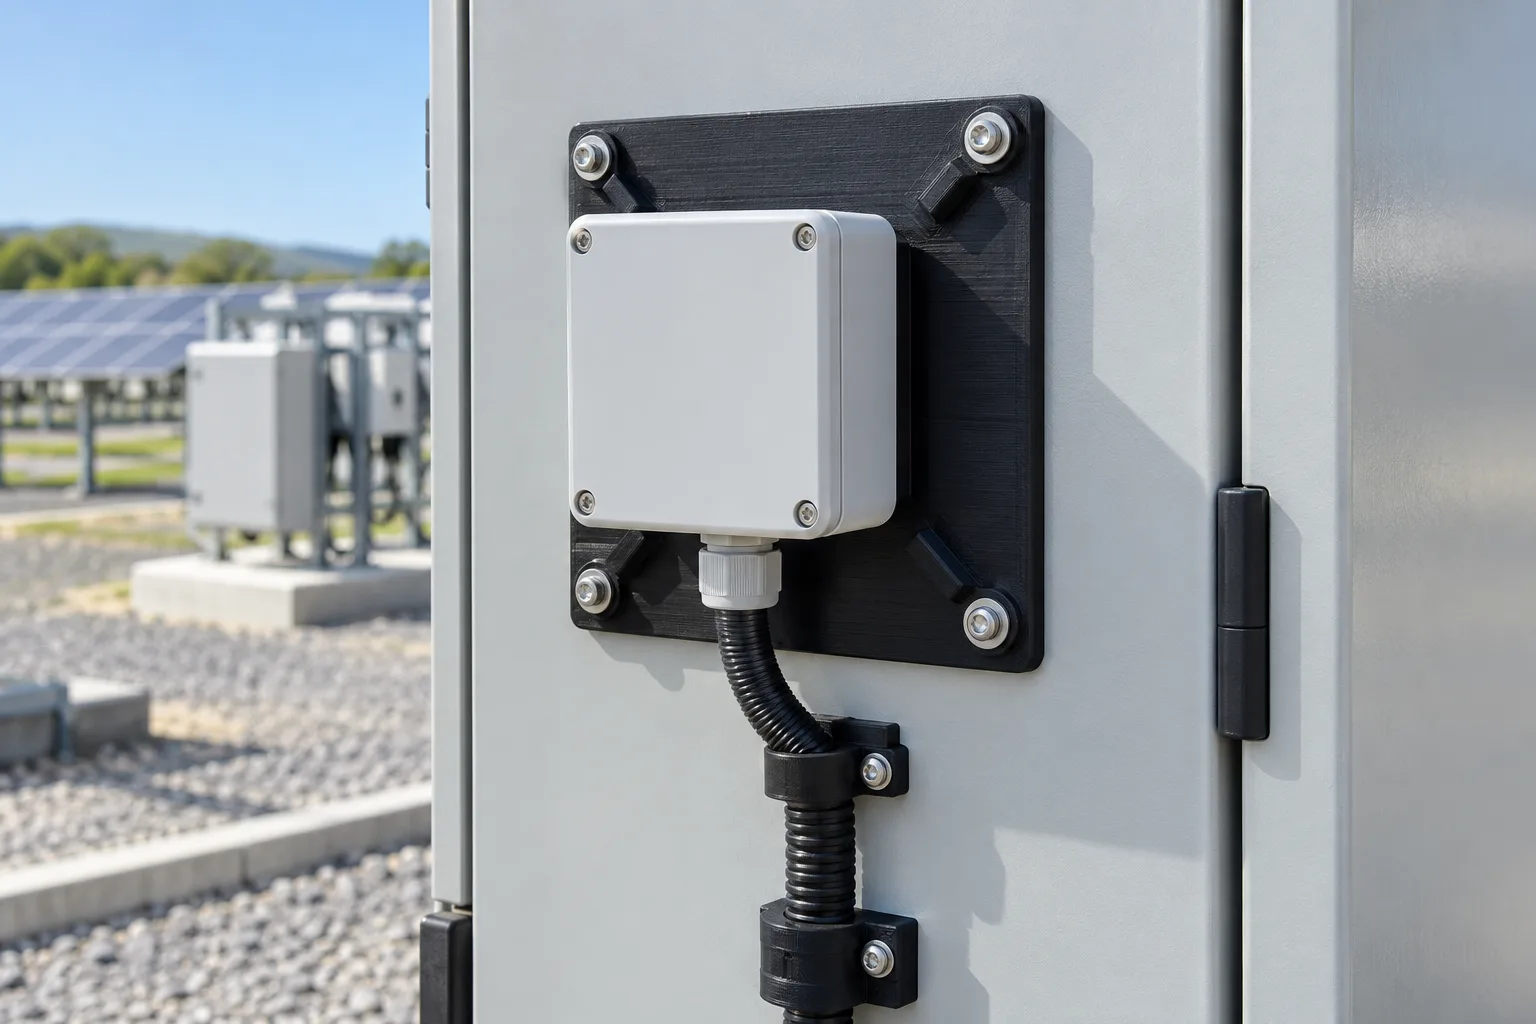
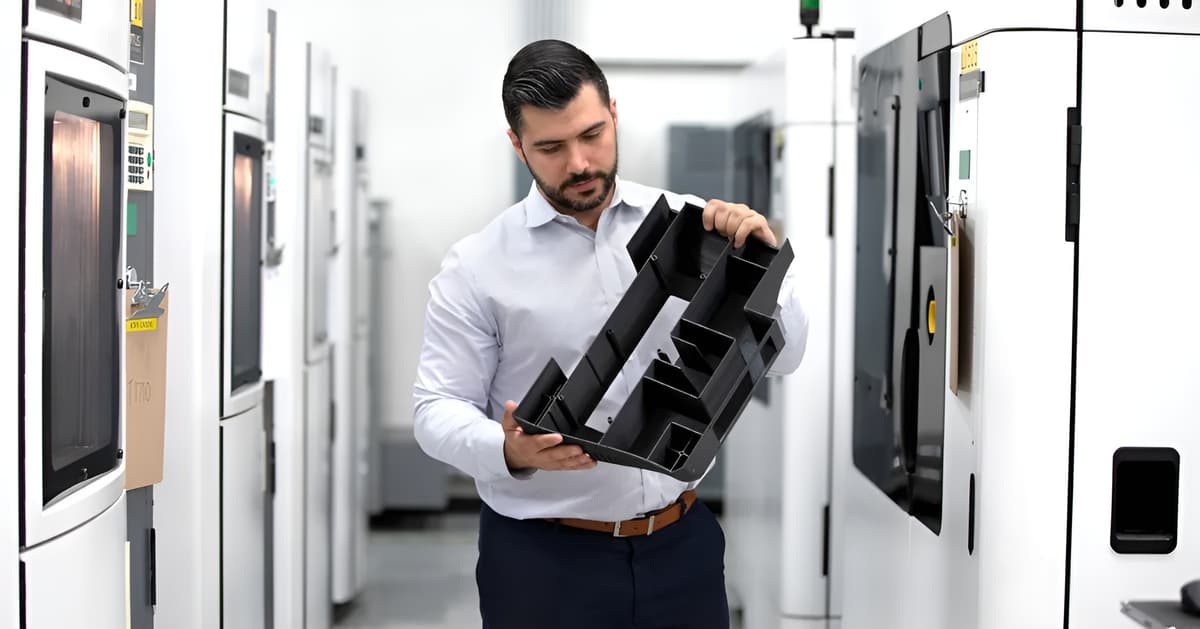
UV-stable ASA makes mounting plates, brackets and covers for outdoor power equipment. Repeat lots print from a saved file: one ASA plate for a power equipment maker ran to more than 600 pieces from one unchanged file and print settings, released in three batches with no mould. Line fixtures, assembly aids and field spares follow the same route, so parts stay available without holding stock.

Typical parts
Mounting plates, brackets, covers, line fixtures, field spares
Key properties
FDM builds to 914 × 610 × 914 mm; repeat lots from saved files
Material data
ASA: 98 °C HDT at 264 psi, UV and weather resistant
Case Studies

Clean Tech Manufacturing Outcomes

Production and development work for fuel cell, clean tech equipment and power generation companies.

Touch-Proof High-Voltage Covers in MJF PA12: Build Direction and GD&T

Case study

Touch-Proof High-Voltage Covers in MJF PA12: Build Direction and GD&T

These MJF PA12 electrical covers came with drawing requirements for build direction, GD&T, marking, packaging and a REACH declaration. We translated those requirements into an order with first article inspection and per-part dimensional checks.

Key outcomes

  • One support delivered ahead of the production lot
  • Geometry unchanged from first quote to order
  • Drawing attached to every production order line
  • First article and per-part checks on the order
Read the high-voltage cover case study
Flange Fittings With 3D Printed Threads: Clear SLA, Then SLS PA12

Case study

Flange Fittings With 3D Printed Threads: Clear SLA, Then SLS PA12

These flanged fittings and collars used threads printed directly from the model. Clear SLA resin supported the first development rounds; a revised fitting moved to SLS PA12. No tapping or threaded inserts were ordered.

Key outcomes

  • Clear SLA and SLS PA12 versions without tooling
  • Each fitting order shipped in 3 to 4 business days
  • Internal and external threads printed from the model
  • Every order shipped complete, on or before target
Read the threaded fittings case study
Engine Pistons and Valve Parts in DMLS: Print, Then Machine

Case study

Engine Pistons and Valve Parts in DMLS: Print, Then Machine

These engine parts started with machining drawings. DMLS produced the shapes in aluminium and stainless steel; groove machining, thread cutting and a wire-EDM slit were specified as post-print operations. Every piston was measured against the agreed tolerance band.

Key outcomes

  • AlSi10Mg and 316L in place of drawn 2618 and steel
  • Ring grooves and threads finished after printing
  • Every piston inside the agreed ±0.002 in band
  • Seal protectors shipped 5 business days early
Read the DMLS engine parts case study
Material Library

Materials for Energy and Clean Tech

Nylons, flame-rated and UV-stable thermoplastics, elastomers, clear resin and metals chosen for heat, flame, UV, static and chemical exposure. Compare full properties on each material page.

Explore the complete material matrix. Compare certifications, mechanical properties and application fit across the full portfolio before locking your production material stack.

Start a quote

Ready to Manufacture Your Energy Hardware?

Upload your CAD files for an instant quote or speak with our application engineers about your specific requirements.

  • Instant pricing with automated manufacturability analysis
  • Production workflows built for repeatable quality
  • Engineering support from prototype to production
Talk to an engineer

Create an account to upload CAD

STEP, STL, OBJ, 3MF and IGES supported

Manufacturing technologies
6
Engineering materials
50+
Part quantities
1-500+