Direct Metal Laser Sintering (DMLS) Volume Production of High Performance End-Use Parts

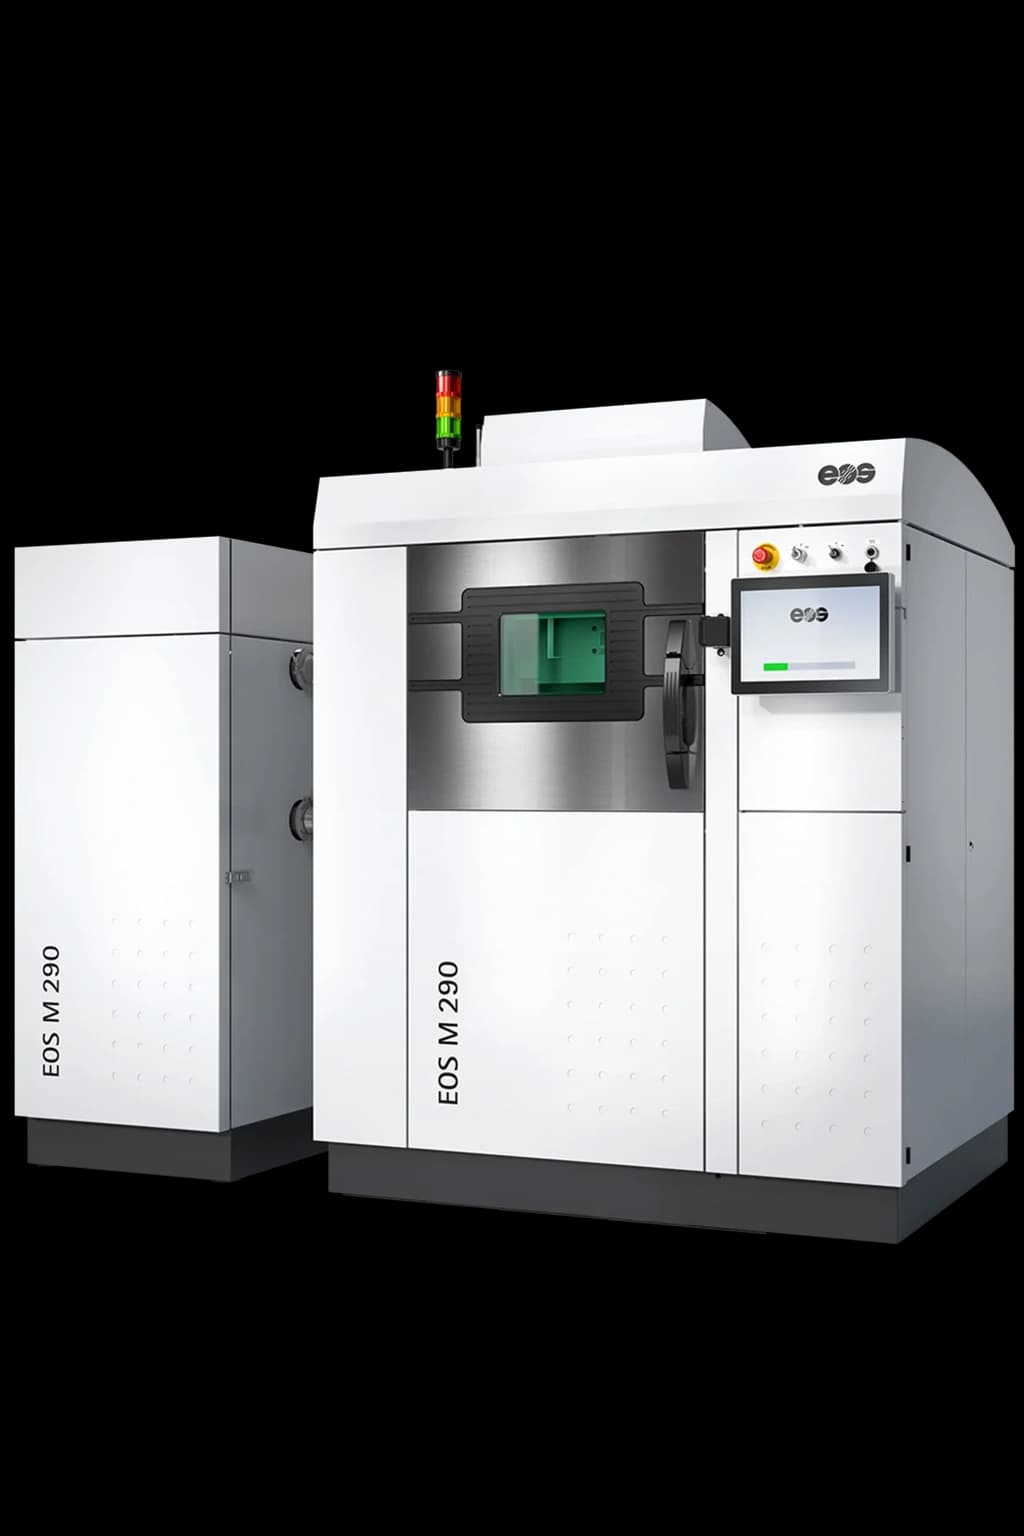
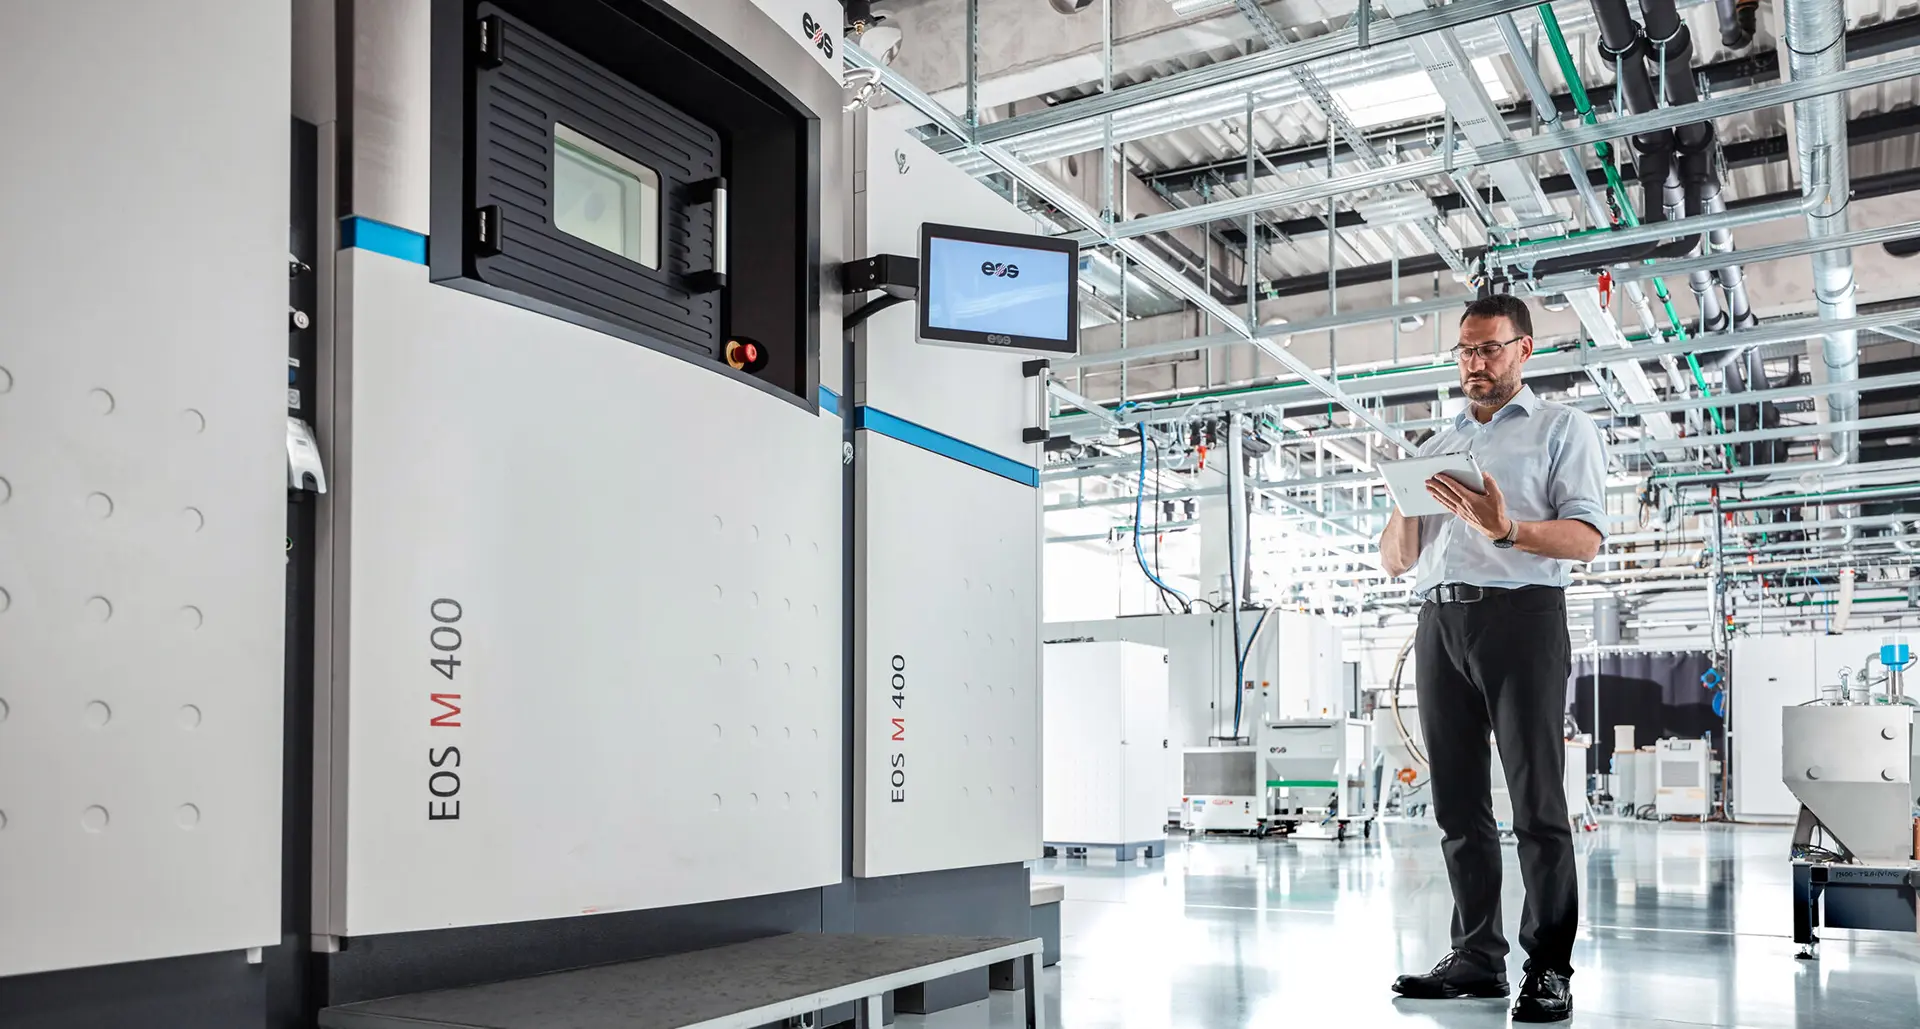
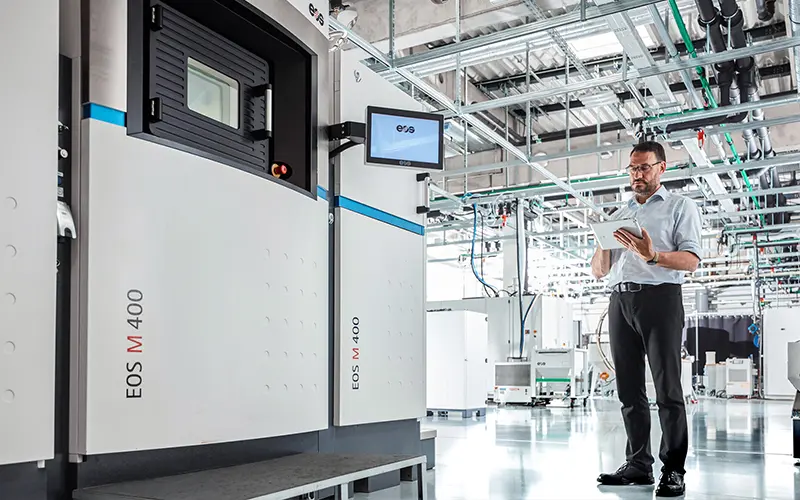
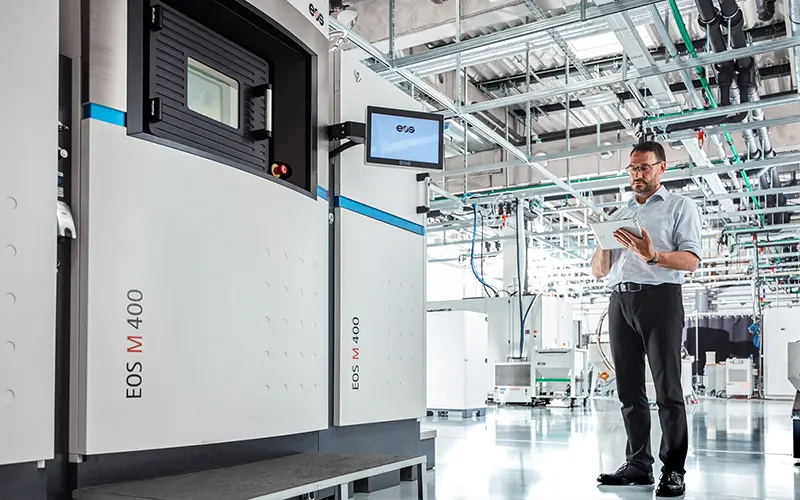
DMLS 3D Printer
Technology Overview

Functional Metal Components

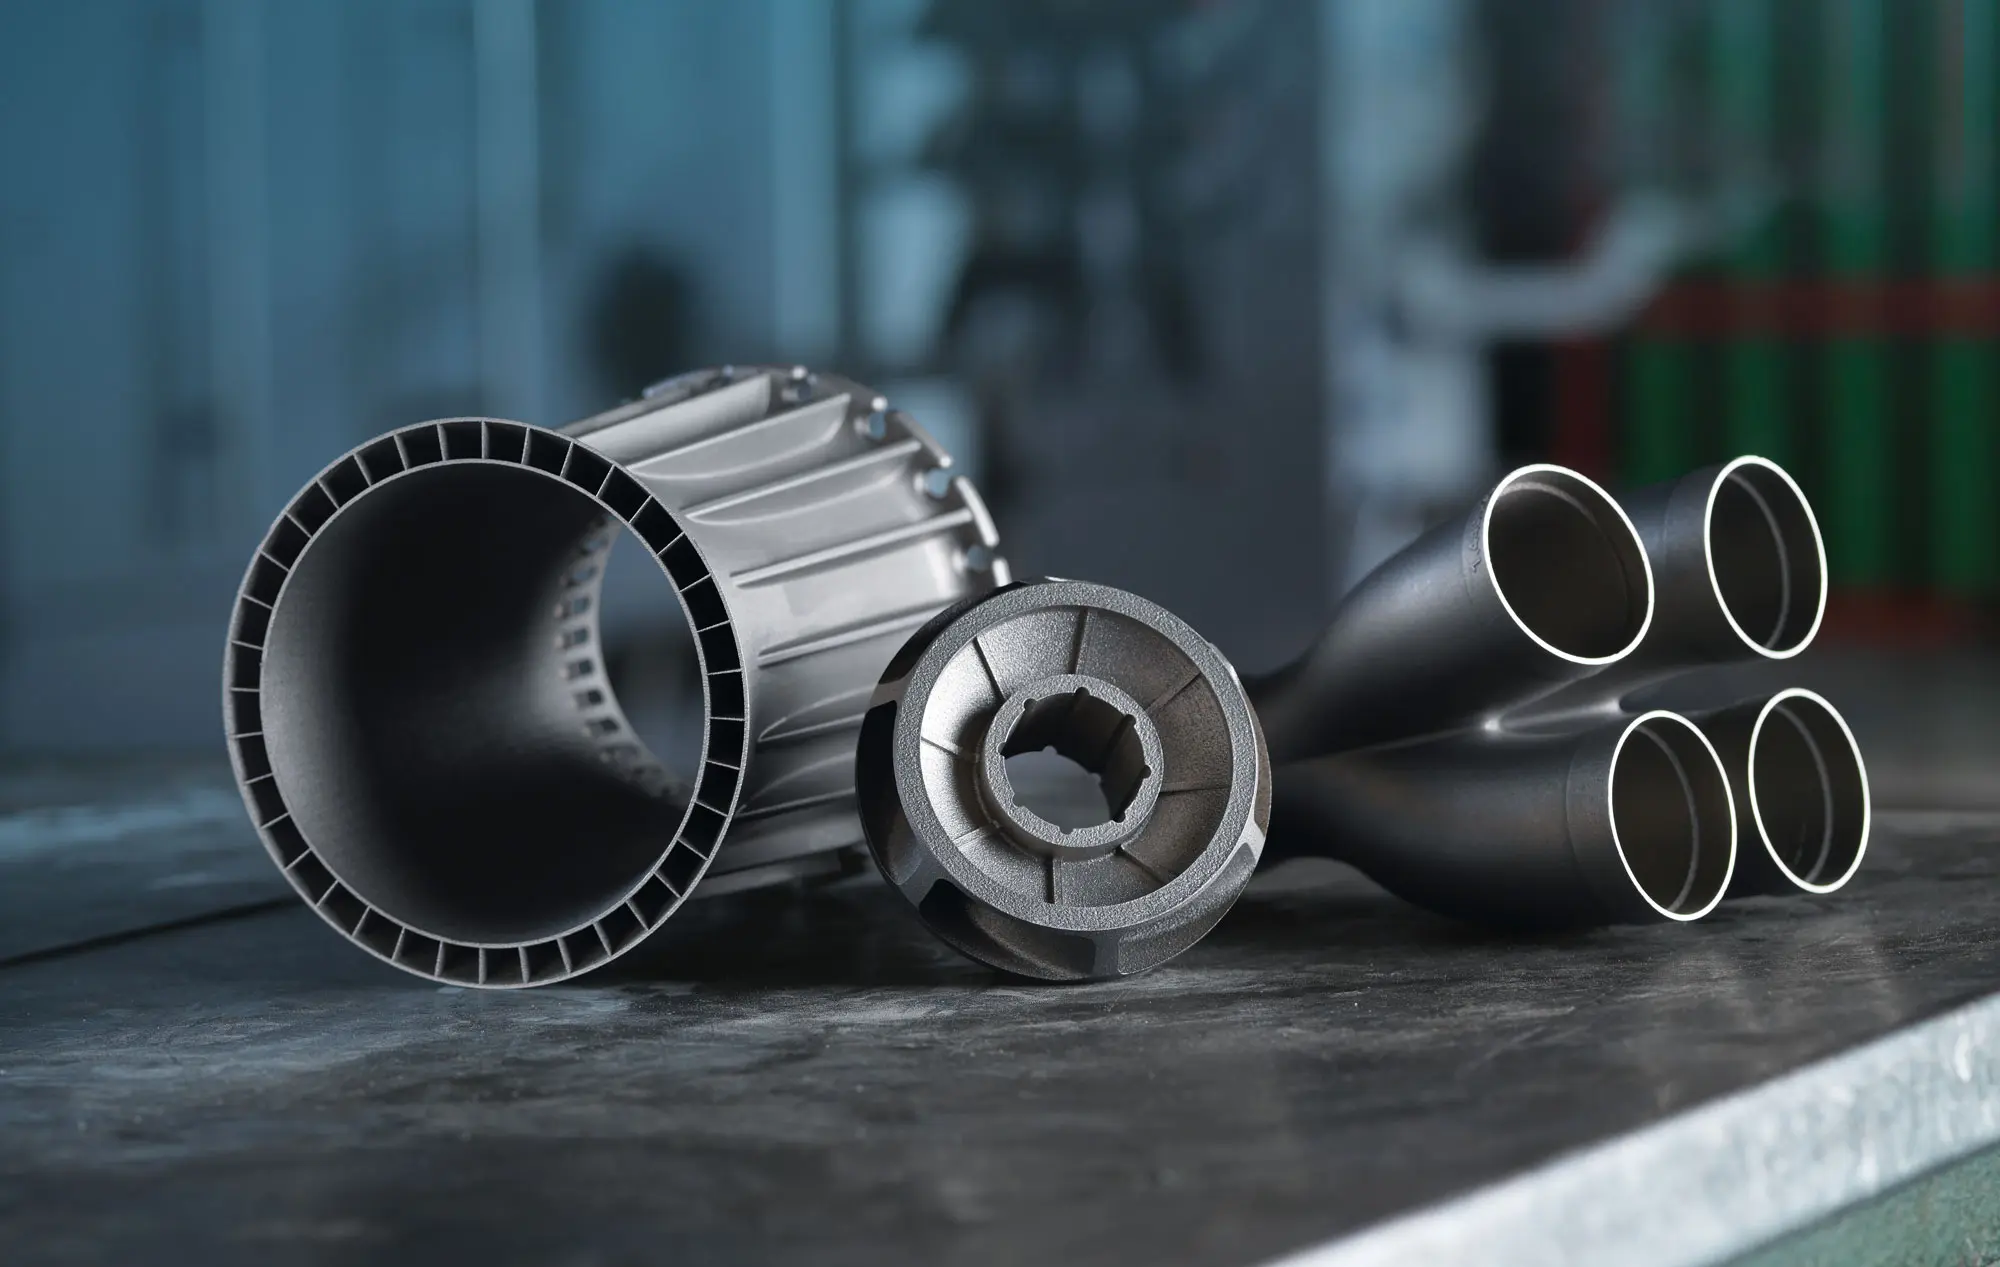
DMLS produces metal parts with mechanical properties matching traditional manufacturing. A high-powered laser selectively fuses layers of metal powder into functional components with exceptional strength and durability. Complex internal geometries and part consolidation enable revolutionary design possibilities in aerospace, energy, automotive and motorsport applications.

Why manufacture with DMLS

Advanced manufacturing capabilities enable complex geometries, functional prototypes, and end-use production parts that would be impossible or cost-prohibitive with traditional manufacturing methods. From functional prototypes to end-use production parts, this technology delivers exceptional performance across demanding industries.

Build volume
400 x 300 x 400 mm
Tolerance
±0.3% (min ±0.3 mm)
Layer height
0.02 - 0.06 mm

Metal Precision · Industrial Grade

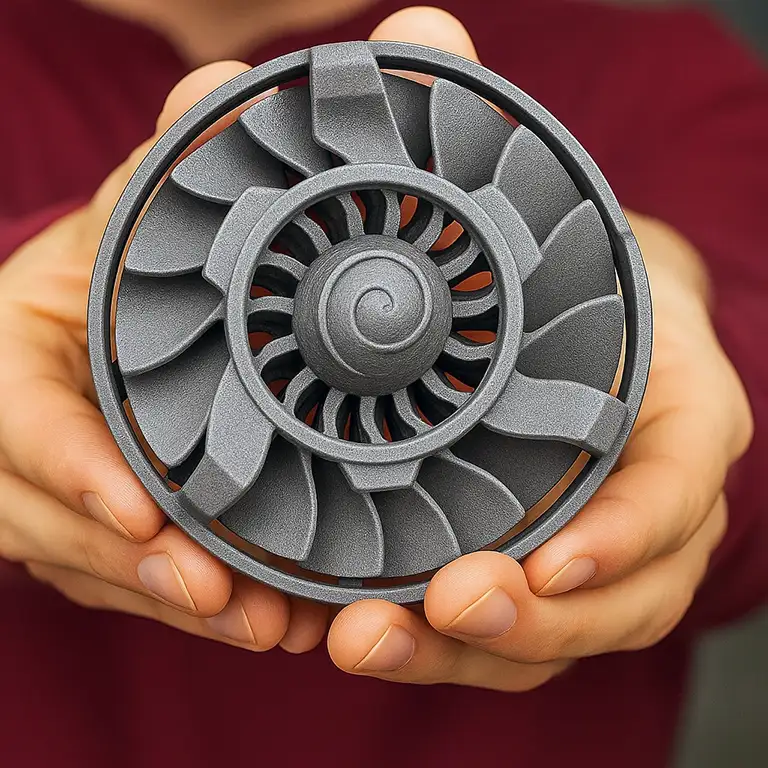
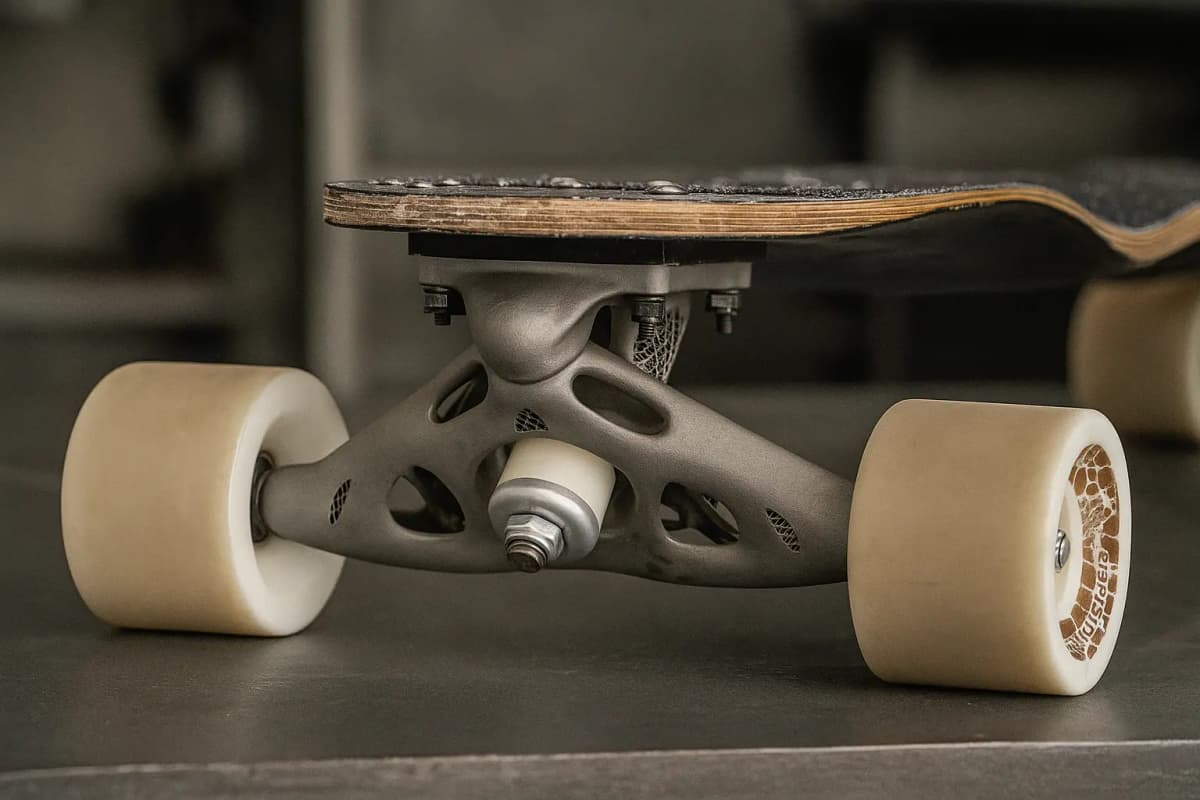
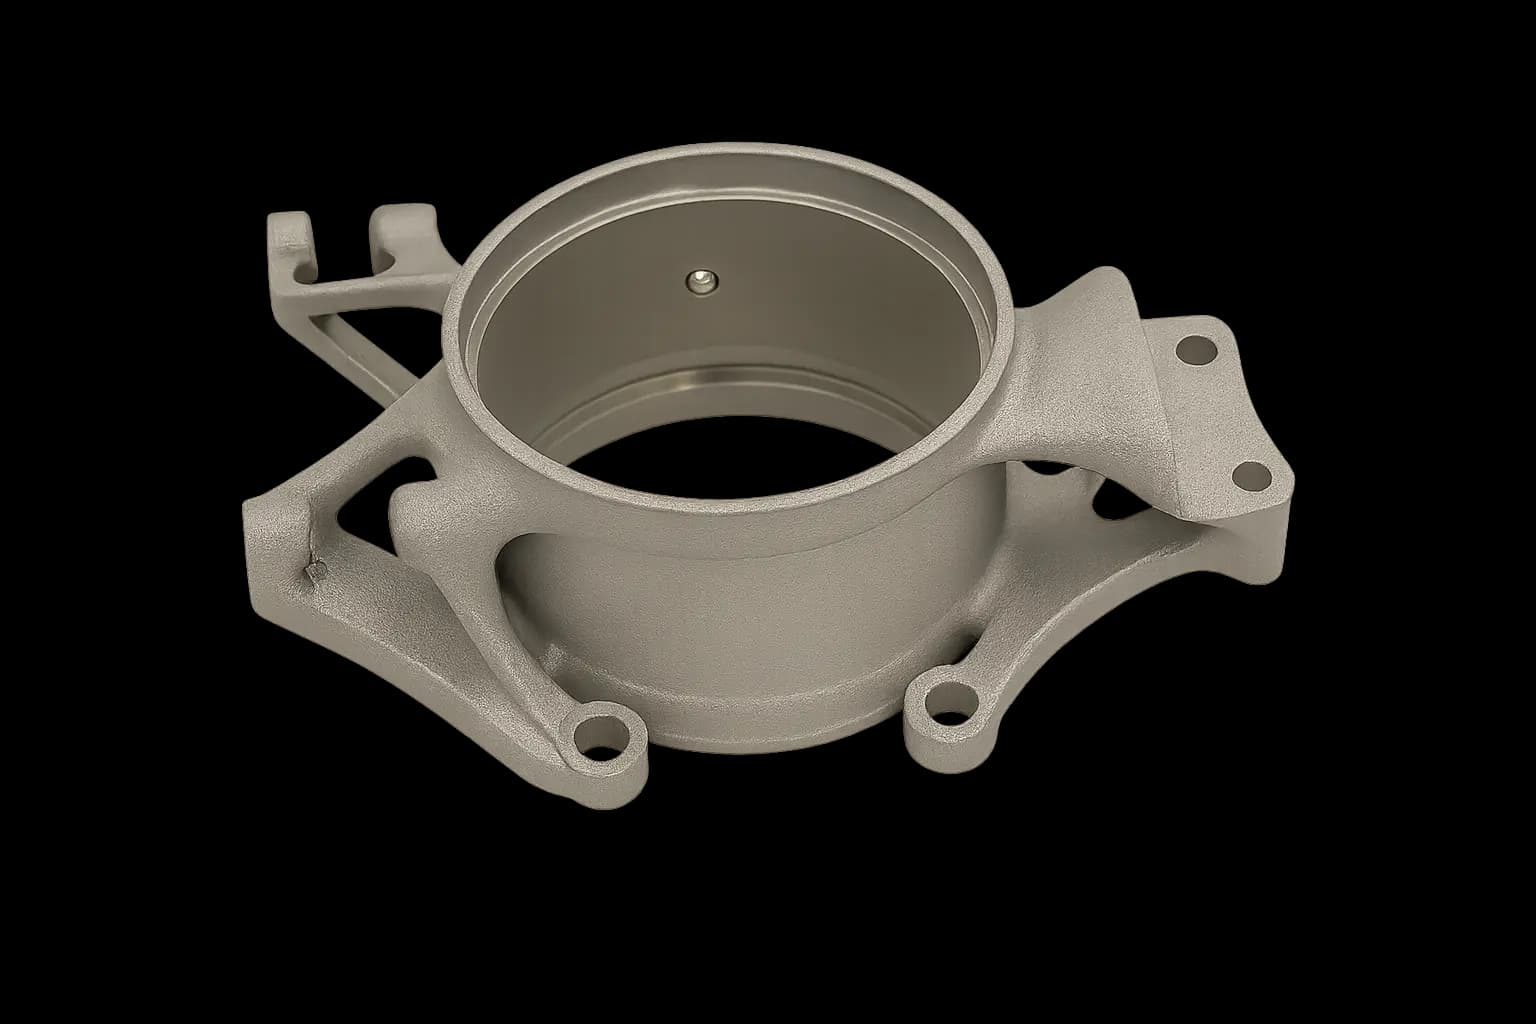
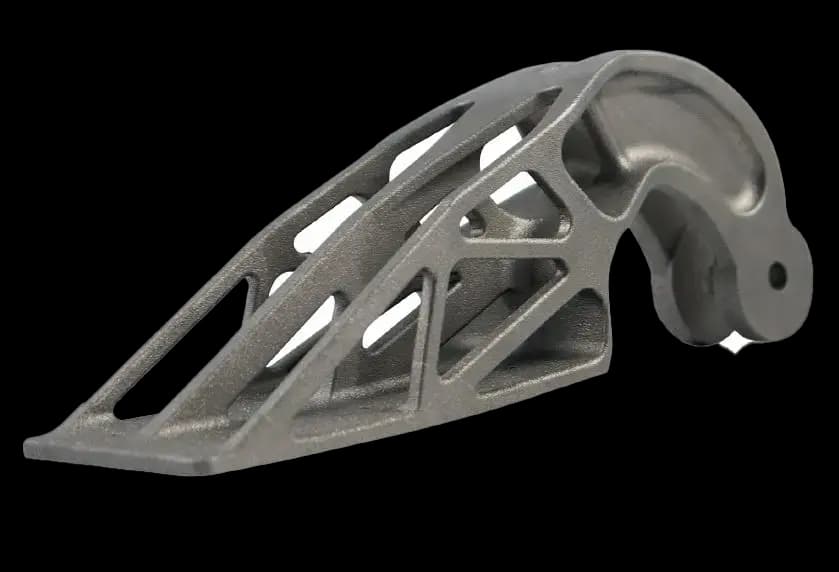
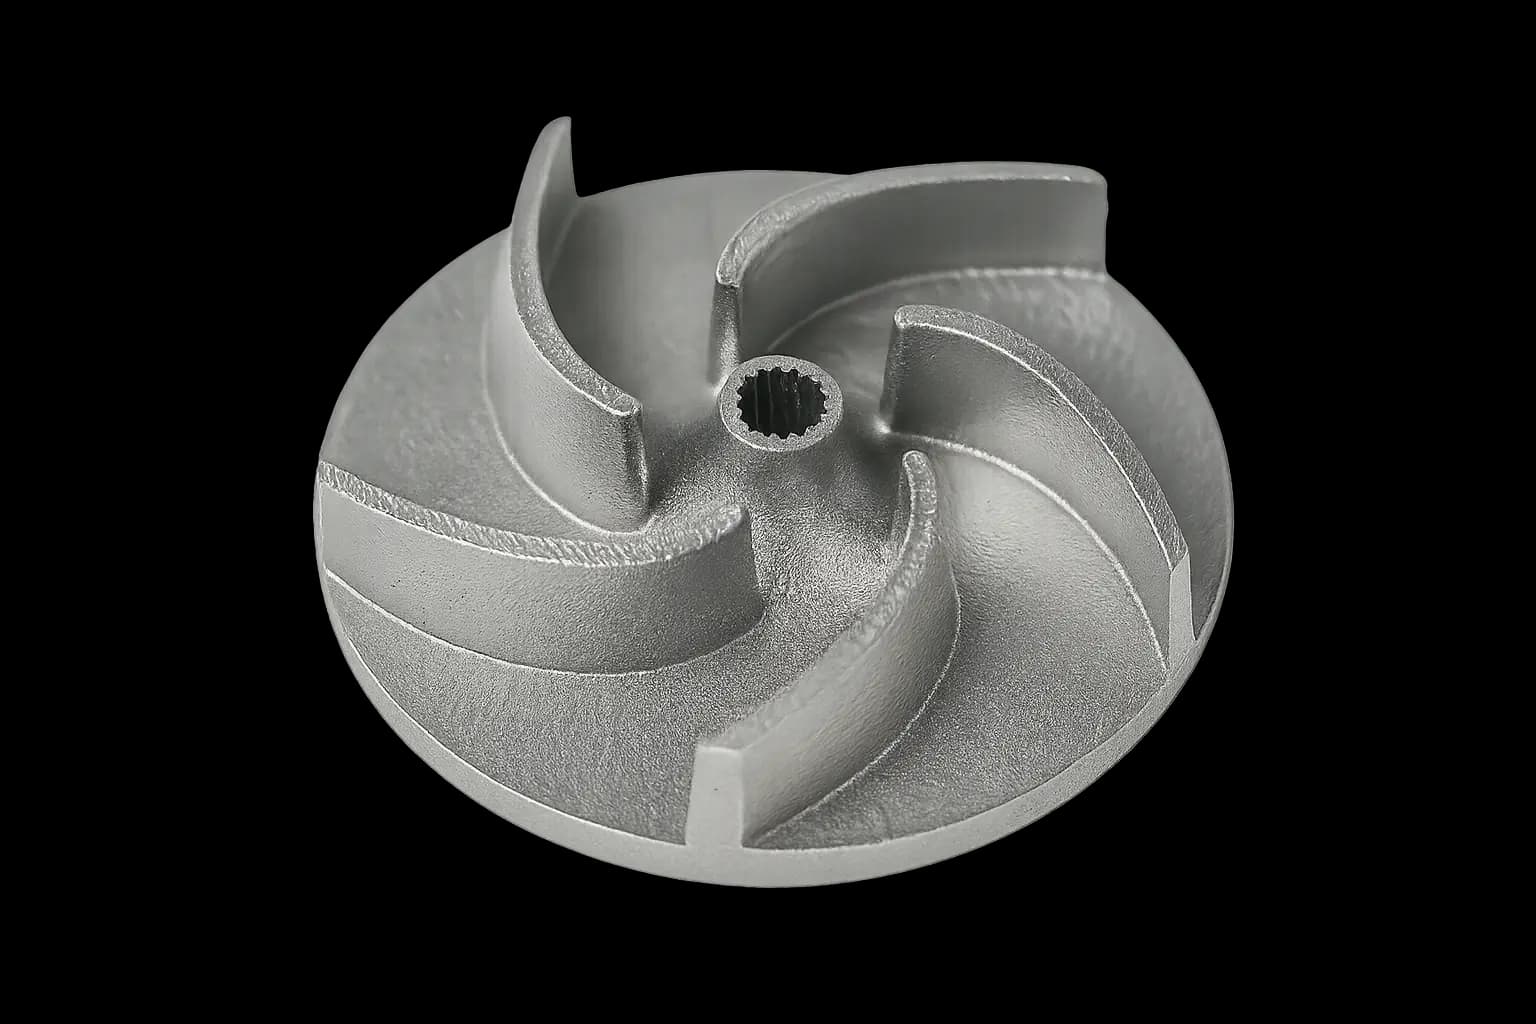
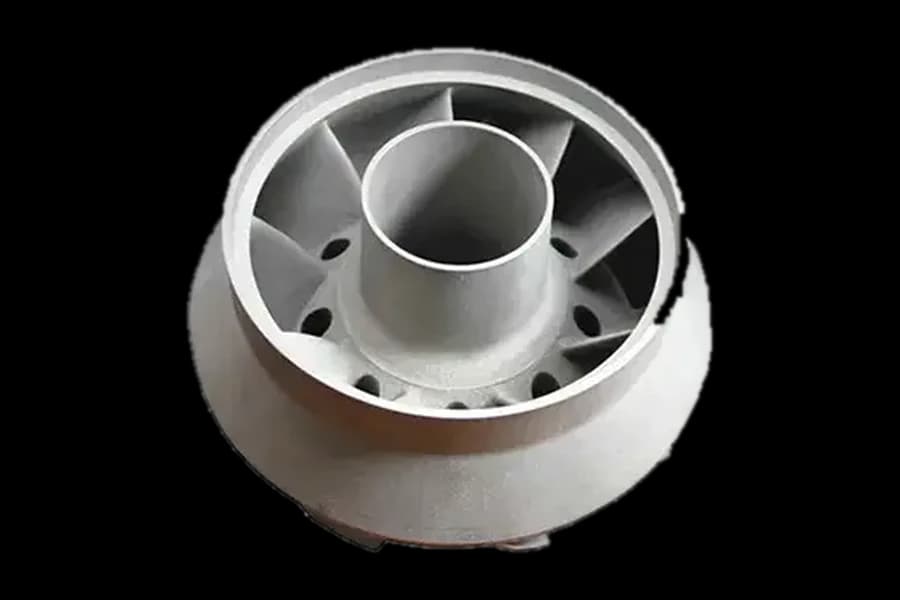
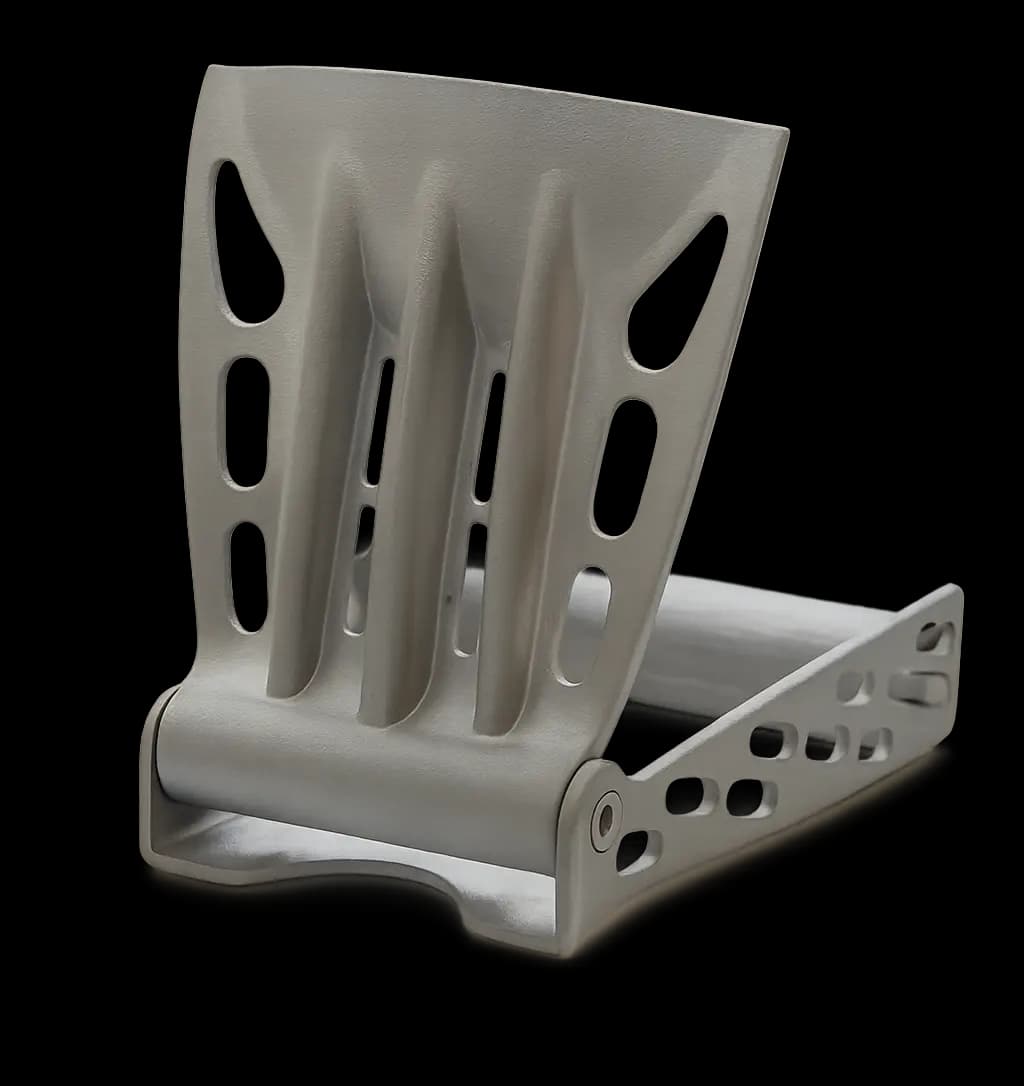
Direct Metal Laser Sintering technology example showing DMLS 3D printing capabilities and quality

Aerospace Manufacturing

Aerospace-Grade Metal Components

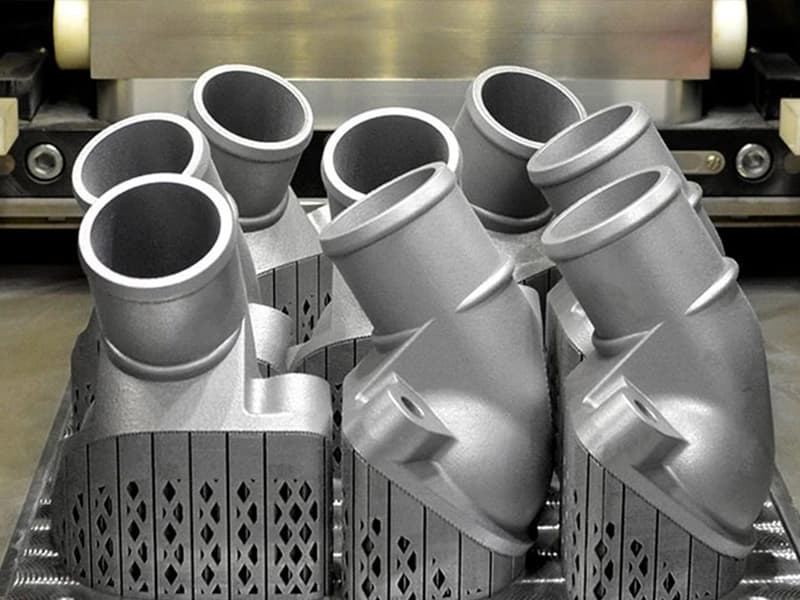
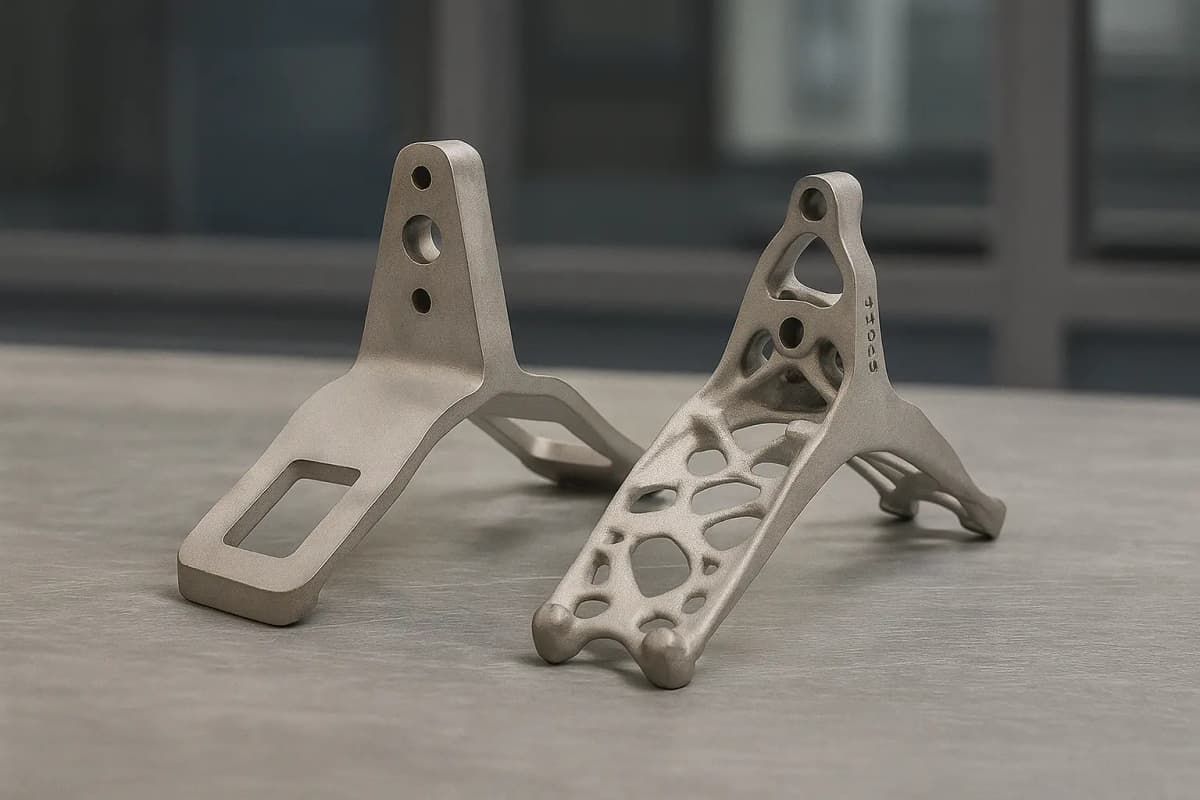
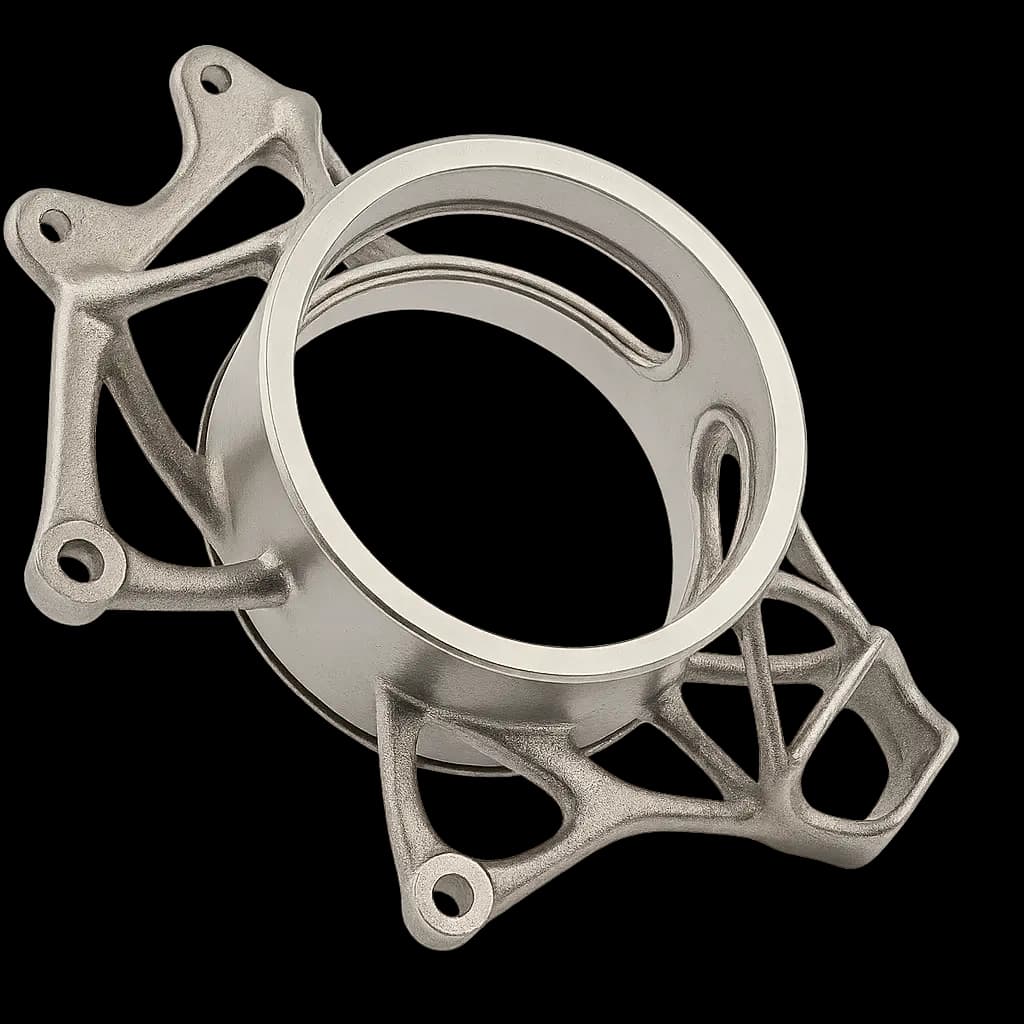
Critical for aerospace and other high-performance applications where failure is not an option, DMLS produces functional metal parts with properties matching or exceeding traditional manufacturing. From titanium aerospace brackets to lightweight heatsinks, this technology enables complex internal geometries and lightweighting strategies impossible with conventional machining.

Production applications

Mission-Critical Components

Aerospace and other high performance applications require documented material properties and full traceability, which DMLS can deliver through certified material batches and detailed build reports. The high-energy laser creates metallurgical bonds equivalent to wrought metals, enabling stress-bearing components that undergo rigorous testing including fatigue, tensile, and impact analysis. Support structures are strategically designed to minimize material waste while ensuring optimal heat dissipation during the build process.

Key advantages

Complex geometries: Intricate internal channels, overhangs, and assemblies impossible with traditional manufacturing.

Functional prototypes: Test mechanical properties and fit before investing in production tooling.

Custom tooling: Jigs, fixtures, and manufacturing aids tailored to specific production requirements.

End-use parts: Production components for aerospace, medical, automotive, and industrial applications.

DMLS automotive components
DMLS medical devices
DMLS aerospace components
DMLS complex geometries
Manufacturing Process

The Direct Metal Laser Sintering (DMLS) manufacturing process

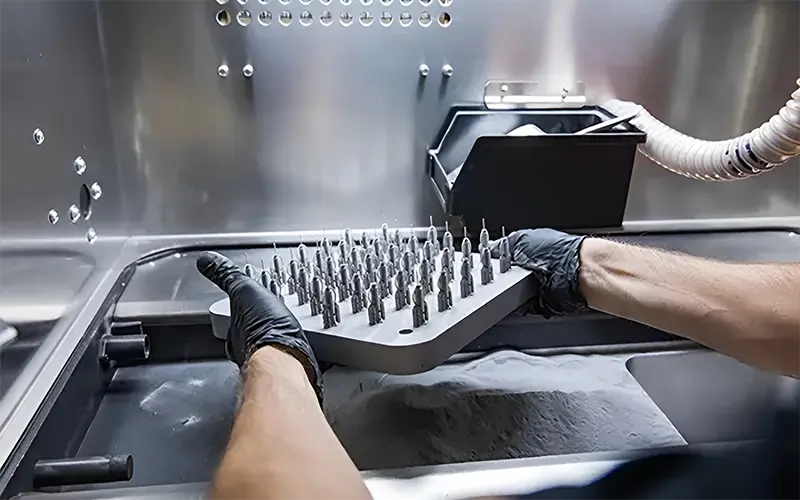
DMLS uses a high-powered fiber laser to selectively fuse metal powder particles layer by layer in an inert atmosphere, creating dense metal components with mechanical properties comparable to traditionally manufactured parts. Builds undergo stress relief and support removal to stabilize geometry before final finishing. Critical surfaces can be machined or polished to meet tight tolerance requirements.

Powder Preparation

Step 1 of 4

Powder Preparation

Fine metal powder is prepared and loaded into the machine. The build platform is preheated to optimal temperature to reduce thermal stress and improve part quality.

Powder Size
15-45 microns
Preheat Temp
80-200°C
Atmosphere
Inert (Argon)
Build Volume

Metal powder bed systems allow dense part nesting while maintaining thermal stability during the build up to 400 x 300 x 400 mm.

Tolerance

Near-net-shape accuracy with machining applied to critical tolerance surfaces to ±0.3% (min ±0.3 mm).

Layer Height

Fine layers for dense metal micro-features and thin walls using 0.02 - 0.06 mm.

Machines

Forge Labs manufactures DMLS parts using EOS M290.

Material Library

Aerospace Grade Metal Alloys

Aerospace-grade metal powders including stainless steel, aluminum, and titanium alloys. Each material meets stringent industry standards for mechanical properties, offering exceptional strength-to-weight ratios and corrosion resistance for critical applications.

  • Aluminum AlSi10Mg Part
    Metal

    Aluminum AlSi10Mg

    Aluminum AlSi10Mg is a casting alloy specifically optimized for Direct Metal Laser Sintering (DMLS) additive manufacturing.

    Tensile Strength
    461 / 466 MPa
    Elastic Modulus
    75 / 70 GPa
    Temp Resistance
    See datasheet
    Material details

    This versatile material combines the lightweight properties of aluminum with silicon and magnesium additions that enhance strength, hardness, and castability.

    Lightweight High-Performance Metal Alloy

    Compliance

    DIN EN 1706 (EN AC-43000)/ASTM F3318-18

    Applications

    Aerospace Components/Automotive Systems/Heat Management/Industrial Equipment

  • Aluminum 6061 Part
    Metal

    Aluminum 6061

    Aluminum 6061 is a versatile precipitation-hardened alloy that combines magnesium and silicon as primary alloying elements to achieve exceptional mechanical properties.

    Tensile Strength
    331 MPa
    Elastic Modulus
    76 GPa
    Temp Resistance
    See datasheet
    Material details

    This heat-treatable alloy offers an outstanding balance of strength, ductility, and corrosion resistance, making it ideal for structural applications where high performance and reliability are essential.

    High-Strength Structural Aluminum Alloy

    Applications

    Aerospace Structures/Automotive Components/Marine Hardware/Precision Fixtures

  • Stainless Steel 316L Part
    Metal

    Stainless Steel 316L

    Stainless Steel 316L is the most popular 3D printed metal at Forge Labs for corrosion-resistant 3D printed parts.

    Tensile Strength
    630 MPa
    Elastic Modulus
    185 GPa
    Temp Resistance
    See datasheet
    Material details

    It combines high strength, excellent ductility, and strong chloride resistance, making it a go-to material for marine hardware, chemical processing equipment, food production components, and precision industrial assemblies.

    Marine-Grade Austenitic Stainless Steel

    Compliance

    ASTM F138 (UNS S31673) chemistry/REACH Regulation (EC) 1907/2006

    Applications

    Industrial Components/Chemical Processing/Food Processing/Marine Applications

  • Stainless Steel 17-4 PH Part
    Metal

    Stainless Steel 17-4 PH

    Stainless Steel 17-4 PH is a precipitation hardening martensitic stainless steel that offers an exceptional combination of high strength, good corrosion resistance, and excellent mechanical properties.

    Tensile Strength
    1335 / 1340 MPa
    Elastic Modulus
    196 GPa
    Temp Resistance
    316 °C
    Material details

    After heat treatment (H900 condition), it achieves tensile strengths exceeding 1340 MPa while maintaining good ductility.

    Precipitation Hardening Stainless Steel

    Compliance

    ASTM A564/A564M-13 (Type 630, UNS S17400)/ASTM F899-12b/ISO 10993-5 (Cytotoxicity)

    Applications
    Precision Tools/Aerospace Components/Automotive Parts/Marine Hardware

  • Maraging Steel MS1 Part
    Metal

    Maraging Steel MS1

    Maraging Steel MS1 is a ultra-high strength steel with exceptional hardness and dimensional stability achieved through precipitation hardening.

    Tensile Strength
    1200 / 1100 MPa
    Elastic Modulus
    150 / 140 GPa
    Temp Resistance
    400 °C
    Material details

    With its 18% nickel content and low carbon composition, it delivers superior mechanical properties ideal for precision tooling applications.

    Ultra-High Strength Steel for Precision Tooling

    Applications
    Injection Molding Tools/Mechanical Engineering/Precision Tooling/Aerospace Tooling

  • Titanium Ti-6Al-4V Part
    Metal

    Titanium Ti-6Al-4V

    Titanium Ti-6Al-4V (Grade 5) is the most widely used titanium alloy in aerospace and automotive applications.

    Tensile Strength
    1080 MPa
    Elastic Modulus
    110 GPa
    Temp Resistance
    350 °C
    Material details

    This alpha-beta alloy offers an exceptional strength-to-weight ratio and excellent corrosion resistance.

    Aerospace-Grade Lightweight Alloy

    Compliance

    ASTM B348 Grade 5/ASTM F2924/ASTM F3302

    Applications
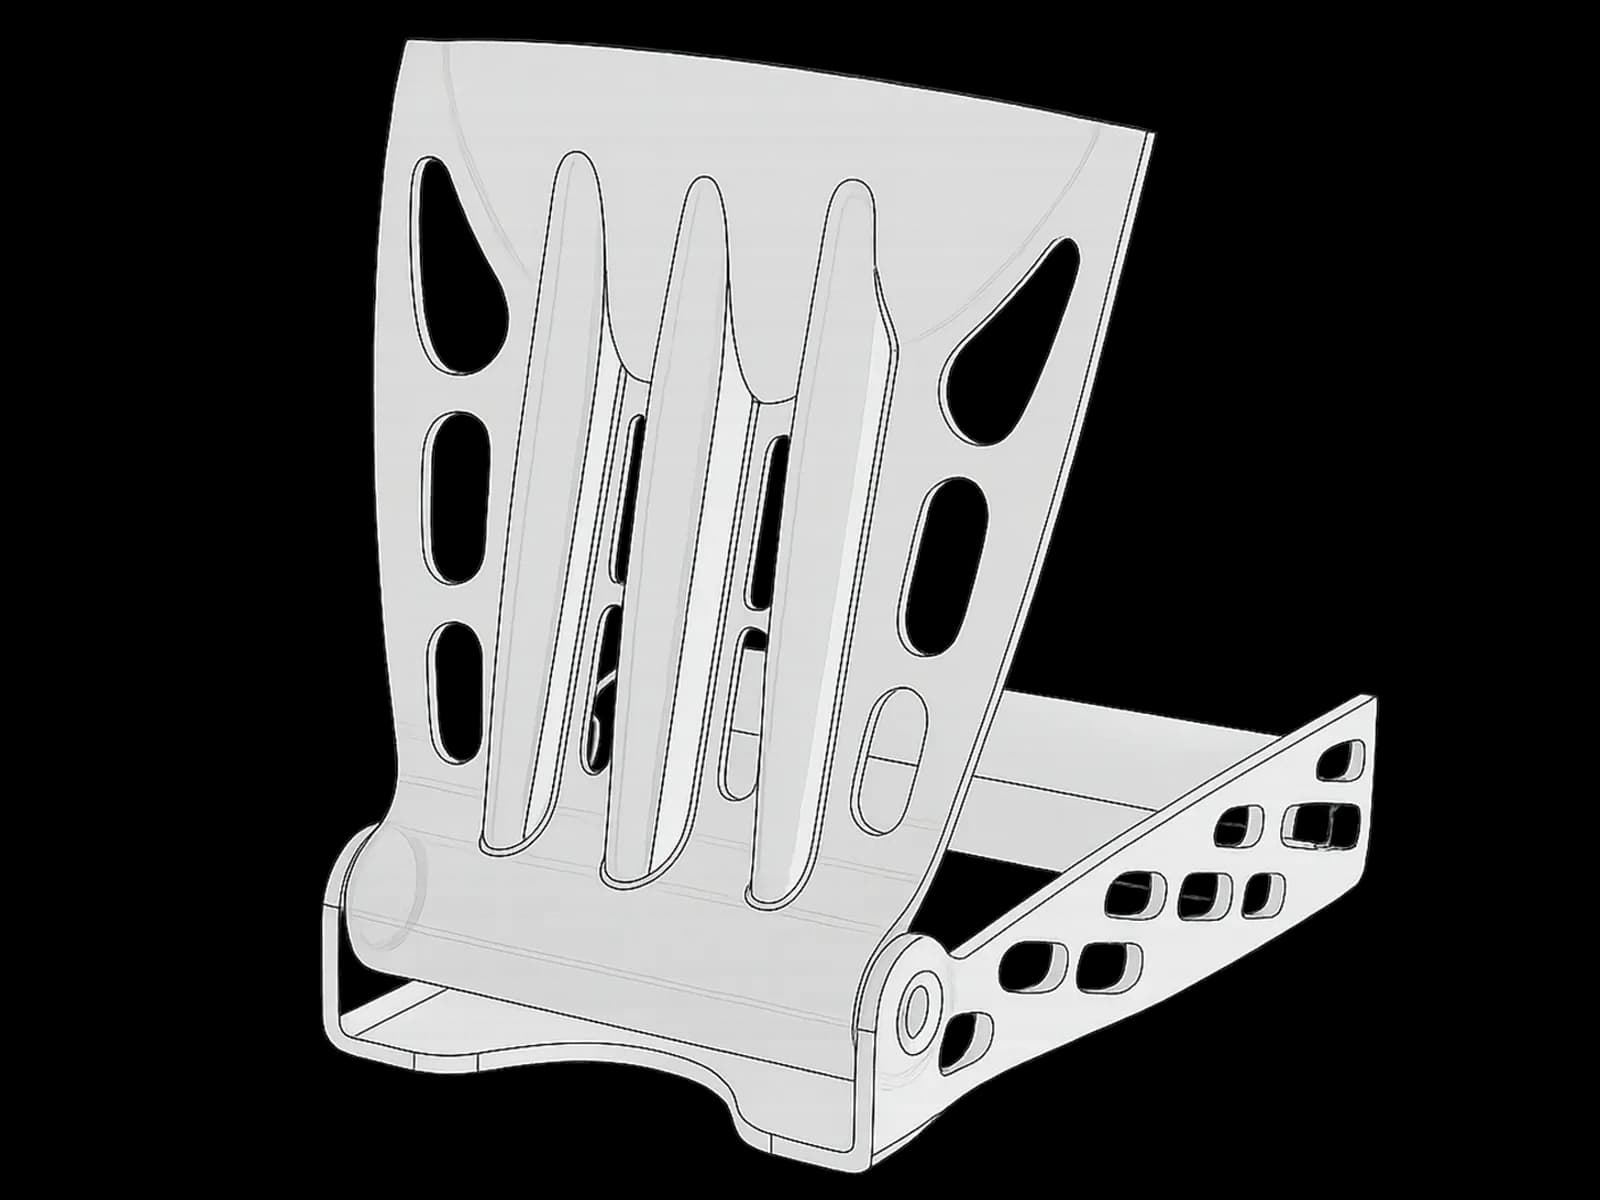
    Aerospace Structures/Precision Components/Automotive Racing/Sports Equipment

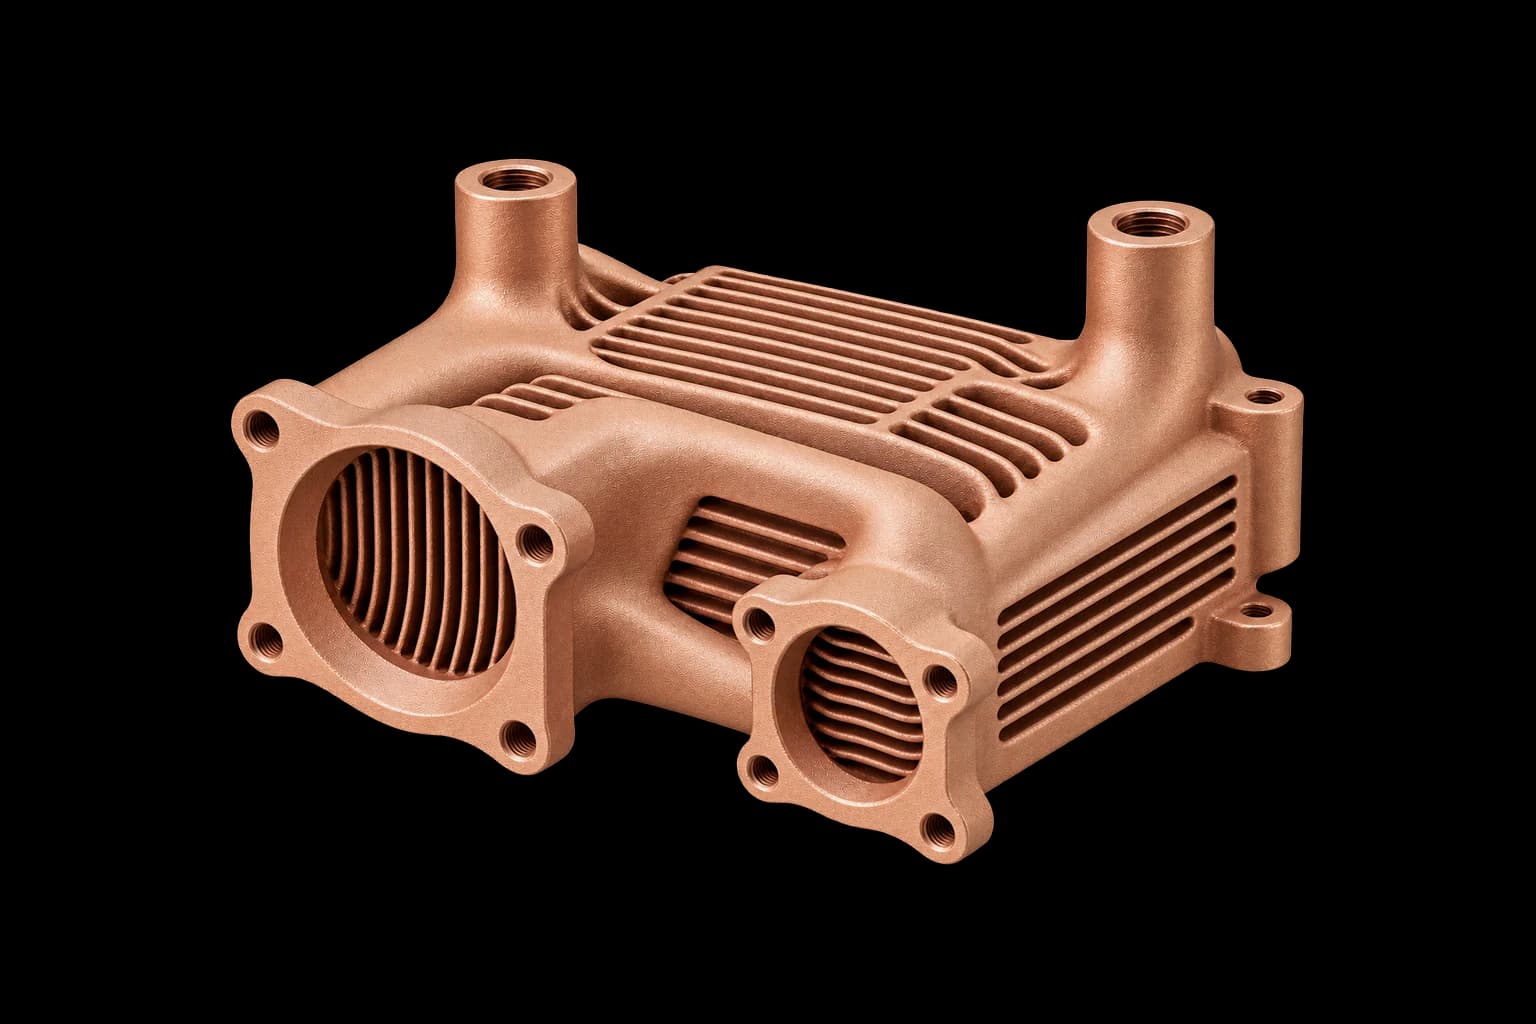
  • Copper CuCrZr Part
    Metal

    Copper CuCrZr

    Copper CuCrZr is a high-conductivity copper alloy for thermal and electrical parts.

    Tensile Strength
    510 / 495 MPa
    Elastic Modulus
    120 / 125 GPa
    Temp Resistance
    See datasheet
    Material details

    Alloyed with chromium and zirconium, it reaches its properties through heat treatment, and EOS offers two cycles: one tuned for conductivity, reaching 88% IACS, and one tuned for strength.

    High-Conductivity Copper Alloy for Thermal and Electrical Parts

    Applications
    Rocket Engine Parts/Heat Exchangers/Induction Coils/Thermal Management

Post-Processing

Material Surface Finishes

DMLS parts generally exhibit a slightly rough, matte finish due to the laser sintering process, resulting in a uniform surface texture. While this natural finish is sufficient for many functional applications, Forge Labs offers several post-processing options to enhance aesthetics, accuracy, and performance.

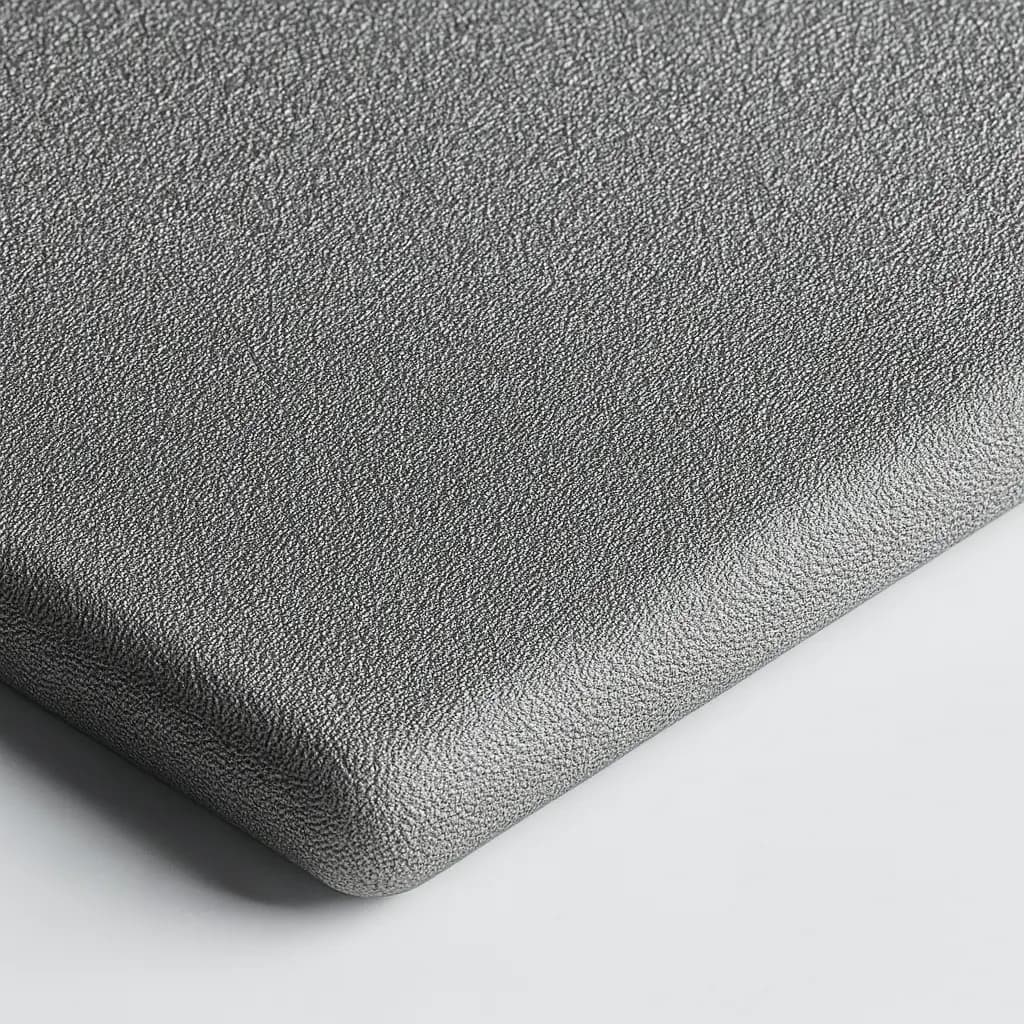
Standard Finish DMLS Finish
Natural

Standard Finish

Support structures are carefully removed, and parts undergo shot peening to create a uniform, matte surface and help relieve residual stresses. Critical features may receive light machining for tighter tolerances.

Finish attributes

Surface TextureUniformly matte surface
AppearanceMatte Grey
DetailsWell represented
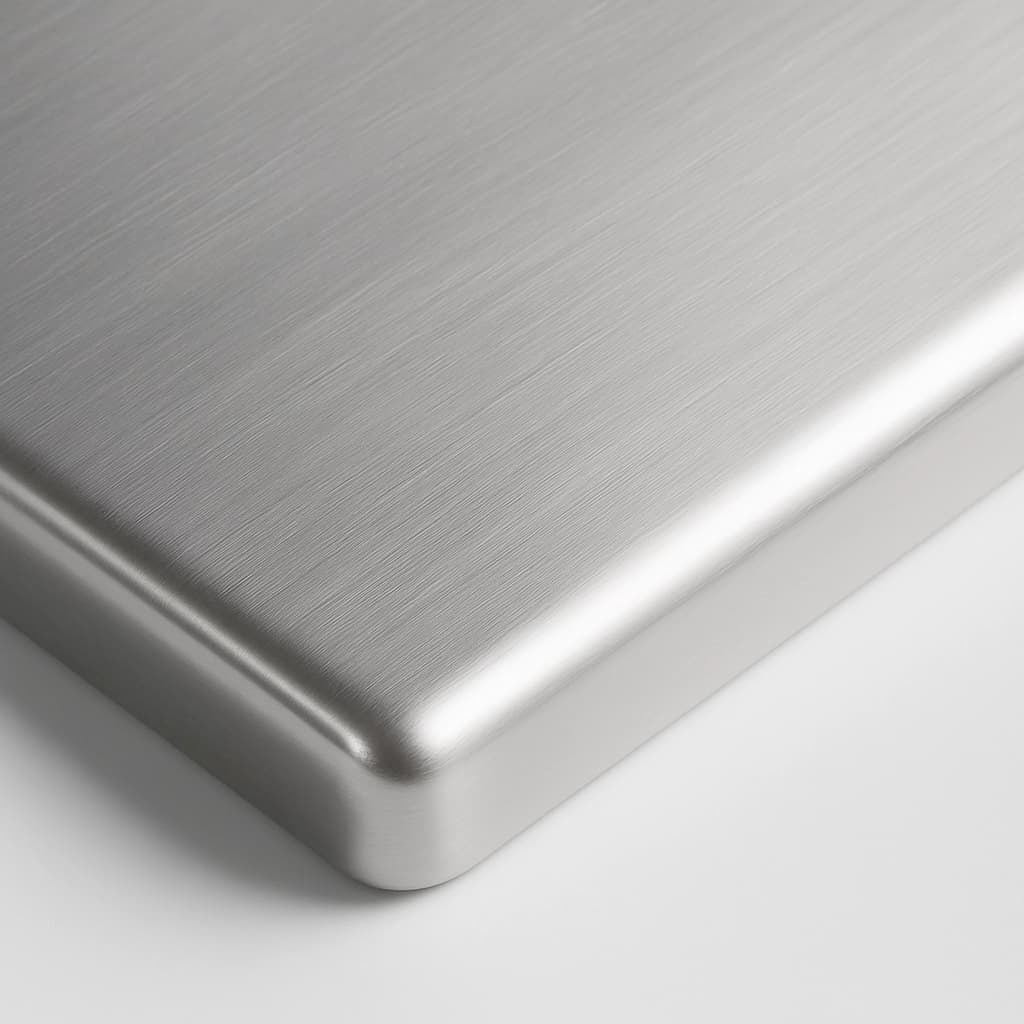
Polished
Natural Finish
Enhanced

Machining & Polishing

Precision machining and polishing processes enhance surface quality, achieving tighter tolerances and smoother finishes for critical applications.

Finish attributes

Surface TextureSmooth, polished finish
AppearanceHigh-gloss metallic
DetailsHigh retention
Anodized
Natural Finish
Protective

Anodizing

For aluminum parts, anodizing forms a protective oxide layer, significantly enhancing corrosion resistance and hardness while improving appearance.

Finish attributes

Surface TextureMatte with reduced texture
AppearanceMatte protective coating
DetailsPreserved
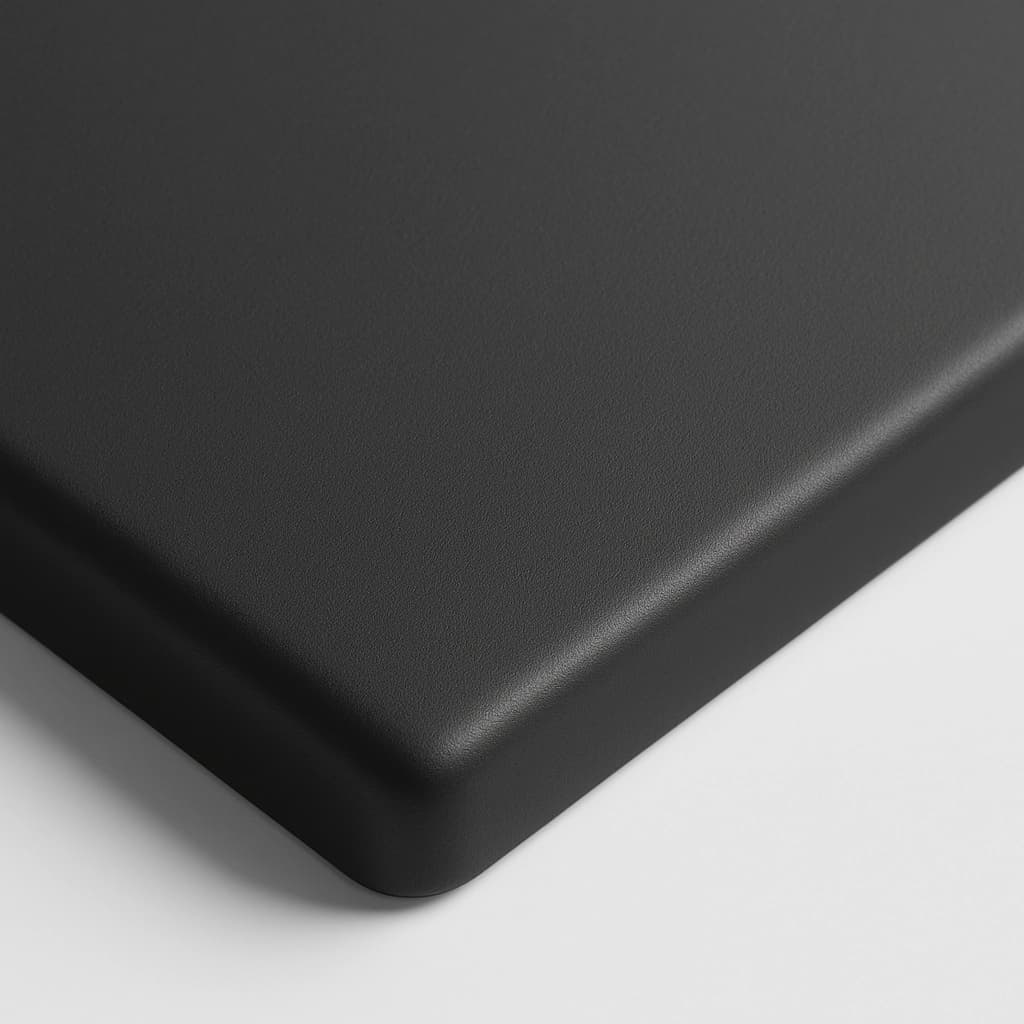
Performance Paint
Natural Finish
Premium

Performance Paint

Automotive-grade coating that enhances aesthetics and durability. Each part is hand-finished with professional-grade equipment for exceptional adhesion and custom color matching.

Finish attributes

Surface TextureMatte to Semi-Gloss
AppearanceCustom color matching available
DetailsClear & refined
Value-Added Services

DMLS Production Services

Metal additive programs require controlled thermal, machining, and inspection steps before release into production.

Stress relief and heat treatment icon

Stress relief and heat treatment

Thermal cycles aligned to alloy requirements and final-use loads.

Support removal planning icon

Support removal planning

Cut strategy to protect datums and reduce secondary rework.

CNC finishing on critical features icon

CNC finishing on critical features

Tight tolerance surfaces machined post-build where required.

Design Guidelines

DMLS Design Guidelines

Our design guidelines for Direct Metal Laser Sintering (DMLS) include important information to improve part quality, minimize costs, and reduce overall manufacturing time. This section is a quick primer before full DFM review.

Maximum Build Volume

Maximum Build Volume

400 x 300 x 400 mm (15.75 x 11.81 x 15.75 in)

Build volumes vary by material:

General Tolerances

General Tolerances

±0.3% (min ±0.3 mm)

Standard production tolerance is ±0.

Minimum Wall Thickness

Minimum Wall Thickness

1.0 mm (0.039")

Supported walls are connected to two or more sides and are thick enough to support the model.

Layer Height

Layer Height

20 - 80 microns

Standard layer height varies by material.

Direct Metal Laser Sintering advantages
Technology Advantages

Why teams choose DMLS

Metal 3D printing with Direct Metal Laser Sintering (DMLS) merges the freedom of additive manufacturing with the proven performance of machined metals, making it especially suitable for low-volume, complex assemblies that need quick turnaround times. By building parts layer by layer, DMLS allows for intricate geometries and consolidates multiple components into a single piece—reducing material waste, tooling costs, and production time.

01Complex Geometries
Being an additive process, intricate internal channels, undercuts, and organic shapes can be printed without the traditional constraints of subtractive machining.
02High Strength & Durability
DMLS parts exhibit excellent mechanical properties and resistance to wear and fatigue, making them suitable for demanding aerospace, automotive, and industrial applications.
03Material Versatility
A variety of industrial-grade alloys—including stainless steels, aluminum, titanium, and superalloys—enable a broad range of functional end-use components.
04Reduced Material Waste
Only the powder required for each build layer is fused, and unfused powder can often be recycled, minimizing raw material waste compared to traditional metal fabrication.
05Faster Iterations
Building parts directly from CAD data shortens lead times, allowing for rapid prototyping and design refinements without expensive tooling.
06Consolidated Assemblies
DMLS allows multiple components to be combined into a single print, reducing part count, assembly steps, and potential points of failure.
Instant Quote Tool

From Upload to Delivery

Upload files, configure manufacturing specs, and track production in one workflow built for engineering teams.

File upload interface
Uploading files

75% complete

Step 01

Upload CAD Files

Automated file checks before production

Drop your CAD files and receive immediate manufacturability feedback. Critical geometry and wall checks run as soon as files are uploaded.

  • Upload STEP, STL, OBJ, and production drawing files
  • Auto-detection for thin walls and trapped volumes
  • Instant design feedback before checkout
Industry Applications
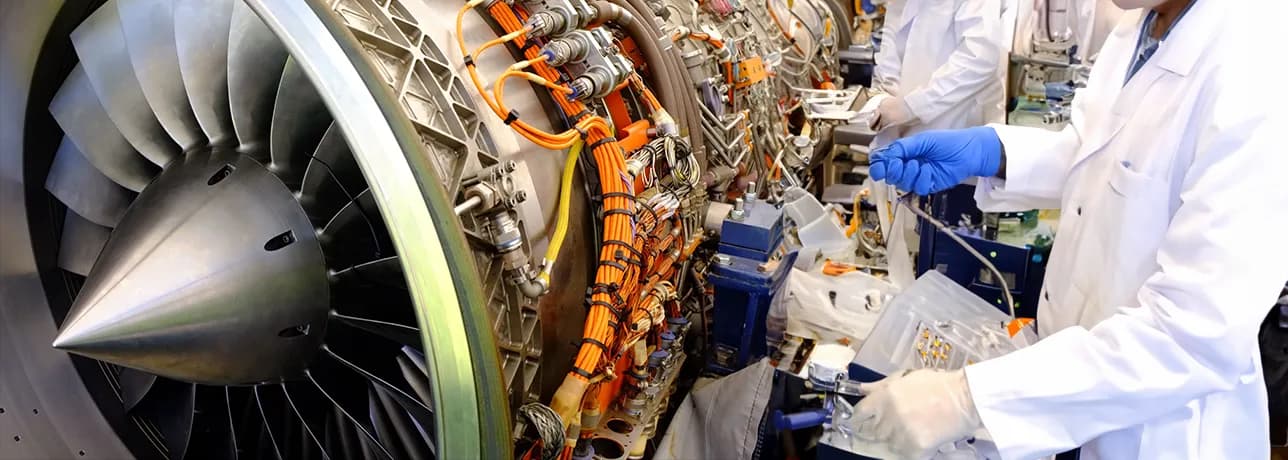
DMLS Applications Across Industries
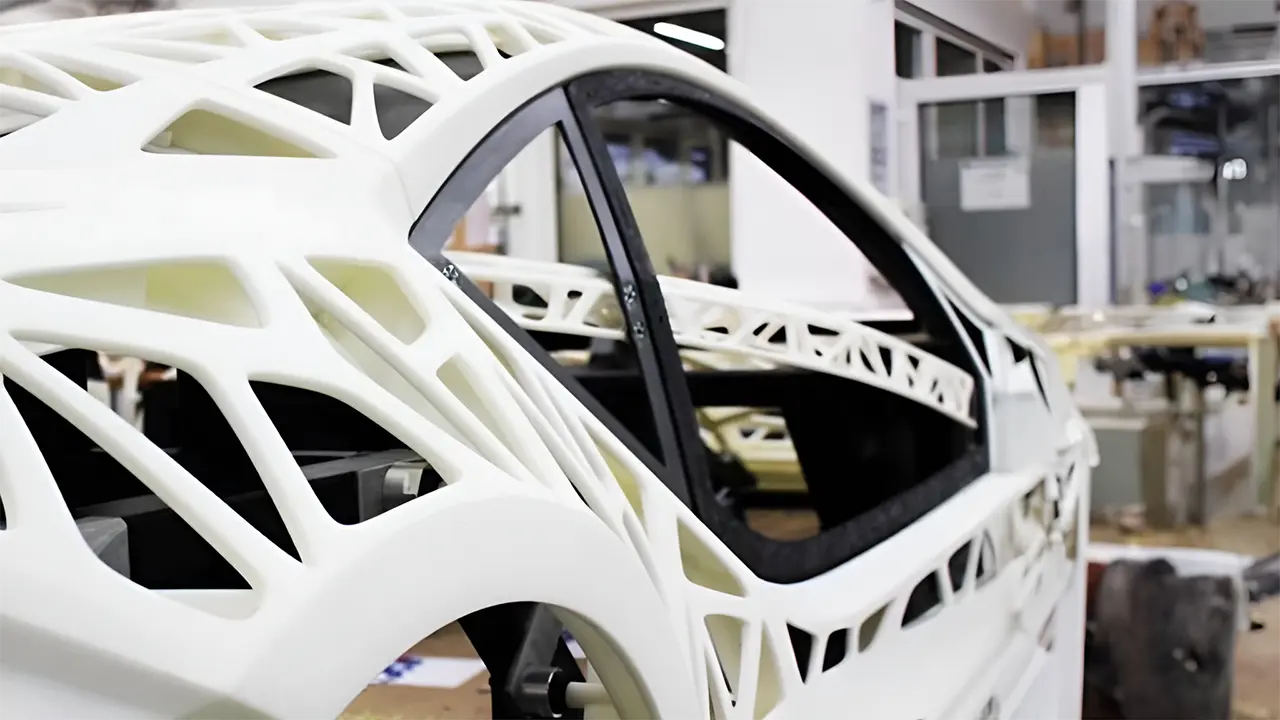
Direct Metal Laser Sintering (DMLS) is used to create functional metal parts with complex internal features. Teams use DMLS to consolidate assemblies, add internal channels, and manufacture high-performance brackets, manifolds, and thermal hardware.

DMLS is selected when you need metal performance with geometry that machining cannot produce, including internal channels and weight-optimized structures. It is often paired with heat treatment and machining on critical features to meet final tolerances.

Start a quote

Ready to manufacture your parts?

Upload your CAD files to get instant quotes for DMLS 3D printing. Professional-grade manufacturing with fast turnaround times.

  • Instant pricing with automated manufacturability analysis
  • Production workflows built for repeatable quality
  • Engineering support from prototype to production
View design guidelines

Create an account to upload CAD

STEP, STL, OBJ, 3MF and IGES supported

Manufacturing technologies
6
Engineering materials
50+
Part quantities
1-500+
Frequently Asked Questions

DMLS Questions & Answers

Common questions about DMLS 3D printing technology. Can't find what you're looking for? Reach out to our technical team.