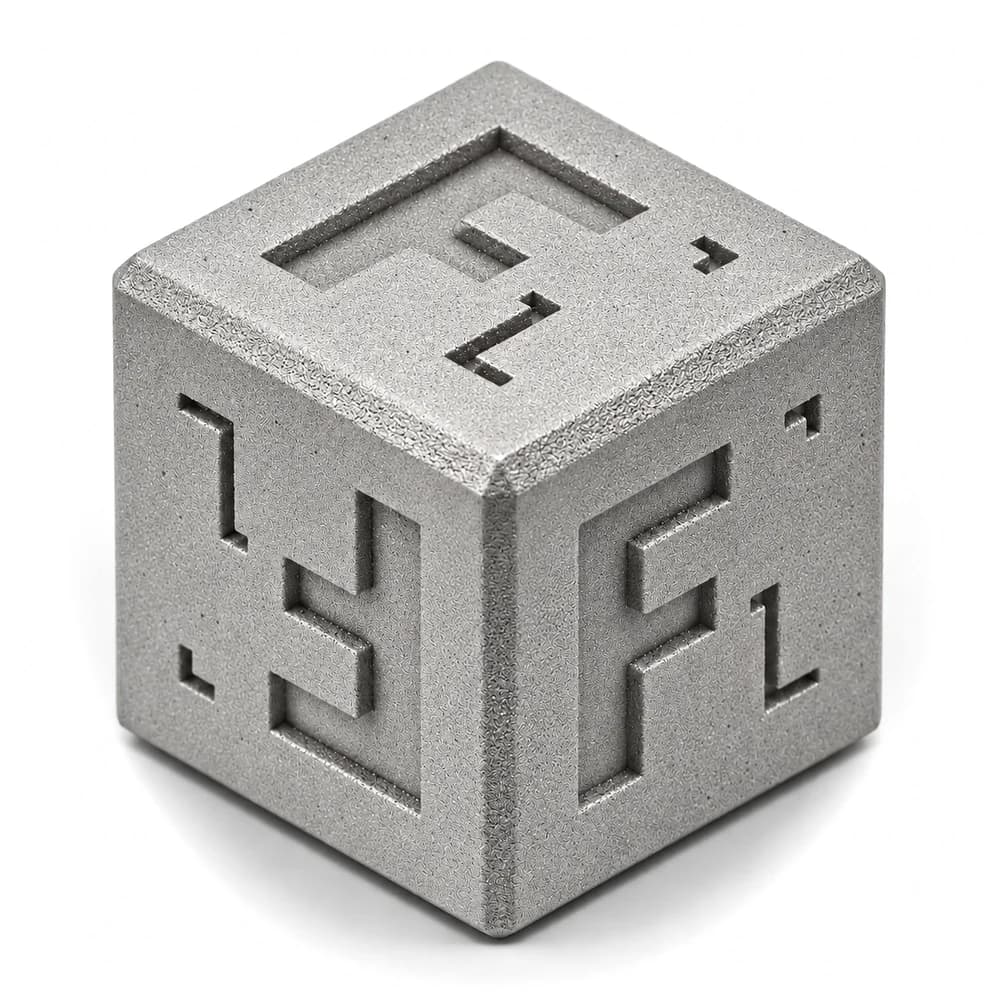
Direct Metal Laser Sintering Stainless Steel 316L For Corrosion-Resistant Parts in Harsh Environments

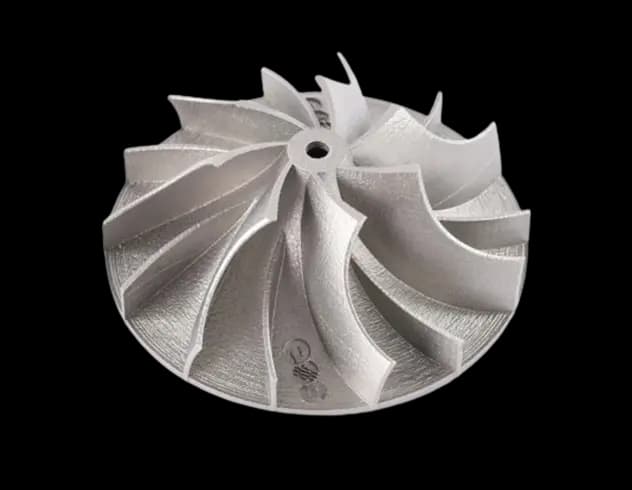
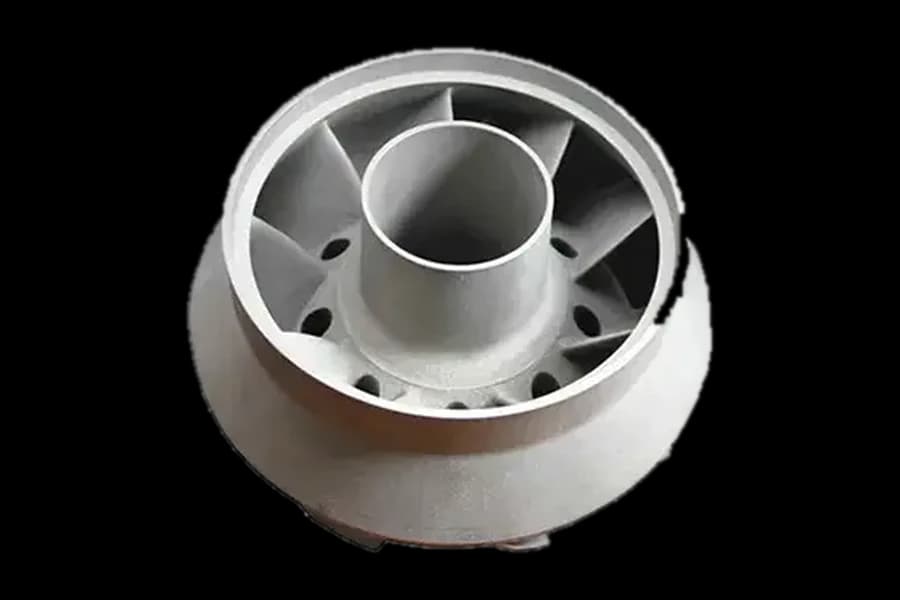
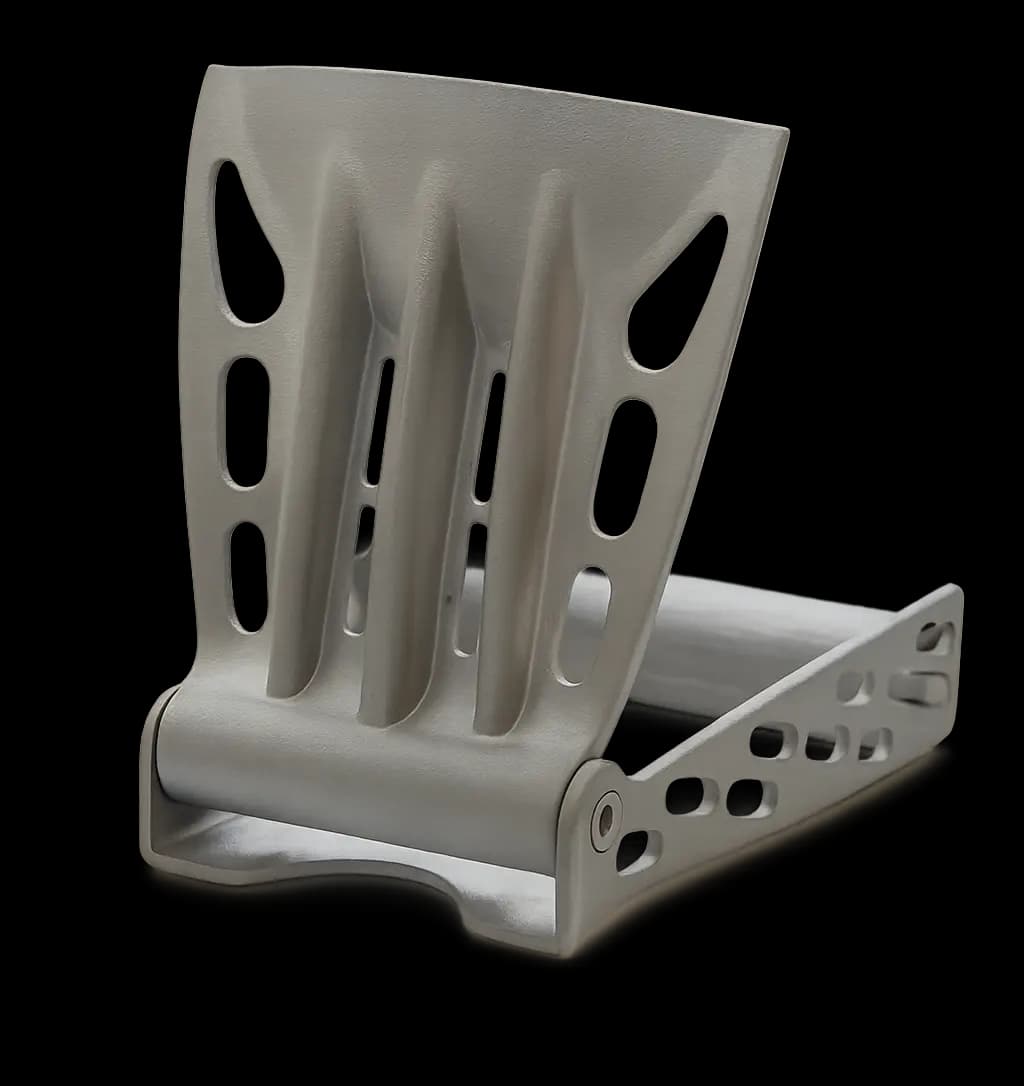
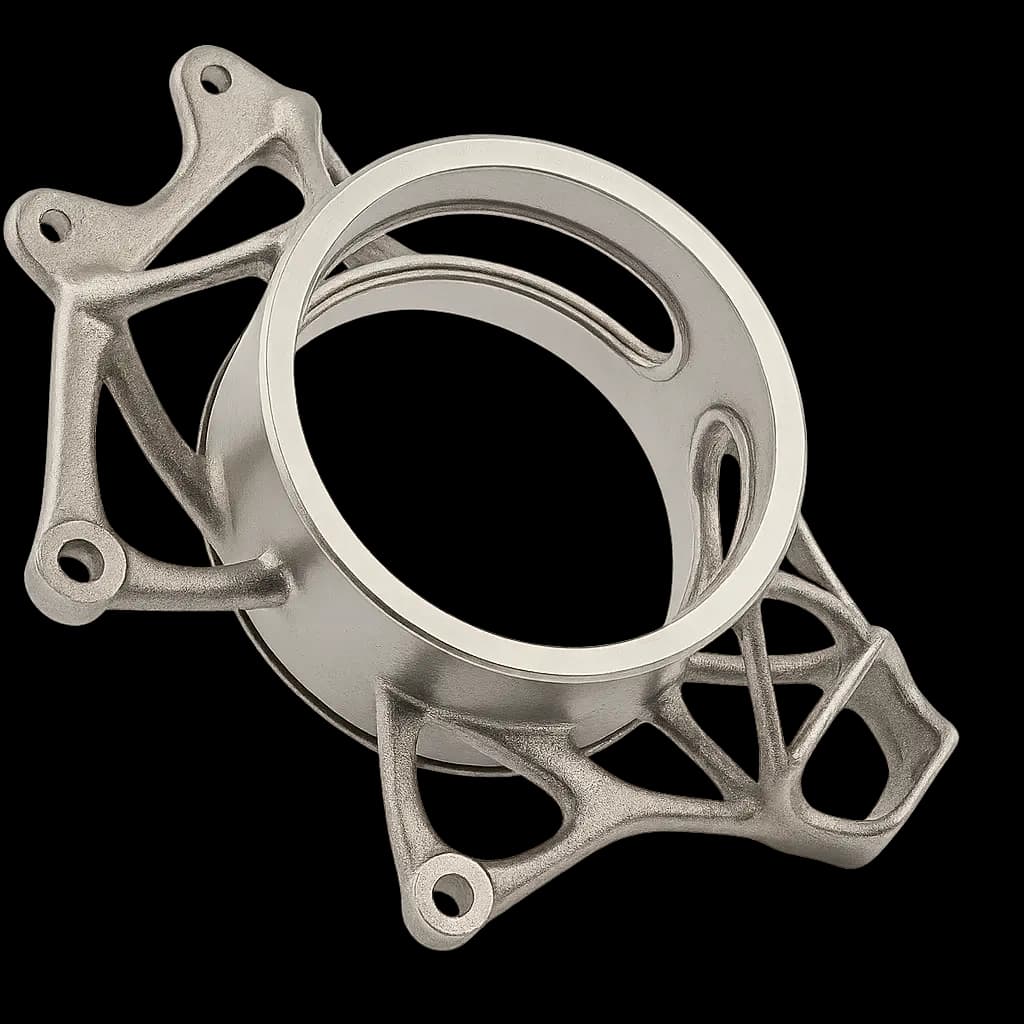
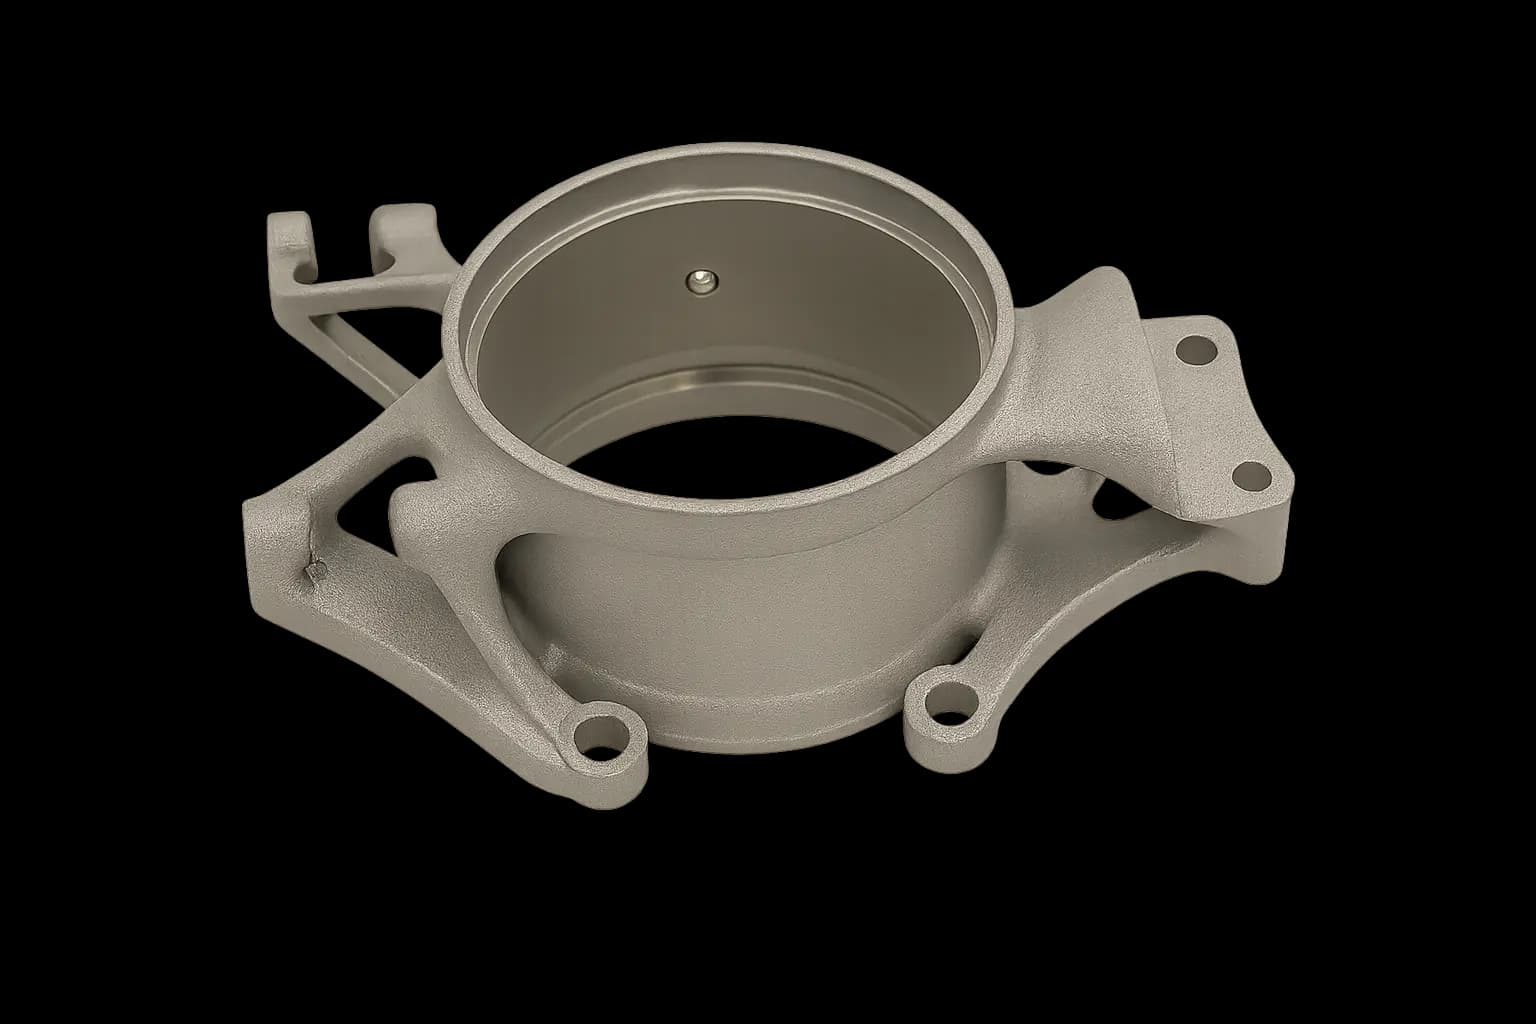
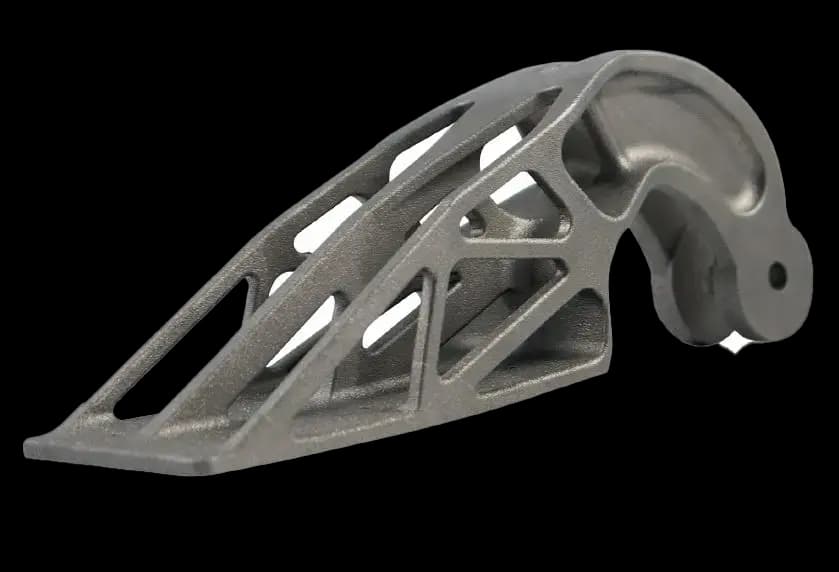
Stainless Steel 316L 3D printed part example
Metal Precision
Industrial Grade
DMLS material

Stainless Steel 316L overview

Stainless Steel 316L is a marine-grade stainless steel, 3D printed by DMLS, for parts that face salt air, chemicals and repeated washdowns. Its added molybdenum gives it strong resistance to chlorides, and it bends rather than cracks, absorbing impact and vibration. Printing turns valves, manifolds, static mixers and test fixtures with internal passages into single parts that are easy to clean. Marine, chemical processing, food production, power generation and aerospace teams use it, along with medical device teams for non-implant tooling and fixtures.

How Stainless Steel 316L is manufactured

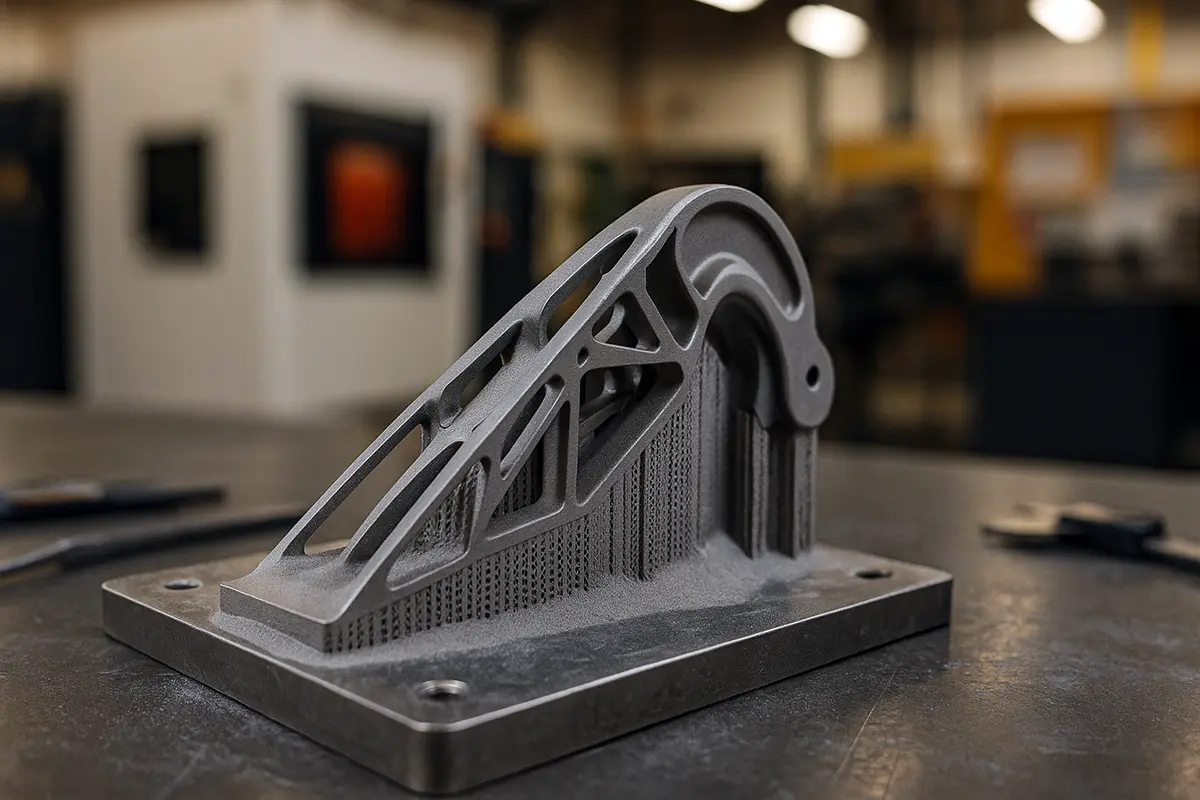
Stainless Steel 316L is manufactured using Direct Metal Laser Sintering (DMLS) on EOS M 290 systems, an industrial powder-bed process in which a laser melts fine stainless steel powder layer by layer in an inert argon atmosphere. Precision F-theta optics keep the laser beam consistent across the entire build platform, and support structures anchor each part to the build plate. This allows complex geometries, internal channels and consolidated designs to be produced in one build, with repeatable quality from the first part to the last.

Build volume
250 × 250 × 325 mm
Lead time
From 4 business days
Layer height
0.02-0.08 mm
Forge Labs Steam

Know before you manufacture in Stainless Steel 316L.

Upload CAD files to Forge Labs Steam for instant Stainless Steel 316L pricing and live manufacturability feedback, and fix issues before production.

Upload CAD files to Forge Labs Steam for instant Stainless Steel 316L pricing and live manufacturability feedback, and fix issues before production.

Surface finishes

Finishes for Stainless Steel 316L

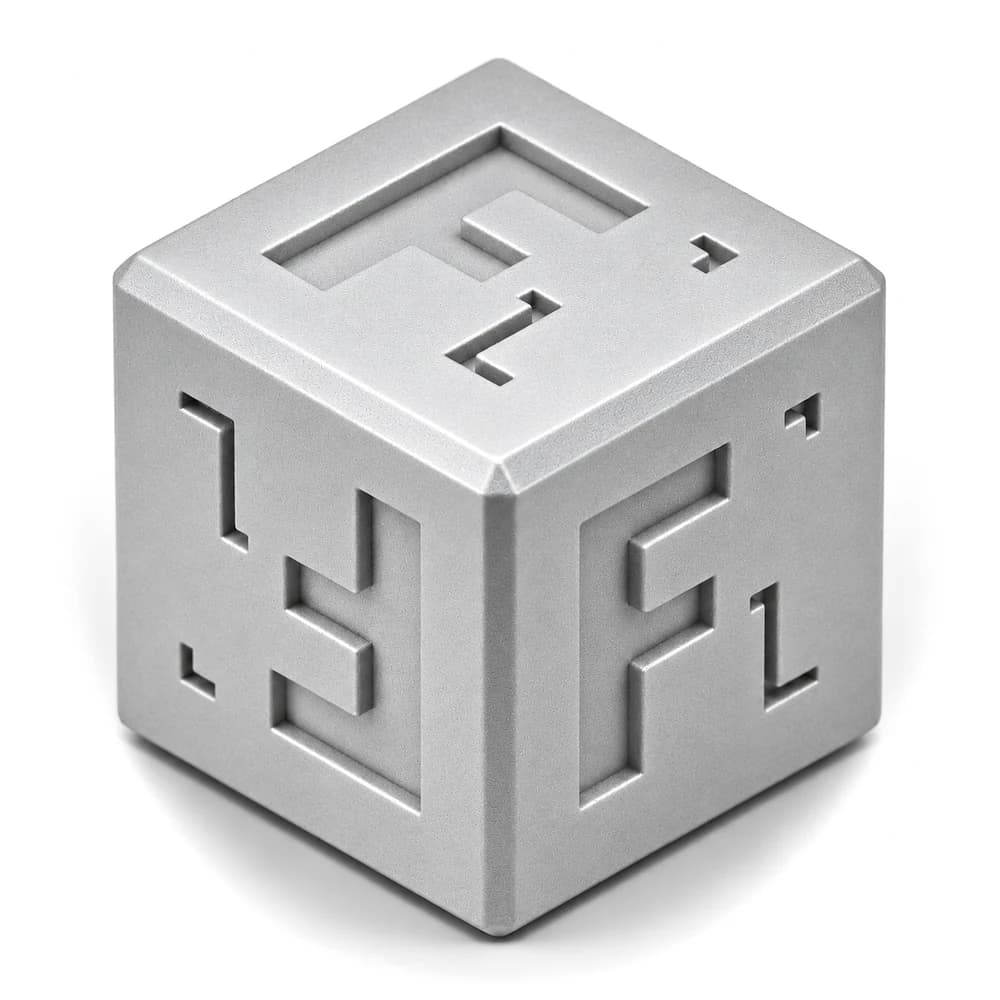
DMLS parts generally exhibit a slightly rough, matte finish due to the laser sintering process, resulting in a uniform surface texture. While this natural finish is sufficient for many functional applications, Forge Labs offers several post-processing options to enhance aesthetics, accuracy, and performance.

Forge Labs sample cube in bead-blasted DMLS stainless steel 316L
Natural

Standard Finish

Support structures are carefully removed, and parts undergo shot peening to create a uniform, matte surface and help relieve residual stresses. Critical features may receive light machining for tighter tolerances.

Surface Texture
Uniformly matte surface
Appearance
Matte Grey
Details
Well represented
Sample cube with a machined and polished satin metal finish
Forge Labs sample cube in bead-blasted DMLS stainless steel 316L
Enhanced

Machining & Polishing

Precision machining and polishing processes enhance surface quality, achieving tighter tolerances and smoother finishes for critical applications.

Surface Texture
Smooth, polished finish
Appearance
High-gloss metallic
Details
High retention
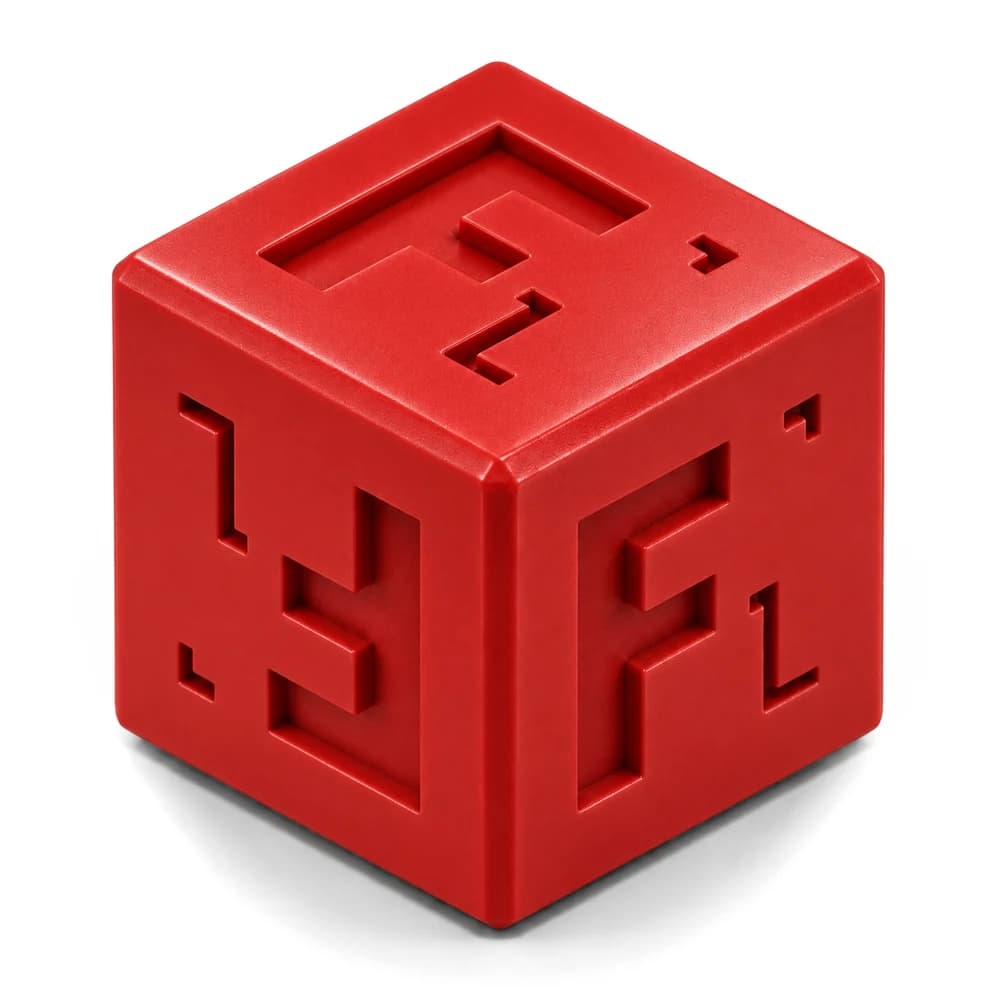
Sample cube with a red automotive-grade performance paint finish
Forge Labs sample cube in bead-blasted DMLS stainless steel 316L
Premium

Performance Paint

Automotive-grade coating that enhances aesthetics and durability. Each part is hand-finished with professional-grade equipment for exceptional adhesion and custom color matching.

Surface Texture
Matte to Semi-Gloss
Appearance
Custom color matching available
Details
Clear & refined
Industry applications

Industry applications for Stainless Steel 316L

EOS Stainless Steel 316L is a production-grade DMLS stainless steel for corrosion-resistant 3D printed parts in marine, chemical processing, food production, and industrial equipment programs. From valves and manifolds to enclosures, brackets, and flow components, 316L supports complex geometries while maintaining cleanability and consistent field performance in harsh environments.

Design teams rely on 316L where chloride exposure, washdown cycles, and long service life matter, and the alloy's ductility helps absorb impact and vibration without brittle failure. Its molybdenum content gives a pitting resistance equivalent (PREN) above 24, so it holds up in marine atmospheres and chloride waters.

It also serves pharmaceutical tooling and stainless emblems and trim, parts that need durable stainless performance without tooling lead times. Teams use Stainless Steel 316L to hold tight tolerances while reducing assembly complexity through consolidated part designs.

Forge Labs gives teams a reliable path from prototyping to repeatable production, with fast iteration across low- to mid-volume runs.

All industries
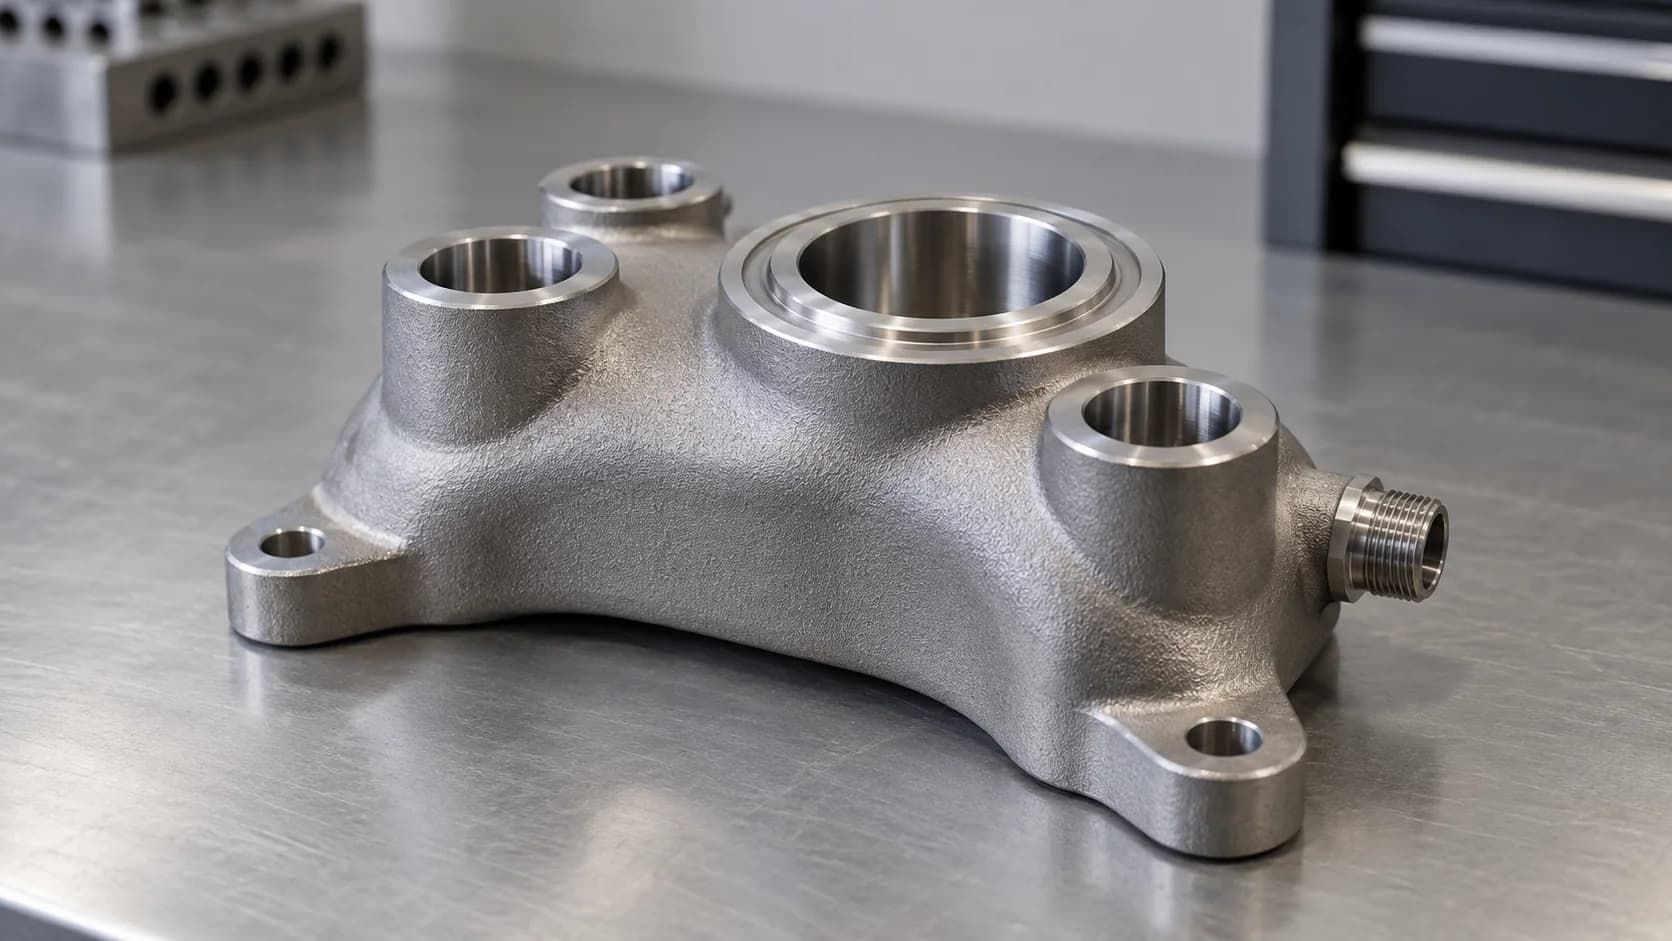
Printed stainless steel test-fixture body with machined ports and a circular seal seat on a workshop bench

Aerospace MRO

Engine Test Fixtures & Maintenance Tooling

Engine maintenance shops use Stainless Steel 316L for test plates and handheld air-test fixtures, where internal air passages, threaded ports and O-ring seals have to work together in one tough body. One printed fixture replaced three separate tools: its passages were printed in place, then bores, pipe threads and O-ring grooves were machined to the drawing, with seal faces finished to about 0.8 µm Ra. The finished body shipped within three business days of a successful print.

  • Engine test plates
  • Handheld air-test fixtures
  • Small MRO replacement parts
Read the stainless test fixture case study
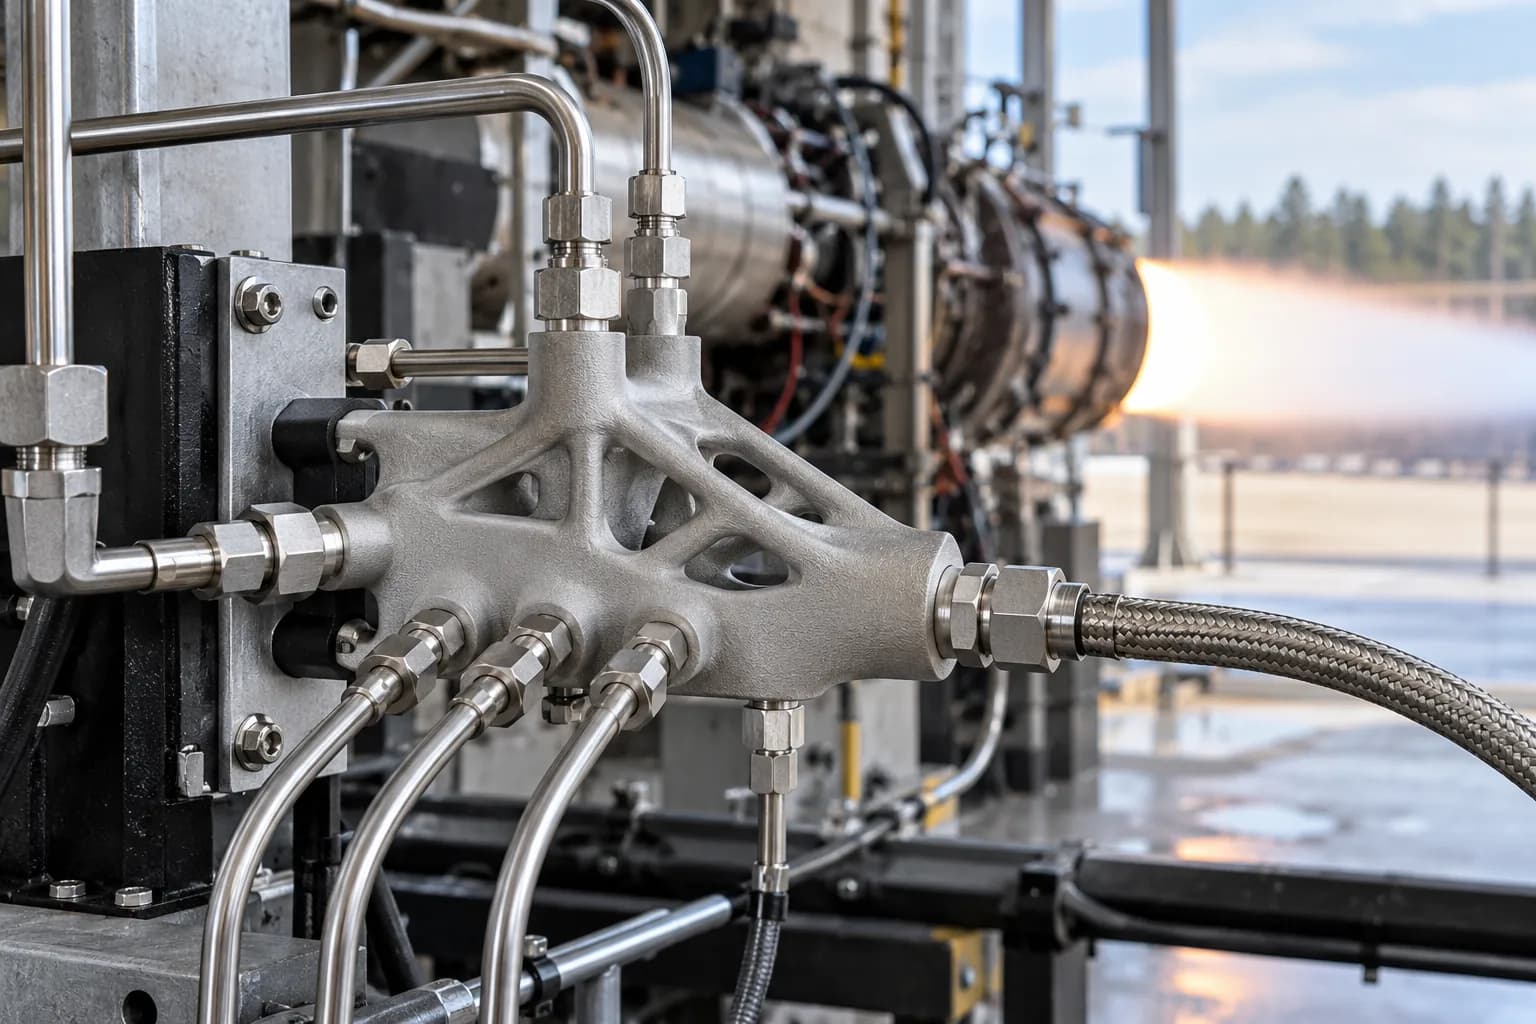
DMLS 316L instrumentation manifold on a propulsion test stand

Aerospace

Propulsion & Test Instrumentation

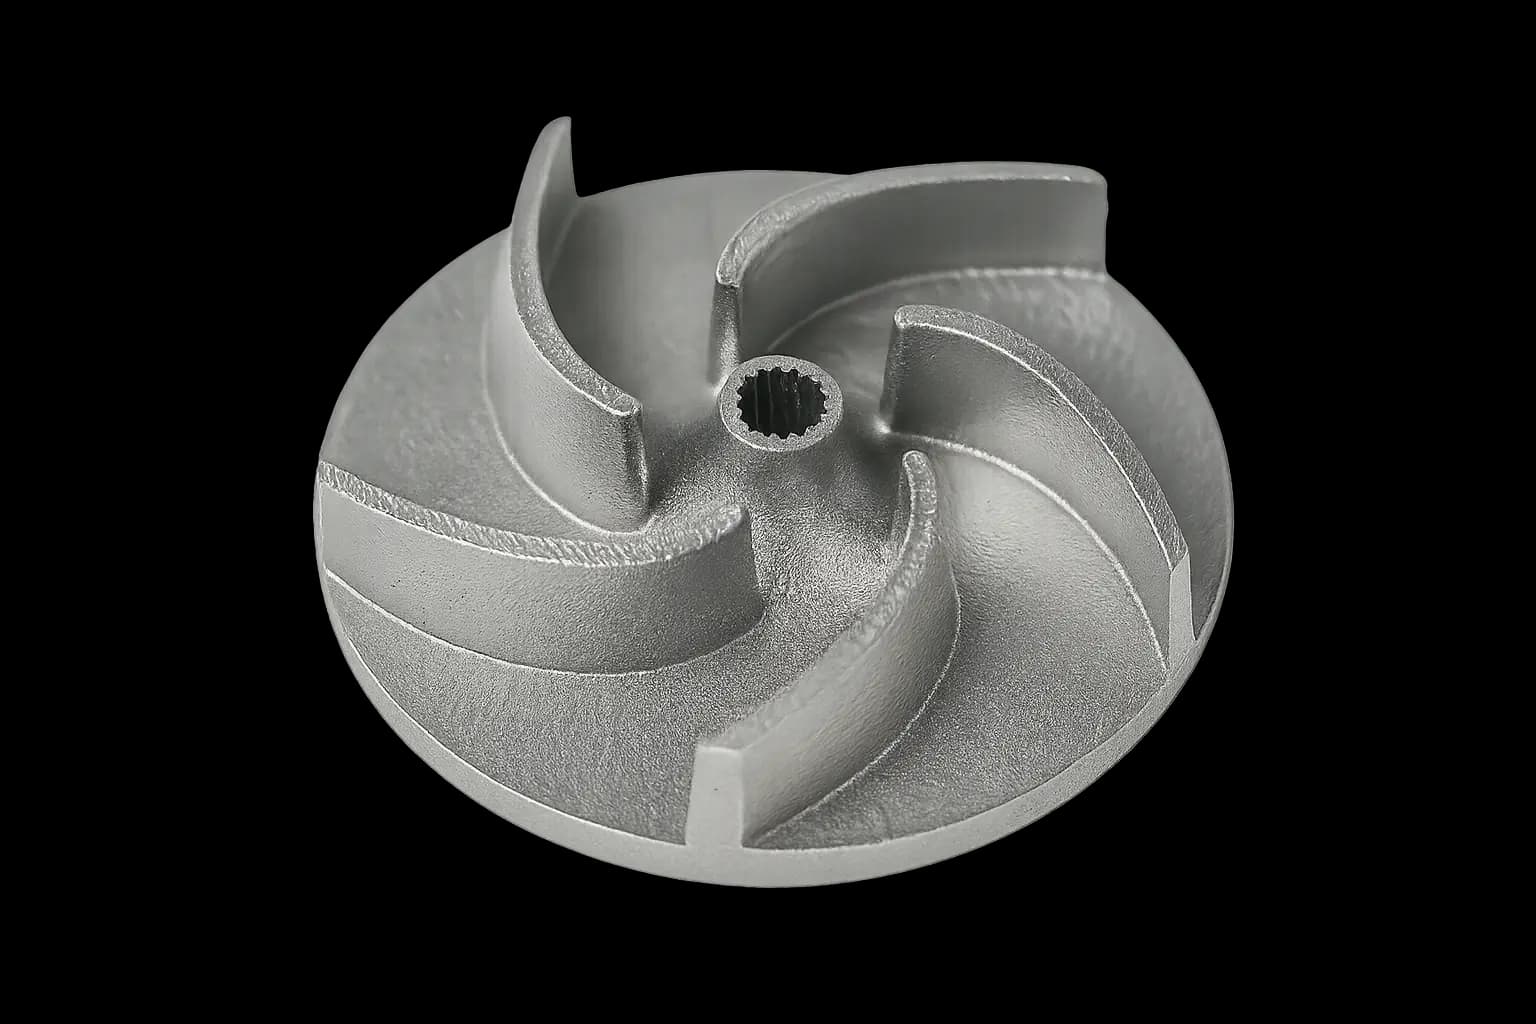
Propulsion developers order combustor swirlers in runs of 35, a radial fuel-pump impeller, and pitot rakes and their sheaths for test instrumentation, printed in DMLS alloys including 316L. Heat treatment, HIP and machining are available where the drawing calls for them. Of those alloys, 316L is the most ductile, with 41% elongation horizontally and 49% vertically as built.

  • Combustor swirlers
  • Fuel-pump impellers
  • Pitot rakes and sheaths
Explore aerospace
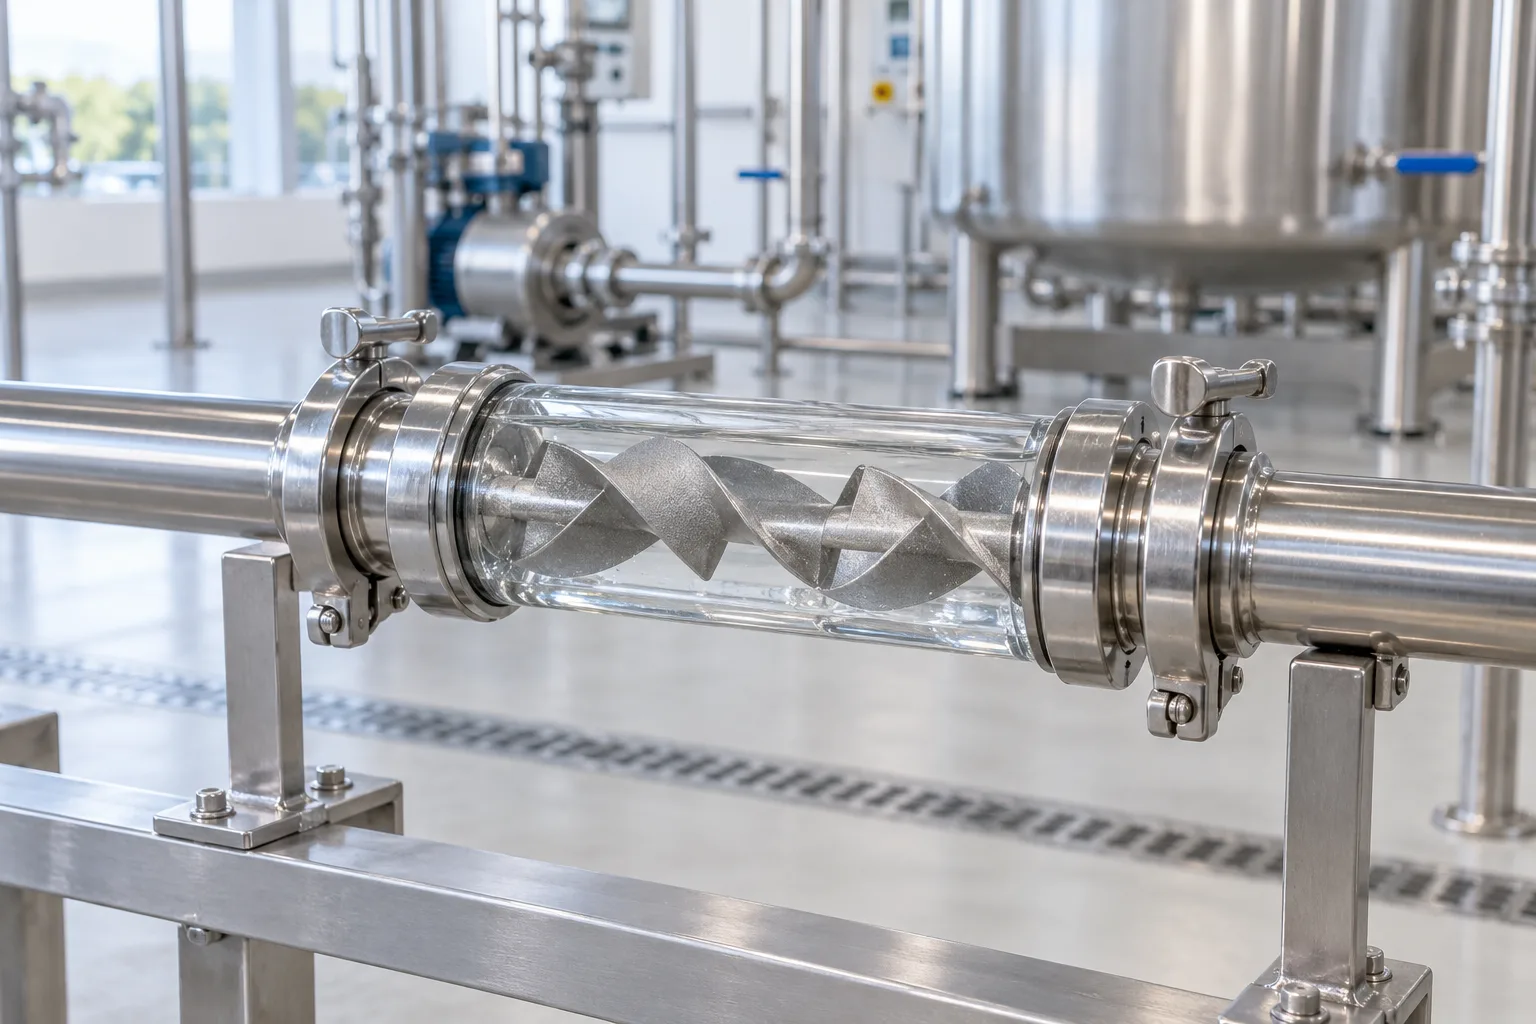
Printed stainless helical static mixer with tri-clamp ends in a clear section of a process line

Clean Tech & Process

Static Mixers & Process Fittings

Process equipment makers use DMLS 316L for helical static-mixer vanes up to 380 mm long with sanitary tri-clamp ends, and for tees with NPT threads and hose barbs. The internal geometry that makes a mixer work would need several machined and welded pieces; printed, it is one part. 316L resists phosphoric and acetic acids, caustic cleaning solutions and organic solvents, which suits reactor nozzles, valve bodies, spray nozzles and dairy or brewery fittings.

  • Helical static mixers
  • Threaded tees and hose barbs
  • Spray nozzles and valve bodies
Explore clean tech
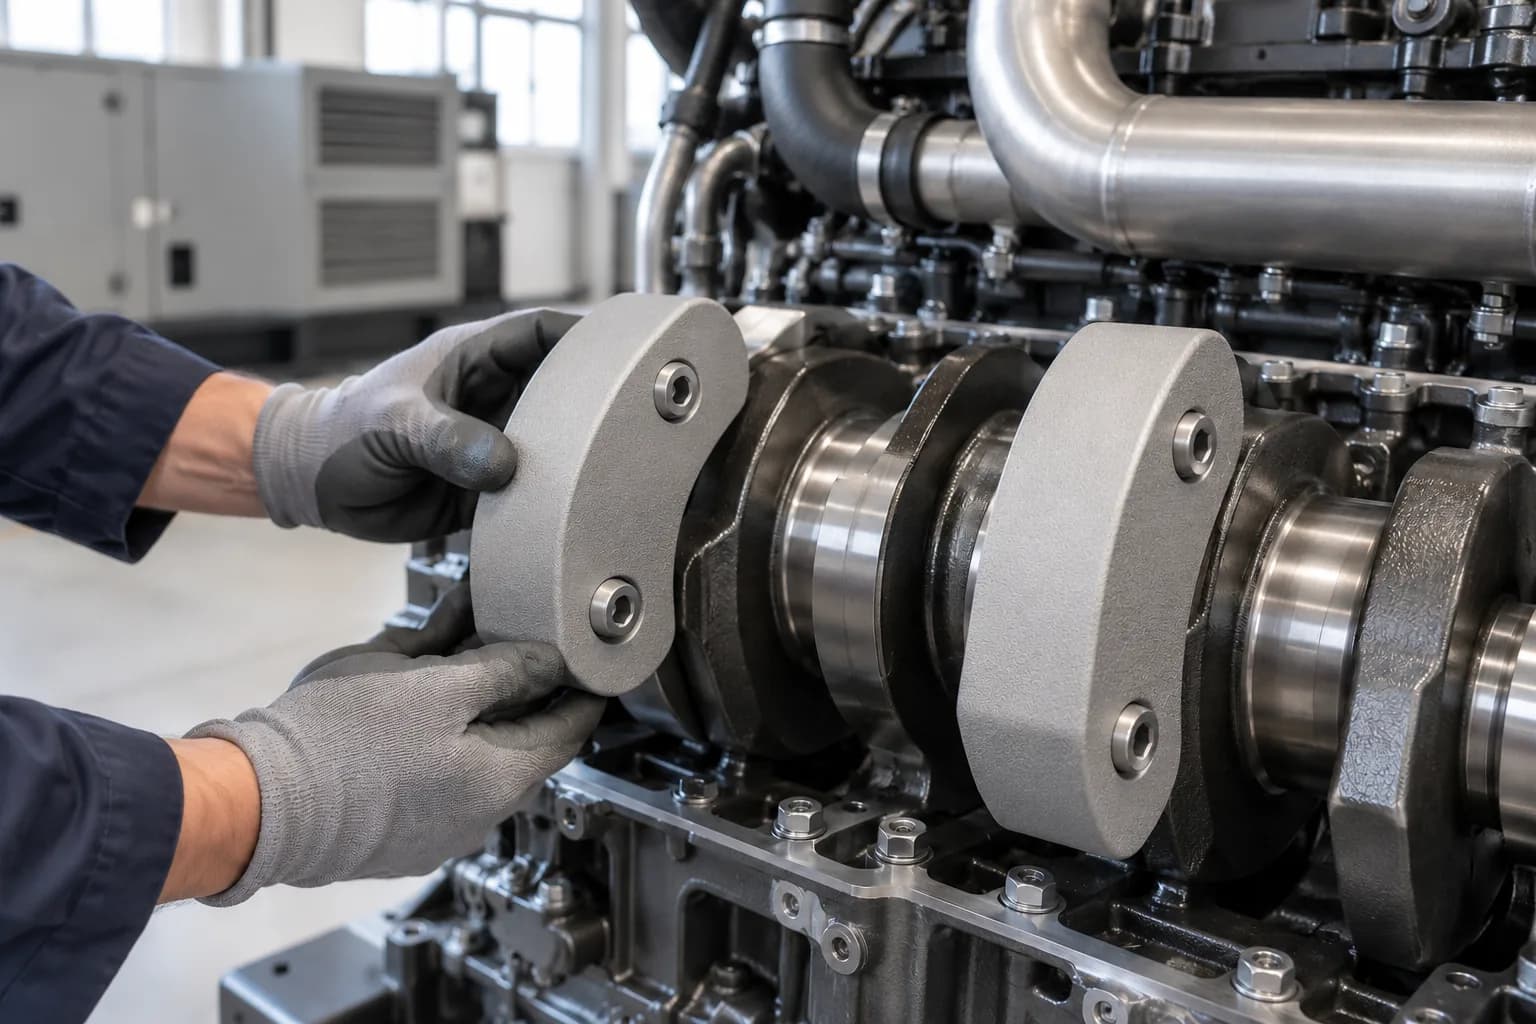
DMLS 316L counterweights on a generator engine

Power Generation

Engine Counterweights & Valve Parts

Power generation equipment makers use DMLS 316L for screw-in counterweights drawn in hot-rolled steel, and for valve plates and valve heads. 316L weighs about the same as the drawn steel, so the designed mass carries over, and the counterweight thread is cut after printing to mate with its piston. A valve plate was printed as modeled and sampled at ±0.3 mm with every reading passing, and the counterweights shipped with their aluminum pistons in 13 business days, on the promised date.

  • Screw-in counterweights
  • Valve plates and valve heads
  • Small engine parts
Read the DMLS engine parts case study
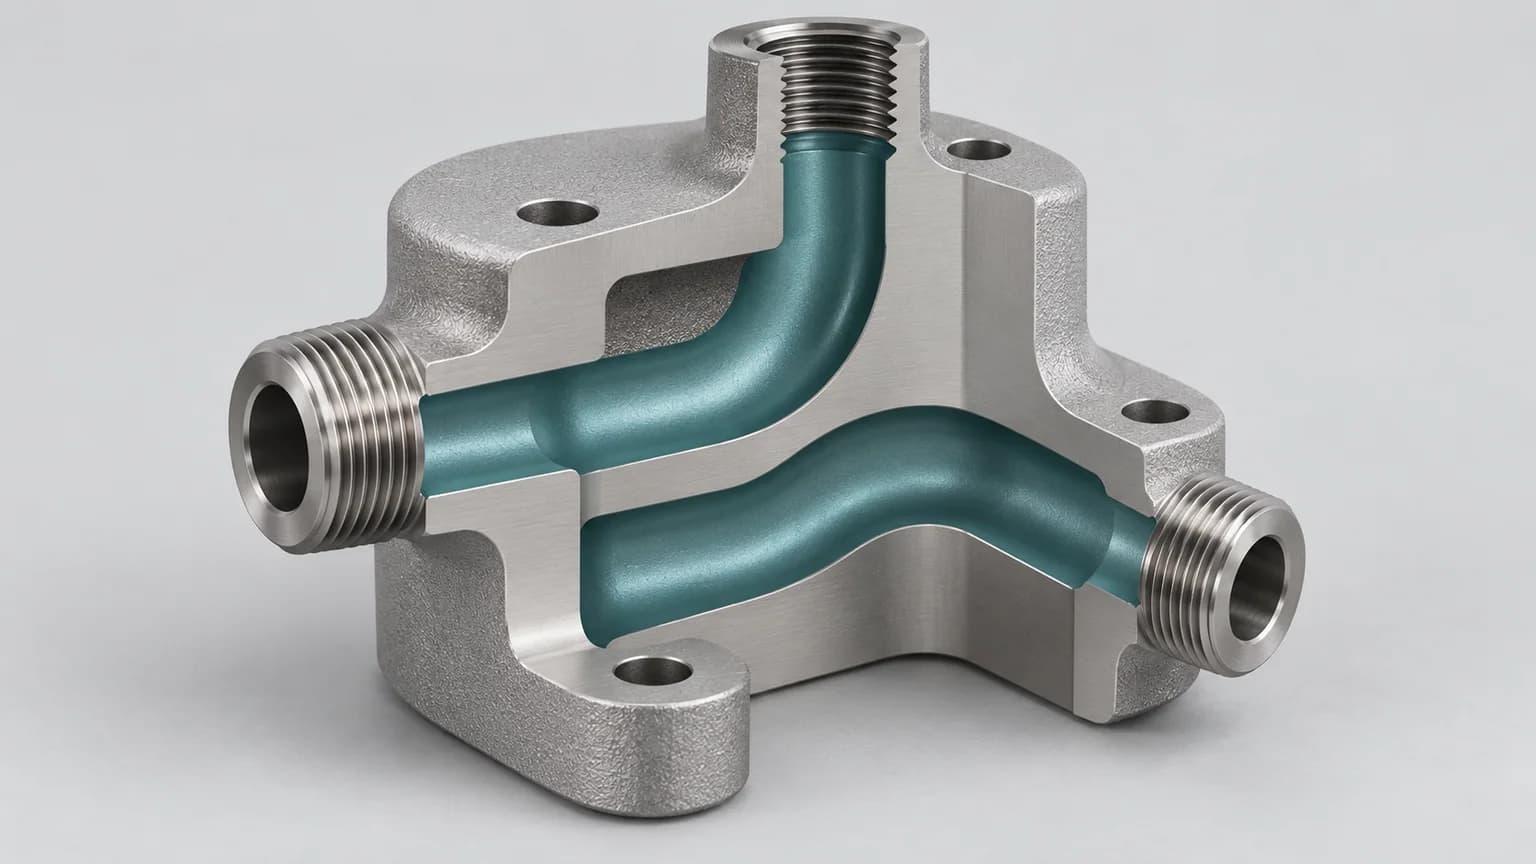
Cutaway of a printed stainless steel body showing smooth internal passages and threaded ports

Medical & Healthcare

Instrument Components & Validation Fixtures

Medical device teams use Stainless Steel 316L for non-implant surgical tooling, handling fixtures, validation fixtures and cleanable process hardware for GMP environments. The powder chemistry corresponds to ASTM F138 (UNS S31673), and serialized lot and build traceability supports the device maker's pilot lots and qualification plans.

  • Non-implant surgical tooling
  • Validation and verification fixtures
  • Cleanable GMP process hardware
Explore medical devices
Performance data

Technical performance for Stainless Steel 316L

Values from the EOS StainlessSteel 316L-4441 datasheet for the EOS M 290 (40 µm), tested to the standard listed with each property. Modulus, hardness, surface roughness and thermal expansion come from EOS's 20 µm datasheets, and alloy constants EOS does not publish come from wrought 316L mill data.

Mechanical performance

Mechanical properties

Stainless Steel 316L delivers dependable strength with exceptional ductility, giving teams a proven DMLS baseline for chemical processing equipment, valves and precision mechanical assemblies. Its balanced mechanical profile handles demanding load conditions while preventing brittleness in critical applications, and its high elongation lets parts deform rather than crack under overload.

The values are for parts as built, with no heat treatment. The horizontal and vertical rows show the modest anisotropy of laser-melted stainless steel, so plan the load direction of critical features in parts that need precise geometry and tight tolerances.

PropertyValue
Tensile Strength (Horizontal)EN ISO 6892-1
630 MPa
Tensile Strength (Vertical)EN ISO 6892-1
580 MPa
Yield Strength Rp0.2 (Horizontal)EN ISO 6892-1
530 MPa
Yield Strength Rp0.2 (Vertical)EN ISO 6892-1
490 MPa
Elongation at Break (Horizontal)EN ISO 6892-1
41 %
Elongation at Break (Vertical)EN ISO 6892-1
49 %
Young's Modulus (Horizontal)ISO 6892 / ASTM E8M (EOS MDS 2014, 20 µm set)
185 GPa
Young's Modulus (Vertical)ISO 6892 / ASTM E8M (EOS MDS 2014, 20 µm set)
180 GPa
Hardness (Rockwell B)EN ISO 6508-1 (EOS MDS 2014, 20 µm set)
89 HRB

Material makeup

Physical properties

Near-full density keeps critical features in tolerance and downstream finishing predictable, and the defect percentage shows how little porosity remains in the printed metal.

Surface roughness is given as built and after shot peening. Machining and polishing take sealing faces and cosmetic surfaces finer still, and 316L can be polished to a mirror finish for aesthetic applications.

PropertyValue
Part DensityEN ISO 3369
≥ 7.97 g/cm³
Average Defect PercentageEOS method
0.015 %
Surface Roughness Ra (as built, vertical faces)EOS MDS 2014, 20 µm set
13 ± 5 µm
Surface Roughness Ra (shot peened, vertical faces)EOS MDS 2014, 20 µm set
5 ± 2 µm

Heat performance

Thermal properties

Stainless Steel 316L suits chemical processing and food equipment that is heated, washed down and cooled. Its relatively high thermal expansion, which rises with temperature, matters where 316L mates with other metals or polymers.

Avoid long-term service in the carbide-precipitation range EOS lists, where carbides can form at the grain boundaries and reduce corrosion resistance. The melting range, conductivity, specific heat and oxidation limit support heat-transfer and high-temperature design.

PropertyValue
Coefficient of Thermal Expansion (25–100 °C)ASTM E228 (EOS Premium MDS, 20 µm set)
15.72 ×10⁻⁶/K
Coefficient of Thermal Expansion (25–400 °C)ASTM E228 (EOS Premium MDS, 20 µm set)
17.70 ×10⁻⁶/K
Carbide Precipitation Range (avoid in long-term service)EOS MDS 2014
427–816 °C
Melting RangeWrought 316L reference (AK Steel)
1371–1399 °C
Thermal Conductivity (100 °C)Wrought 316L reference (AK Steel)
16.2 W/m·K
Specific Heat Capacity (0–100 °C)Wrought 316L reference (AK Steel)
500 J/kg·K
Oxidation Resistance in Air (intermittent service)Wrought 316L reference (Macsteel)
870 °C

Functional performance

Electrical properties

Stainless Steel 316L conducts electricity, so parts can be grounded, but its resistivity is far higher than aluminum or copper, so it suits grounded housings, shielding features and fixtures rather than current-carrying parts.

The permeability row is for annealed wrought 316L, which is essentially non-magnetic, a useful property for instrument hardware near sensors.

PropertyValue
Electrical Resistivity (20 °C)Wrought 316L reference (AK Steel)
7.4×10⁻⁷ Ω·m
Electrical Conductivity (20 °C)Calculated from resistivity
1.35 MS/m
Magnetic Permeability (annealed, 200 Oe)Wrought 316L reference (AK Steel)
≤ 1.02 μr

Compatibility data

Chemical properties

EOS publishes no chemical table for printed 316L, so the ratings come from wrought 316L corrosion data for the same alloy. It resists marine atmospheres, chloride waters, phosphoric and acetic acids, caustic cleaning solutions, organic solvents and food and dairy fluids, while hydrochloric acid and boiling strong caustic attack it, and permanent seawater immersion is not recommended.

Chemical ratings are screening guidance; confirm them with application-specific testing before production release.

ChemicalRating
Marine Atmosphere
Excellent
Chloride Waters (up to ~2,000 ppm)
Good
Seawater Immersion
Poor
Phosphoric Acid
Excellent
Acetic Acid
Excellent
Formic Acid
Good
Dilute Sulfuric Acid (<5%, up to 49 °C)
Good
Hydrochloric Acid
Poor
Nitric Acid
Good
Caustic Cleaning Solutions
Good
Sodium Hydroxide 50%, Boiling
Poor
Organic Cleaning Solvents
Excellent
Petroleum Products
Good
Food and Dairy Process Fluids
Good

Compliance

Compliance profile

EOS states that the powder chemistry corresponds to ASTM F138 (UNS S31673), and its safety data sheet confirms the powder contains no REACH Annex XIV substances. EOS's datasheet for the alloy states that as-built tensile properties show the values of ASTM A403, a wrought fittings standard, so solution annealing is not necessary, and EOS lists heat treatment to AMS 2759 as optional.

Each status comes from EOS documents for the powder, so teams can start industrial qualification from supplier data. EOS does not develop or certify the powder as a medical device or for food contact, so the part owner validates those uses.

StandardStatus
ASTM F138 (UNS S31673) chemistryPowder chemistry corresponds to the ASTM F138 surgical-implant bar standard; EOS sells it as StainlessSteel 316L-4441
EOS MDS
REACH Regulation (EC) 1907/2006Powder contains no Annex XIV substances; its nickel content falls under Annex XVII restrictions
EOS SDS
Resources

Datasheets and design resources

Datasheets, design guidance and supplier documentation for Stainless Steel 316L.

Download center

Access the most recent datasheet and supporting documentation maintained by our engineering team.

Stainless Steel 316L datasheet

Design guidelines

Explore printable geometry recommendations, wall thickness tips, and finishing playbooks for DMLS.

View DMLS design guide
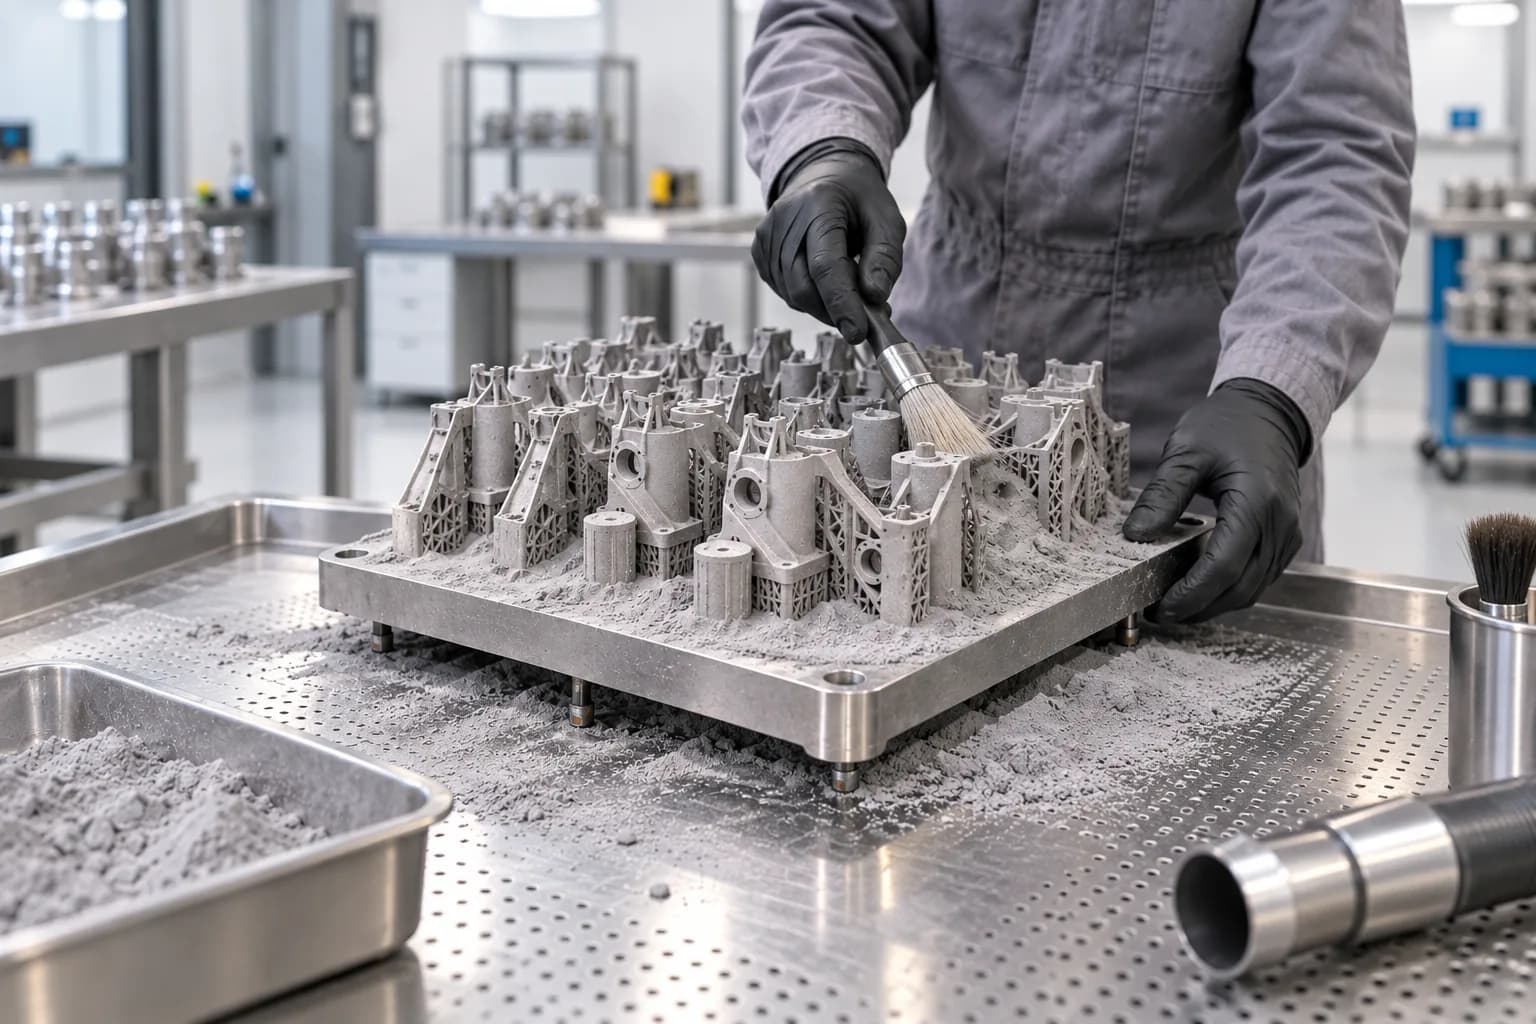
DMLS metal parts on a build plate being cleared of powder
Advanced Manufacturing

Built with Precision DMLS Technology

Stainless Steel 316L is manufactured using Direct Metal Laser Sintering (DMLS) technology, providing high strength and precision for mission-critical applications. Dense tooling and end-use components print from a single prototype to repeat production batches.

Tolerance
±0.3% (min ±0.3 mm)
Production capacity
Multiple parts and assemblies built on each plate
Quality control
In-process monitoring and batch traceability for consistent part quality and material properties
Heat treatment
Stress relief and solution annealing
Colours & finishes
Support removal, shot peening, polishing and machining
Learn more about DMLS technology
Frequently Asked Questions

Frequently asked questions about Stainless Steel 316L

Can't find the answer you're looking for? Reach out to our customer support team.

Stainless Steel 316L is known for its corrosion resistance in marine and chemical environments, its high ductility and toughness, and its dimensional accuracy for complex geometries. As-built DMLS parts reach 630 MPa tensile strength and 41% elongation horizontally in EOS testing, making it suitable for chemical processing, food and beverage equipment and marine hardware.
Start a quote

Ready to Get Started with Stainless Steel 316L?

Upload your design and get an instant quote for Stainless Steel 316L parts.

  • Instant pricing with automated manufacturability analysis
  • Production workflows built for repeatable quality
  • Engineering support from prototype to production
Compare all materials

Create an account to upload CAD

STEP, STL, OBJ, 3MF and IGES supported

Manufacturing technologies
6
Engineering materials
50+
Part quantities
1-500+