
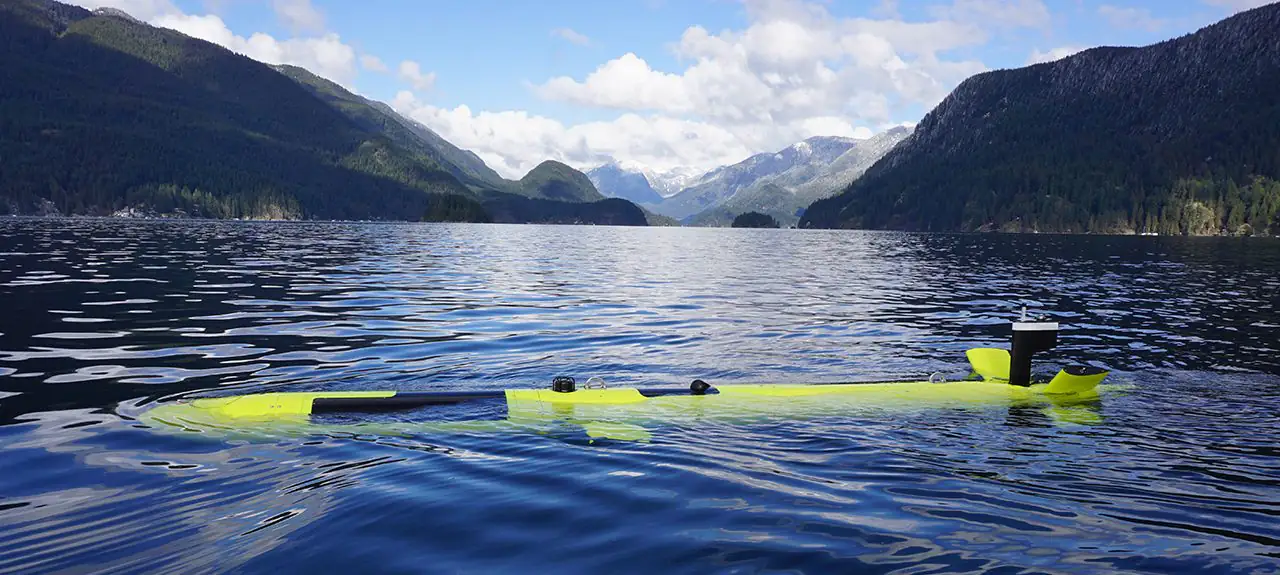
International Submarine Engineering (ISE) has designed and built underwater vehicles since 1974, from autonomous and remotely operated vehicles to robotic manipulators. Parts for its Explorer autonomous underwater vehicle (AUV) are needed as one-offs and short runs, and several of its hull-mounted parts and control-surface pieces had been shaped by hand, built up from moulded fibreglass, or drawn with geometry that would have been expensive to machine. ISE replaced three of them with parts printed by Forge Labs in ASA by Fused Deposition Modelling (FDM).
For this project, Forge's 2017–2018 manufacturing quotes priced an ASA obstacle-avoidance bracket at CAD $395.12 and a forward plane extension at CAD $216.44 per part. The joint case study reported traditional costs of $1,000 for the mount and $1,000–$1,500 for the fibreglass extension. These historical figures show where printing saved work: fitting compound curves, combining moulded pieces and making repeat parts from a file.
The Project at a Glance
- Application: end-use brackets, mounts and plane extensions for ISE's Explorer autonomous underwater vehicle, plus printed templates and jigs for installing them
- Parts: an LED panel bracket with a separate tracing template, an obstacle-avoidance mount with a printed drill jig, and plane extensions
- Process: FDM on Stratasys equipment, mostly at 0.254 mm (0.010 in) layers, with some plane-extension lots at 0.178 mm
- Material and finish: ASA in black or white for the end-use parts; plane extensions printed solid and painted by ISE to match the hull
- Cost comparison: mount quote $395.12 against a reported $1,000 traditional cost (60.5% lower); plane extension quote $216.44 against $1,000–$1,500 in fibreglass
- Reorders: plane extensions printed from stored files for spares and new vehicles
- Quoted lead times: 1–2 days for the mount and 2–3 days for the plane extension
Parts That Have to Follow a Curved Hull
An AUV hull is a smooth shell with compound curves. Anything mounted to it, whether a light, a sensor or a control surface, needs a mating face that follows the curve and a bolt pattern that lines up with holes through the shell. Each traditional route had its own cost:
- Hand fabrication. Hand-made obstacle-avoidance mounts were reported to be expensive and difficult to produce, and each was unique, which made them difficult to replace in the field.
- Machining. The LED panel had to sit at an irregular angle inside its bracket, geometry that would have been very expensive to machine.
- Moulded fibreglass. Each plane extension was several moulded pieces glued together and then machined.
"Making short run production parts can be very expensive when using complex CNC machining and fabrication - 3D printing has allowed us to produce complex parts and one-offs much more cheaply than traditional methods."
Printing changes the economics because one file defines the part. Cost follows material and machine time rather than setups, so a curved mating face or an angled seat costs about the same as a flat one, and the second copy matches the first.
The PartsThree Parts, Three Routes Replaced
| Part | Previous route | Printed route | What changed |
|---|---|---|---|
| LED panel bracket | Angled geometry, expensive to machine | ASA bracket modelled to the inside of the hull, plus a printed tracing template | Angled seat at little or no extra cost; the bracket was reported to be its own drilling template |
| Obstacle-avoidance mount | Hand-fabricated to the hull, each one unique | ASA mount from one file, with a printed drill jig | Identical copies, shaped for flow |
| Plane extension | Moulded fibreglass pieces, glued and machined | One solid ASA piece, painted by ISE | One part instead of an assembly |
Why FDM in ASA
FDM builds a part by extruding thermoplastic filament layer by layer, with a separate soluble support material under overhangs. FDM was chosen for many of ISE's end-use components. It prints engineering thermoplastics straight from CAD, at sizes that suit vehicle brackets and fairings.
UV stability for parts that ride at the surface
An AUV spends time on deck and rides awash at the surface, so exterior parts see sun. Stratasys describes ASA as similar to ABS with better UV resistance and measured almost no loss of strength after 1,000 hours of accelerated UV weathering. UV resistance is why ASA became ISE's default for exposed parts. By contrast, HP's weathering tests show bare PA12 turning brittle under prolonged UV, so PA12 goes outside only painted or coated.
| Stratasys ASA data | Value | What it means here |
|---|---|---|
| 1,000 h QUV weathering (ASTM G154) | Stress at break 30.5 to 29.5 MPa | Little strength loss after accelerated UV ageing |
| Elongation at break | 5.9% (XZ), 1.8% (ZX) | Layer bonds are the weak direction |
| Flexural strength | 61.5 MPa at 5% strain, no break (XZ); 51.0 MPa at break (ZX) | Orient bending loads along the layers |
| Specific gravity | 1.08 | Slightly denser than water: count printed parts in the weight and trim budget |
FDM is directional
In Stratasys's XZ tests the load runs along the extruded roads; in ZX the bar is built upright and the load pulls the layers apart. For a bracket in compression against a hull this hardly matters. For a cantilever or a bolted flange ear it decides the orientation: a lug printed in the build plane carries load along the roads, while the same lug standing up in Z can split along a layer. Holes differ too: one whose axis runs up the build prints round, one lying on its side comes out slightly oval, so drill or ream any hole that must be precise.
Fill is a specification
Sparse fill replaces a part's interior with a honeycomb structure that can save material and machine time. When ISE asked for a drill jig at around 50% sparse fill, we explained that Stratasys sparse fill is not an exact percentage: it comes in lower- and higher-density styles, and the resulting density depends on the geometry. For the thin parts in that request, solid and sparse-fill prices were almost the same: there was too little interior volume to remove for a meaningful saving. Specify the loads and how a part will be used before choosing fill; a lower setting alone does not guarantee a cheaper part.
Hollow designs need one more check: a closed cavity fills with soluble support during the build, so give it drain holes (our FDM design guide sets a 4 mm minimum) or print it solid.
Tolerance and installation
Our published FDM tolerance is ±0.25 mm or ±0.3%, whichever is greater: ±0.3 mm on a 100 mm feature, ±0.9 mm on a 300 mm part. On a short bracket that variation fits within a normal clearance hole; across a 300 mm part it can use up the clearance, so on long bolt patterns open or slot the holes in CAD, or drill the shell through the printed part or a printed jig. Drilling through the part is the method reported for the LED bracket below: the holes in part and hull then match whatever small variation either has.
LED Panel BracketTemplate First, Then the Bracket
An LED panel had to be set into the vehicle's curved body. That meant cutting a large, complex opening through a finished, painted hull, and holding the panel at an angle behind it.
Mark the opening before cutting
ISE ordered a printed template for the opening alongside the brackets, and we offered to have it ready a business day ahead of them. The template is an open frame: an outline with diagonal braces, light and stiff, using little material, with the hull visible through it while it is positioned. Taped in place, it lets the fitter trace the opening before any cut is made. ISE left the template's colour and fill to us, which is typical for parts like this.
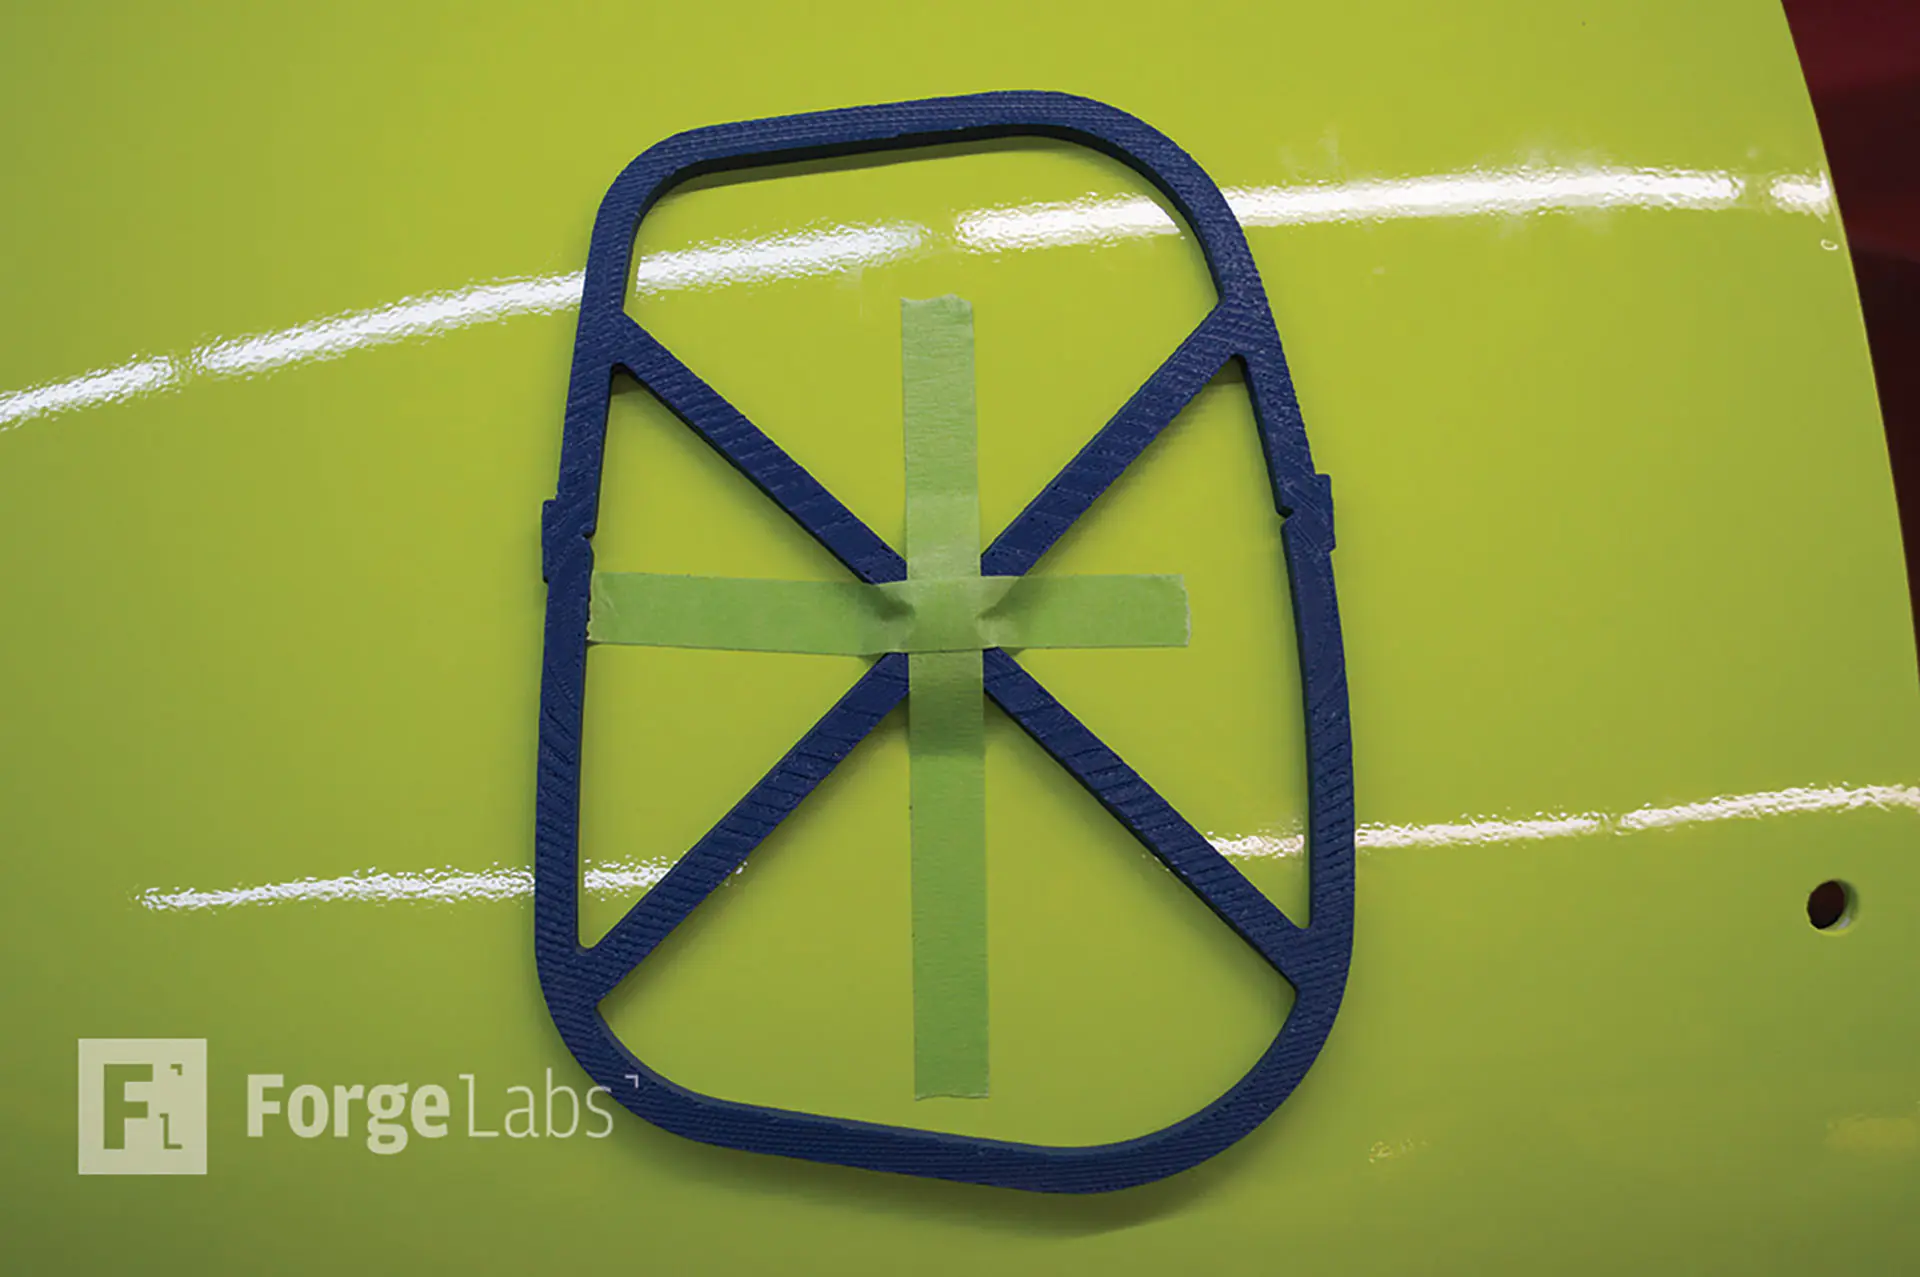
A printed tracing template, taped to the hull, used to mark the outline of the LED-panel opening before it was cut.
A bracket modelled to the inside of the hull
The bracket was printed in white ASA, with its upper edge modelled to follow the inside of the shell. It was reported to serve as its own drilling template, which transfers the bolt pattern straight from part to hull with no separate jig to keep in step with the design. The panel sits at an angle within the bracket, and that angled seat was about as cheap to print as a flat one. ISE's raised lettering prints in at no extra cost; our FDM design guide asks for raised detail at least 1 mm wide and 0.5 mm high.
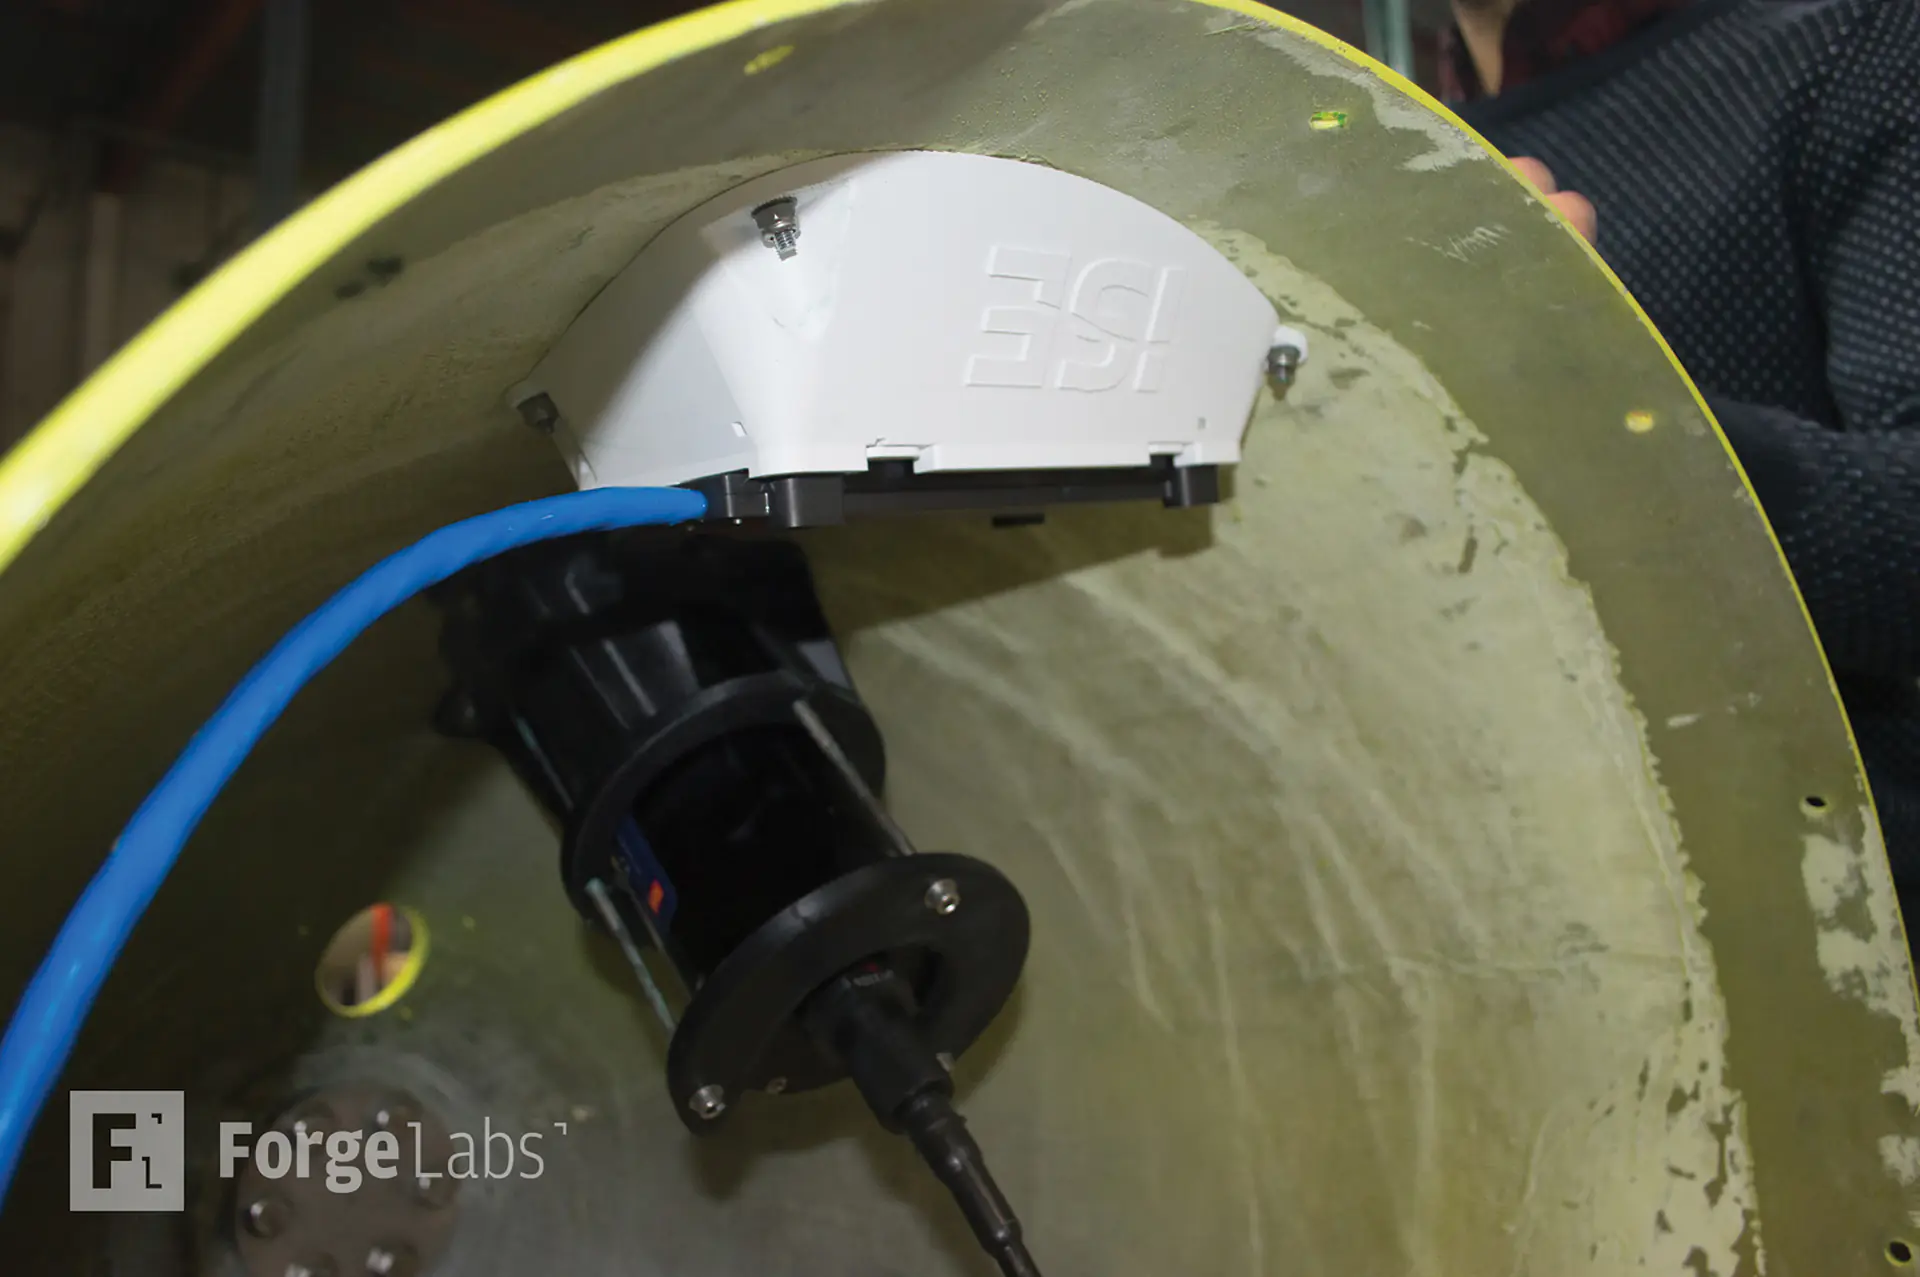
The white ASA LED panel bracket fitted inside the hull, its upper edge following the curve of the shell.
When the bracket design changed, the new files went straight into a new order, with no tooling to change.
Obstacle-Avoidance MountOne File Instead of Hand Fitting
The obstacle-avoidance mount holds part of the vehicle's obstacle-avoidance system against the compound curve of the hull. Printed from one file, every copy carries the same mating curve and hole pattern, so a spare is a reorder rather than another round of hand fitting.
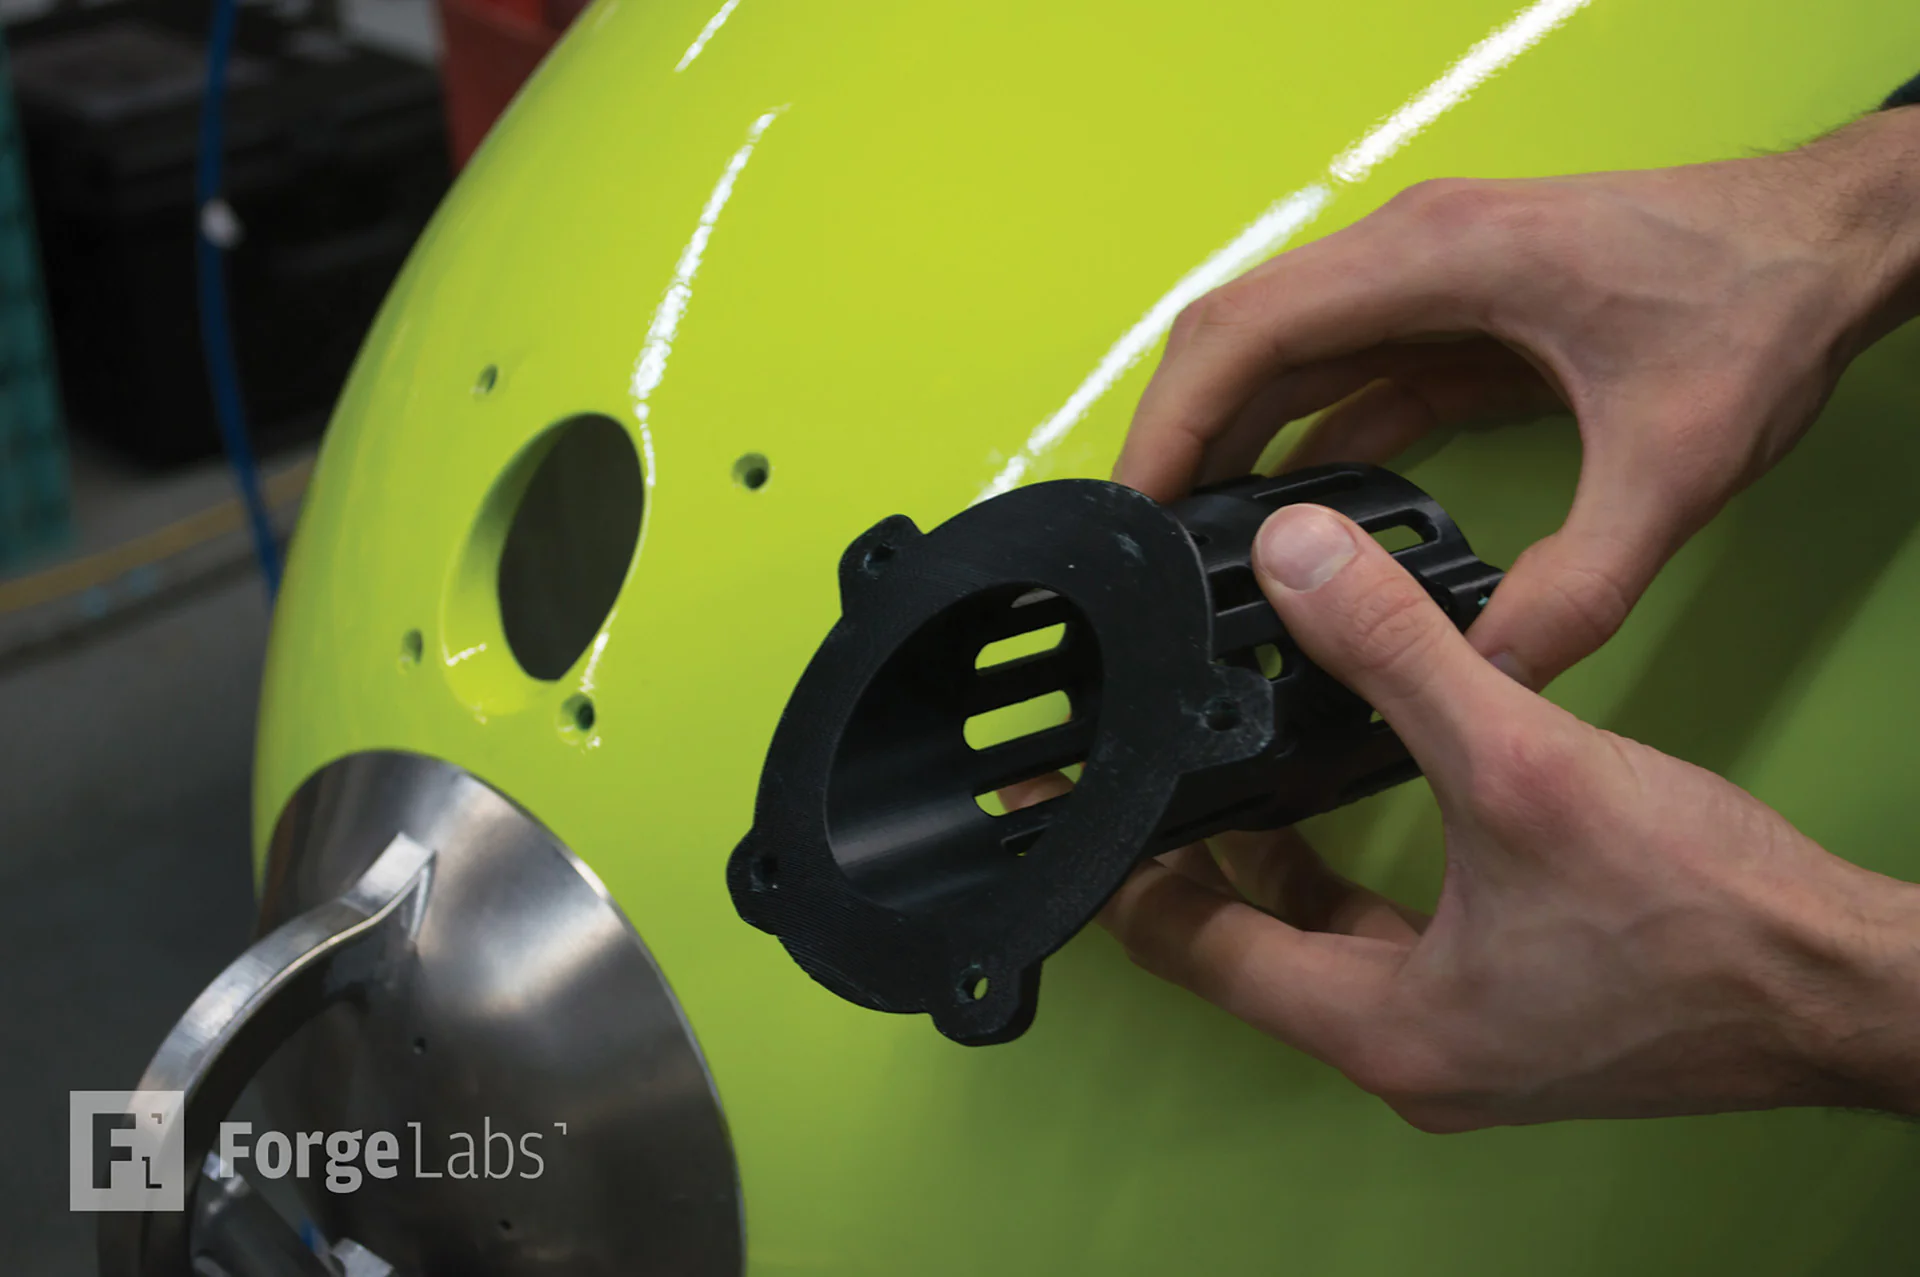
A printed ASA obstacle-avoidance mount test-fitted to the curved hull; its holes match the bolt pattern drilled through the shell.
Fill by function: solid mount, sparse jig
ISE ordered its first obstacle-avoidance mount parts in solid black ASA, with a printed drill jig in sparse-fill white ASA. A mount that carries load is normally printed solid; a jig that only locates a drill does not need to be. A separate jig keeps the drill out of the finished mount's own holes and can be reused on the next vehicle; if it will drill many hulls, press in metal drill bushings, because plain guide holes in a plastic jig wear.
On a bulky mount, there is more interior volume to change. Discuss the required stiffness and loaded regions before reducing fill, and compare the quoted saving with the demands on the part.
Shaped for flow
Printing also let ISE make the mount's outside much more hydrodynamic at very low cost. A faired surface costs about the same to print as a blocky one; on a hand-made part, every curve is extra work.
Forge quoted the mount at $395.12, with a 1–2 day lead time. Compared with the original case study's reported $1,000 traditional cost, the quoted manufacturing price was 60.5% lower.
Plane ExtensionsOne Printed Piece Instead of a Fibreglass Assembly
The plane extensions attach to the vehicle's planes. In fibreglass, each was several moulded pieces glued together and then machined. Printed, each is a single ASA part: no moulds, layup, cure or bonding. Forge quoted the forward extension at $216.44 per part with a 2–3 day lead time; the original case study reported $1,000–$1,500 for the fibreglass version. ISE's painting was separate from the printed-part quote.
Orientation and fill for a cantilevered part
A plane extension is a cantilever, with bending loads peaking at the root where it attaches. If the span runs up the build, root bending pulls the layers apart, the 1.8% ZX direction in the ASA data. Laying the span in the build plane keeps bending stress along the roads; the trade is stair-stepped layers across the airfoil's gently curved faces. ISE's purchase orders specified the material, solid fill and the layer height, and some lots used finer 0.178 mm layers, which reduce stair-stepping at the cost of a longer print.
Painted to match
ISE painted the extensions itself to match the hull. Over a filler primer, paint hides FDM layer lines and lets a printed part and a fibreglass shell read as one surface. Because the parts would be painted, the base colour did not matter, and lots were printed in black or white. If your parts will be painted, say so on the order and leave the colour open.
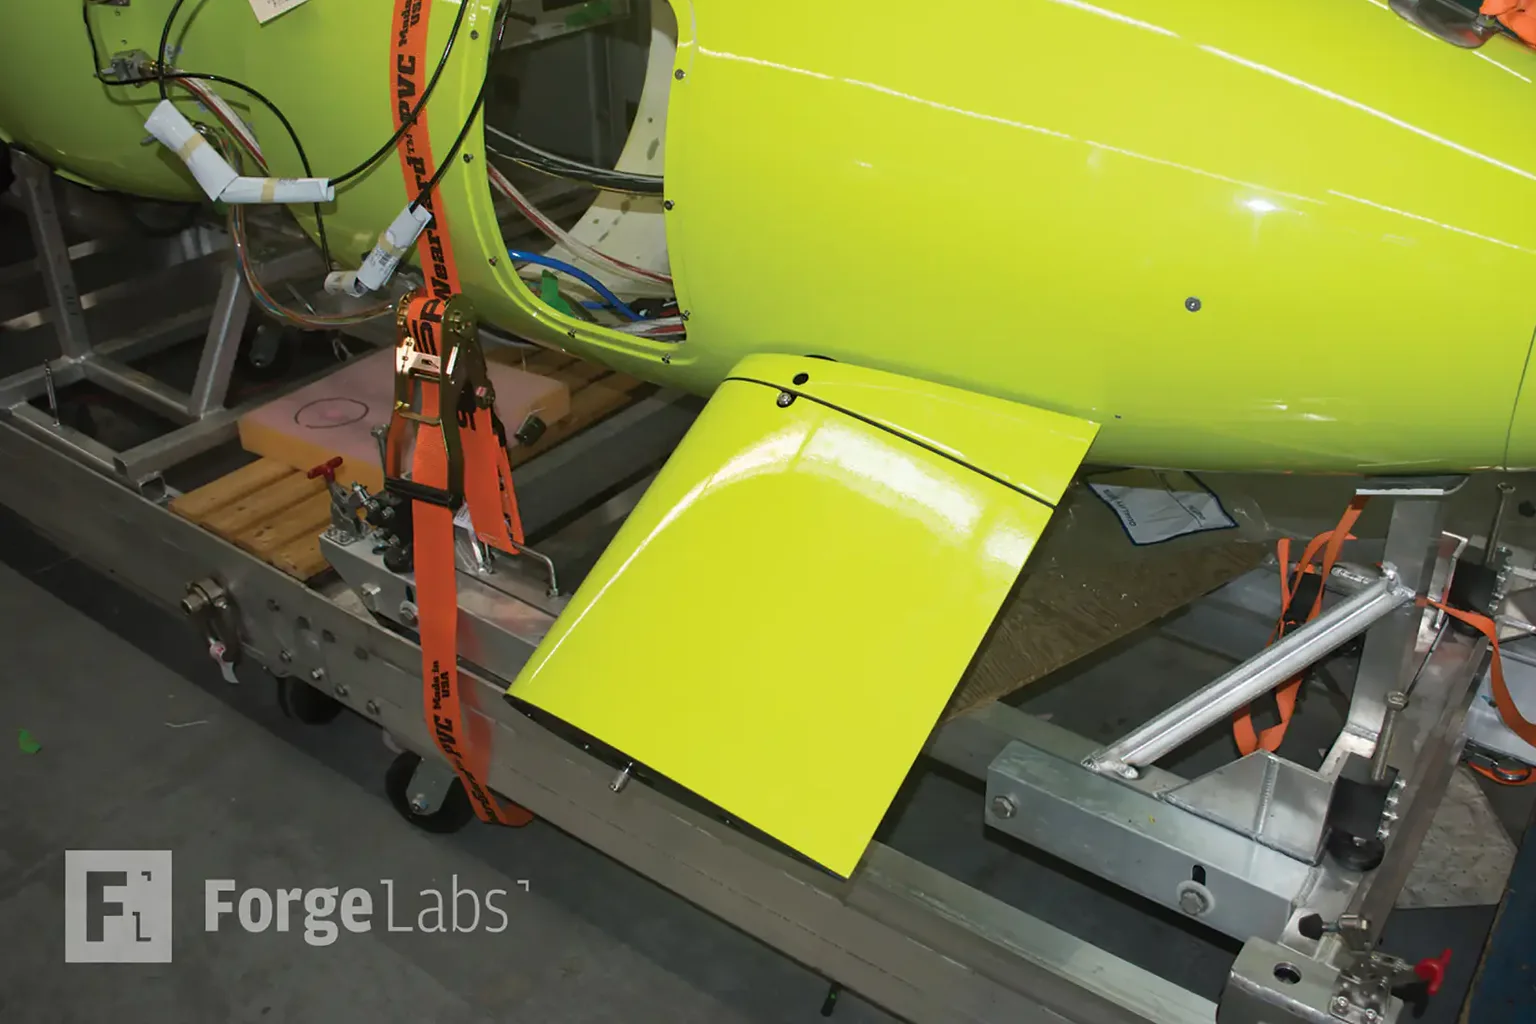
A plane extension, printed in ASA and painted by ISE to match the hull, on the vehicle in its cradle.
Reordered from the file
Plane extensions were reordered for spares and new vehicles. Each reorder started from stored files, without a mould to maintain. Keep the approved revision and manufacturing specification together so a replacement uses the intended geometry, material and fill.
TurnaroundShort Lead Times Without Tooling
The mount's 1–2 days and the extension's 2–3 days were quoted lead times. Separate urgent extension orders were completed the same day or within two days. Stored files and a familiar material let Forge move straight into printing, without making moulds or waiting for a fibreglass layup to cure. For a vehicle waiting on a replacement, that removed work from the manufacturing schedule as well as cost from the part.
The Longer RelationshipFrom Three Parts to Dozens of Orders
ISE began ordering from Forge Labs in 2017. The work included end-use brackets and mounts, plane extensions, drilling templates and jigs, connector panels and cable trays, tooling for fibreglass layup and moulds, and short production runs. Processes included FDM (ASA, ABS, Nylon 12, ULTEM 9085, and PLA for layup tools), SLA, PolyJet and SLS. Our separate case study on ISE's PolyJet antenna moulds covers one of the tooling jobs.
Materials were chosen by environment: ASA where a part would see sun, ULTEM 9085 where flame retardance was needed, and nylon where UV and water were not an issue. The practical lesson is to choose a material for each component's exposure and duty, then preserve that specification for repeat orders.
What this says about printed parts on underwater vehicles
- Templates and jigs are the quiet workhorse. ISE bought printed drilling templates, drill jigs, hatch templates and cut-out templates alongside its end-use parts. They are cheap, and they lower the risk of a mis-cut or mis-drilled hole in a finished hull.
- Exterior end-use parts belong in UV-stable material. ASA for anything in the sun, with PA12 kept inside or painted.
- Repeatability comes from the file. A stored file replaces the fitter's skill and the mould on the shelf, so a later spare is made from the same definition as the original.
What the Printed Parts Delivered
| Part | Reported traditional cost (CAD) | Printed quote per part (CAD) | Price reduction | Quoted lead time |
|---|---|---|---|---|
| Obstacle-avoidance mount | $1,000 | $395.12 | 60.5% | 1–2 days |
| Forward plane extension | $1,000–$1,500 (fibreglass) | $216.44 | About 78–86% | 2–3 days |
Beyond cost, the mounts became identical copies instead of hand-fitted one-offs, each plane extension became one part instead of a bonded assembly, and printed templates and jigs lowered the risk of installing parts on a finished hull.
LessonsWhat to Apply to Your Own Vehicle Parts
- Model the mating face from the hull, not the fitter's hands. The hand-made mounts were each unique; the printed ones share one curve and hole pattern.
- Print a template before you cut a finished hull. A light open-frame template marked the LED opening before the painted shell was cut.
- Let the part drill its own holes, or print a jig. Drilling through the bracket, as reported for the LED panel, transfers its pattern directly. Where the finished part's holes must not be drilled through, or the pattern repeats across vehicles, use a printed jig, as ISE did for the mount, with metal bushings if it will drill many holes.
- Use angles and curves freely. The angled LED seat cost about the same as a flat one.
- Replace multi-piece layups with one printed piece, then paint, leaving the base colour open. Each plane extension became one ASA part, printed in black or white because it would be painted.
- Orient cantilevers and lugs so loads run along the layers. ASA elongation at break is 5.9% along the roads and 1.8% across them.
- Specify fill by function and check the saving. A mount and a locating jig have different duties; on a thin part, sparse fill may barely change the price.
- Choose material by environment. ASA for sun, ULTEM 9085 for flame retardance, PA12 where UV and water are not a factor.
- Keep the file as the spare. Store the approved revision with its material, fill and finishing requirements.
Could Your Vehicle Part Be Made This Way?
Good candidates are brackets, mounts, fairings and housings that must follow a curved hull or shell; control-surface pieces now laid up in fibreglass; templates and jigs for cutting or drilling a finished hull; and parts needed in ones and twos per vehicle, then again as spares. Exterior parts in sun suit ASA; interior parts can also use PA12 or ULTEM 9085.
Send a STEP file with the drawing, the quantity per vehicle, which surfaces will be painted, which holes must hold position and which loads the part carries. For parts that stay immersed or carry pressure, test printed samples in your own conditions before release; Stratasys's ASA data covers strength and UV weathering, not long-term immersion.
For design rules, see our FDM design guide, our guides to part orientation and 3D printed jigs and fixtures, and 3D printing for robotics. Related case studies cover FDM ASA and carbon-fibre nylon parts for welding robots and repeat SLS PA12 exoskeleton actuator parts.
Need Parts That Fit a Curved Hull?
Send us the STEP file, drawing and quantity per vehicle. We will recommend a material, fill and orientation for each part, and quote any templates or jigs you need to install it. We offer lead times from 2 business days, 24-hour turnaround on request, and next day shipping anywhere in the US and Canada.
Discuss Your Parts With Us